Carton Flow Racking Systems: How Gravity-Fed Dynamic Storage Cuts Picking Travel Time by Up to 75%
Global procurement directors, supply chain engineers, and distribution managers are turning to engineered Carton Flow Racking to conquer the complexities of rapid order fulfillment, split-case picking, and strict FIFO inventory rotation. Discover structural specifications, design calculations, market dynamics, and factory-direct custom fabrication from Guangzhou Heda Shelves Co., Ltd.
- 25+ Years ExperienceSpecialized rack engineering since 2001
- 30,000 t / MonthIn-house manufacturing scale
- CE & ISO 9001:2015Strict international quality compliance
- 10,000+ InstallationsExported across 120+ countries
The Mechanics of High-Performance Carton Flow Racking Systems
Carton Flow Racking (frequently termed carton live storage or gravity flow shelving) is an advanced material handling structure designed for high-throughput fulfillment environments where individual cartons, plastic bins, or totes must be processed with extreme speed and zero picker interference.
Unlike static shelving where pickers must traverse long aisles and reach deep into cluttered shelves, carton flow systems transform the storage volume into a dynamic mechanical conveyor. The core operational principle relies on inclined wheel tracks or full-width roller tracks mounted between horizontal load beams. Goods are loaded from the rear replenish aisle and glide smoothly under gravitational force to the front pick face.
This physical separation of loading and retrieval aisles eliminates bottlenecks. Replenishment staff restock cases without obstructing active pickers on the forward side. As front boxes are removed for individual item consolidation, subsequent totes advance autonomously. The structural outcome is an immediate 40% to 75% reduction in overall picker walking distance, condensed storage footprint, and seamless enforcement of First-In, First-Out (FIFO) product movement—indispensable for perishable foods, pharmaceuticals, cosmetics, and fast-moving retail consumer items.
- Automatic gravity replenishment with zero power consumption
- Dedicated ergonomic pick trays (knuckle trays) to reduce wrist strain
- Modular lane guides adaptable to variable package dimensions
- 100% full-depth accessibility with high SKU density
Engineering Parameters: Wheel Track Beds vs. Full-Width Steel Roller Tracks
Selecting the exact roller configuration is essential for maximizing carton flow velocity and avoiding carton hang-ups or structural deflection. Guangzhou Heda Shelves Co., Ltd. manufactures both skate-wheel tracks and heavy roller beds custom-sized to carton packaging dynamics:
| System Property | Skate-Wheel Track Beds (Plastic / Nylon) | Full-Width Roller Beds (Steel / Galvanized) | Full-Bed High-Density Polypropylene Wheels |
|---|---|---|---|
| Best Suited Packaging | Rigid plastic totes, flat uniform corrugated cartons | Soft bottom boxes, wire baskets, heavy wooden crates | Mixed carton shapes, irregular dimensions, shifting SKUs |
| Standard Capacity | 15 – 35 kg per linear lane meter | 50 – 120 kg per linear lane meter | 25 – 60 kg per linear lane meter |
| Recommended Incline Pitch | 3.0% – 4.5% (1.7° to 2.6° slope) | 2.0% – 3.5% (1.1° to 2.0° slope) | 3.0% – 4.0% (1.7° to 2.3° slope) |
| Lane Adjustability | Fixed or clip-in guide separators | Individual roller axle brackets | Infinite multi-lane flexibility, drop-in dividers |
| Surface Finish | Galvanized frame with virgin PE / POM wheels | Zinc-plated / powder-coated heavy steel tubes | Extruded high-tensile aluminum alloy rails |
Engineered Carton Flow Racking Systems Built for Scale
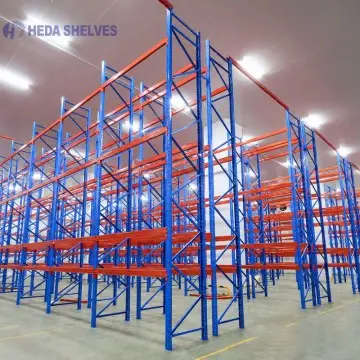
Whether deploying stand-alone picking stations, integrating dynamic carton beds into selective pallet racking, or incorporating flow levels within multi-tier mezzanine picking towers, explore our primary configurations.
Integrated Pallet & Carton Flow
Drop-in gravity track beds fitted beneath upper reserve pallet storage bays for maximum vertical cube utilization.
Inquire Now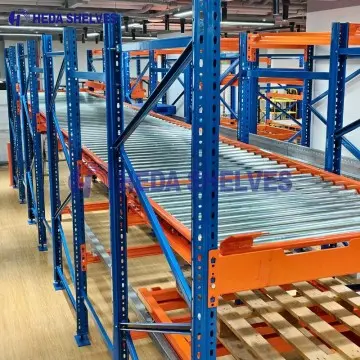
Standalone Picking Towers
Multi-tier dedicated carton live storage equipped with ergonomic knuckle trays and take-away roller conveyor lanes.
Inquire Now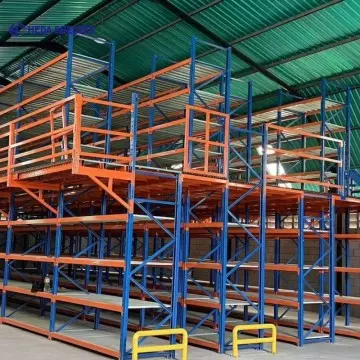
Mezzanine Carton Flow Modules
Engineered multi-level picking modules multiplying warehouse floor space by 200% with integrated vertical chutes.
Inquire Now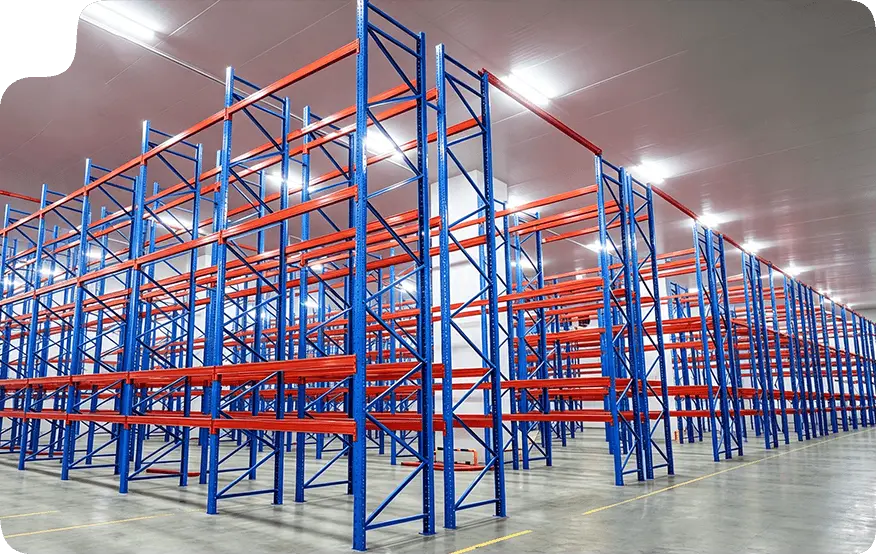
Refrigerated Carton Flow Racks
Low-temperature grease bearings and galvanized corrosion-resistant tracks engineered for food, vaccine, and cold room logistics.
Inquire NowFuture Procurement Trends & Development in Carton Flow Systems
As supply chains pivot from bulk pallet shipments to high-frequency, each-picking ecommerce fulfillment, global warehouse planners are rethinking dynamic flow architecture. Here is where the sector is advancing over the coming decade.
1 Pick-to-Light & Sensor IoT
Modern distribution facilities require zero-error picking. Modern carton flow tracks are pre-machined with snap-in conduits to support Pick-to-Light (PTL), Put-to-Light, and optical inventory level sensors. Real-time consumption telemetry alerts restocking crews the instant a lane drops below critical thresholds, eradicating stock-outs during peak seasons.
Smart Logistics Integration2 AMR & Robotic Pick Cells
Rather than humans walking aisles, future warehouse blueprints integrate carton flow beds as dynamic buffer racks feeding Autonomous Mobile Robots (AMRs) and articulated robotic picking arms. By maintaining predictable presentation angles and self-indexing carton positions, carton flow offers the consistent spatial geometry required by machine vision systems.
Automation-Ready Design3 Universal Drop-In Modularity
Procurement teams are moving away from proprietary, welded rack assemblies that bind them to a single supplier. The prevailing procurement demand focuses on universal bracket drop-in beds that easily adjust on 50mm, 75mm, or 76.2mm pitch beams. This allows facility operators to repurpose existing racking inventory without costly capital reconstruction.
Flexible Asset LifecycleKey Drivers Shaping Next-Gen Carton Flow Adoption
- Surging SKU Counts: Micro-fulfillment and retail customization require dense, front-facing SKU presentation without expanding building footprint.
- Labor Shortages & Ergonomics: Tilted front knuckle trays present carton contents at ideal ergonomic sightlines, slashing repetitive bending and operator fatigue.
- Strict Expiration Tracking: Strict First-In First-Out gravity movement ensures dated pharmaceutical and perishable food inventories rotate reliably.
Procurement Evaluation Criteria for Strategic Buyers
- Wheel Axle Longevity: Look for cold-drawn steel axles and impact-modified virgin polypropylene or acetal rollers to prevent flat-spotting.
- Galvanized vs. Painted Track Beds: High-cycle abrasion quickly peels paint; continuous hot-dip galvanized or extruded anodized aluminum tracks ensure multi-year corrosion resistance.
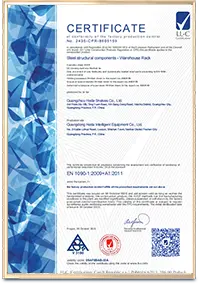
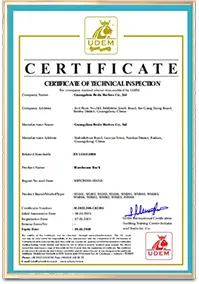
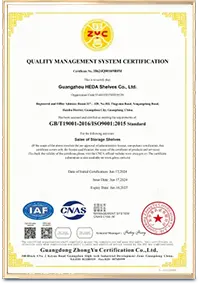
- Factory Capacity & Quality Control: Verify verified testing certificates (CE, ISO 9001) and in-house cold roll-forming capabilities for consistent beam tolerances.
Why Leading Global Brands Partner with Guangzhou Heda Shelves Co., Ltd.
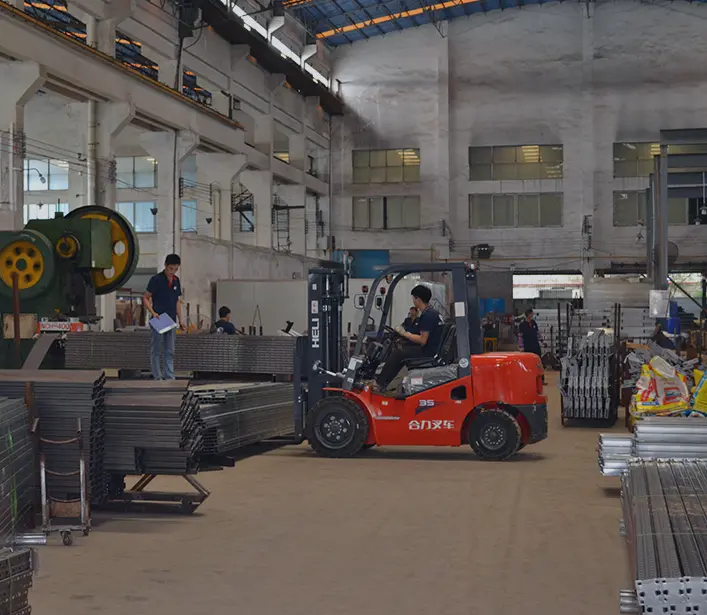
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international leader in the engineering, fabrication, and export of high-density warehouse storage systems. Operating from our modernized 30,000 square meter production facility with over 300 experienced technical experts and structural engineers, we deliver comprehensive warehouse solutions that maximize vertical storage density and operational velocity.
Our carton flow racking and industrial shelving systems are built to withstand intensive industrial operations. Every column, beam, track, and bracket is manufactured from premium high-grade certified steel, undergoing automated CNC cold bending, multi-station column punching, acid pickling, phosphating, and electrostatic powder coating. With an expansive monthly production capacity reaching 30,000 tons, we support enterprise distributors, logistics integrators, and commercial facilities worldwide with swift lead times and strict structural consistency.
Free 3D & CAD Layouts
Submit your building floor plan and carton parameters. Our engineering team delivers full CAD schematics and 3D visual models within 24 hours.
CE & ISO 9001 Certified
Rigorous factory quality verification (CE No. 2435-CPR-8605159) ensuring structural compliance and safety across every batch.
Custom OEM / ODM Support
Tailored track widths, roller materials, beam spans, and load profiles engineered to your specific carton dimensions and conveyor heights.
Ocean Packaging & Fast Lead
Protective export bundle wrapping and optimized container stuffing that prevents transit scuffing while minimizing international freight costs.
10 Rigorous Production Stages Behind Every System
Every carton flow bed, upright frame, and connector beam is produced within Guangzhou Heda Shelves Co., Ltd.'s modern workshops under continuous quality monitoring.
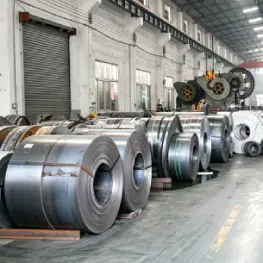 01
Raw Steel Quality Test
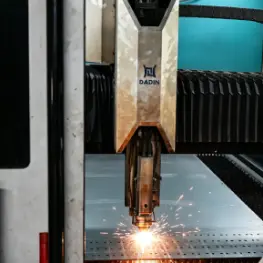 02
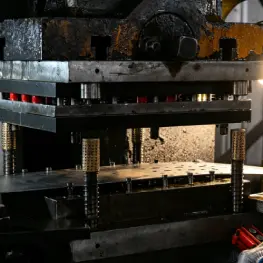
Precision CNC Cutting
 03
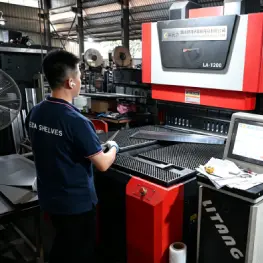
Automated Punching
 04
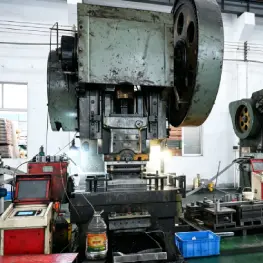
Cold Roll Forming
 05
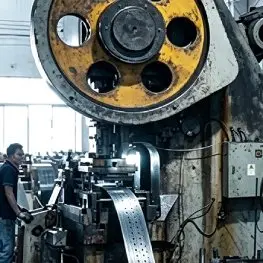
Track Profile Bending
 06
Automated Polishing
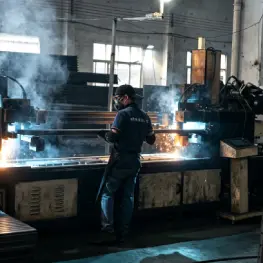 07
Robotic Structural Welding
 08
Pickling & Phosphating
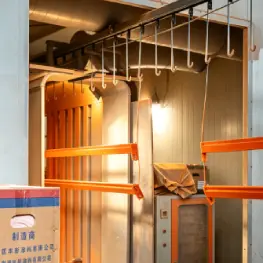 09
Electrostatic Coating
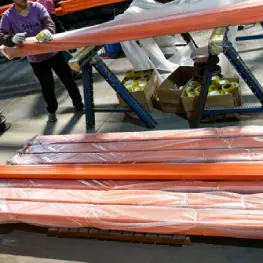 10
Final QC & Export Stacking
Audited Quality Systems for Global Tenders
Procuring warehouse racking internationally demands verified certification to appease municipal building inspectors, insurance auditors, and corporate safety standards. Guangzhou Heda Shelves Co., Ltd. adheres to stringent manufacturing protocols with verifiable test records.
- CE Certified: Structural Standard Certificate No. 2435-CPR-8605159
- ISO 9001:2015: Quality Management System Certification No. 18624Q00169R0M
- Environmental Compliance: RoHS compliant, heavy metal-free powder finishes


Questions Global Procurement Directors Ask Most About Carton Flow Racking
Gain definitive technical clarity on pitch angle calculations, carton deflection, retrofitting existing uprights, and international shipping logistics.
Get CatalogWhat is Carton Flow Racking and how does it optimize split-case picking operations?
How do you calculate the correct incline slope angle for various cartons and totes?
Can carton flow beds be retrofitted into our existing pallet racks?
What is the weight carrying capacity per running lane and per bed level?
How does Guangzhou Heda Shelves protect racking components against corrosion and impact?
What parameters are needed to request a free 3D design and quotation?
"A properly calculated carton flow system is not simply steel and wheels; it is an ergonomic, high-speed engine that drives warehouse productivity. Every millimeter of pitch and roller spacing is calculated to ensure seamless, jam-free operation."
Senior Logistics Engineer, Guangzhou Heda Shelves Co., Ltd.Transform Your Order Picking Efficiency Today
Partner directly with the manufacturer. Request our comprehensive industrial catalog, complete technical specifications, or a tailored 3D CAD warehouse layout proposal from Guangzhou Heda Shelves Co., Ltd.
- Free 3D Layout & CAD Design
- Sample Testing for Custom Cartons
- Factory Direct Competitive Pricing
- Worldwide Door-to-Port Delivery