- 25+ Years ExperienceEstablished in 2001 with 300+ staff
- 30,000 t / Month30,000 m² factory capacity
- CE & ISO CertifiedCE 2435-CPR-8605159 & ISO 9001
- 10,000+ ProjectsShipped globally across 120+ countries
What Is a Gravity Flow Pallet Rack and How Does It Drive High-Throughput Warehouses?
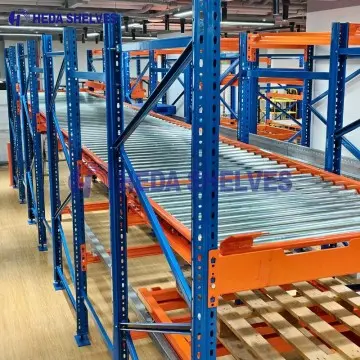
A gravity flow pallet rack—frequently termed dynamic live storage, pallet flow racking, or roller-bed racking—is an ultra-high-density storage system operating strictly on gravity. Driven entirely by mechanical inclination and natural gravitational descent, pallet flow provides unmatched stock rotation without external electrical draw.
By engineering dedicated loading faces on the charging end and separated unloading faces on the discharge end, gravity flow pallet racks completely segregate forklift loading traffic from high-velocity picking activity. As incoming unit loads are deposited into deep rolling lanes (spanning from 2 pallets deep to expansive 25-pallet-deep channels), the 2.5% to 4.0% incline allows the unit to coast gently forward at controlled speeds.
When the front pallet is unloaded by a reach truck or counterbalance forklift, the trailing inventory automatically indexes forward to fill the vacant front position. This continuous automatic replenishment eliminates internal warehouse staging bottlenecks, reduces vehicle travel distances by up to 50%, and unlocks true First-In, First-Out (FIFO) stock rotation indispensable for perishable food, cold storage, beverage bottling, pharmaceutical supply chains, and batch-controlled manufacturing.
- True mechanical First-In, First-Out (FIFO) rotation
- Decoupled aisles eliminate forklift cross-traffic collision risks
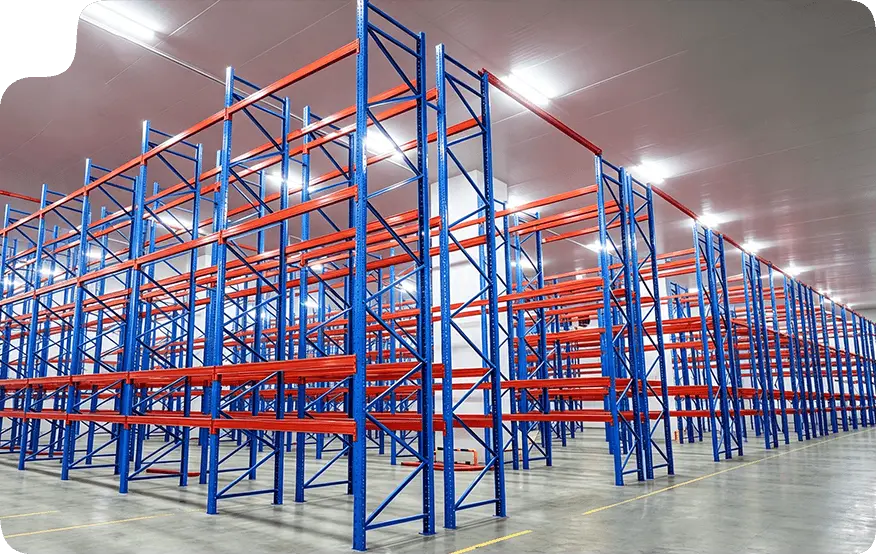
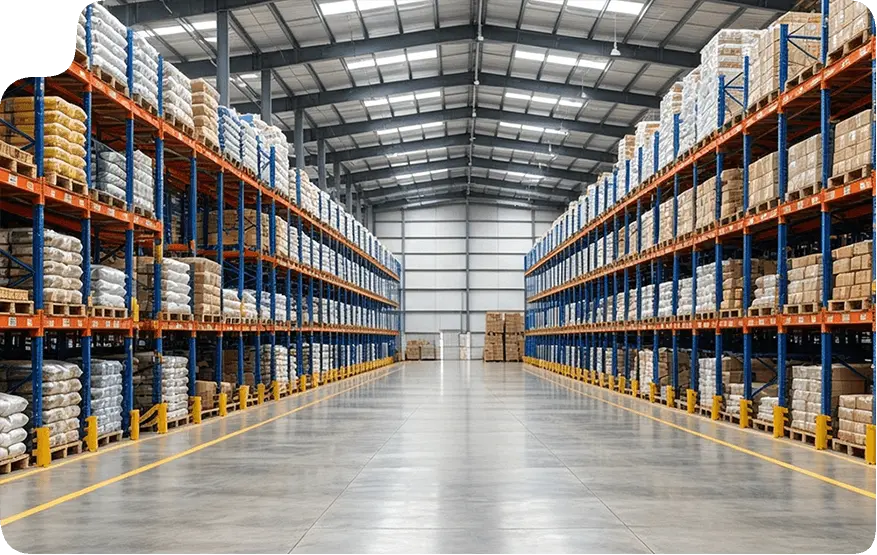
- Up to 70% floor surface utilization compared to selective racks
- Zero electrical power requirements during regular dynamic cycles
Engineered Gravity Flow Configurations Tailored to SKU Profiles
No two dynamic warehouse applications are identical. Guangzhou Heda Shelves Co., Ltd. configures track width, roller geometry, slope gradient, and braking mechanisms based on specific unit load dynamics, pallet construction, and throughput velocities.

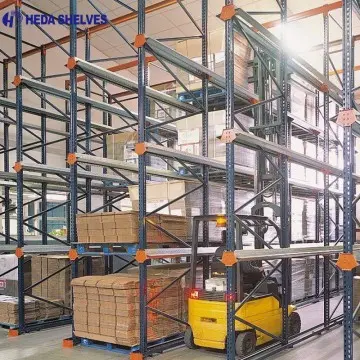
Full-Width Steel Roller Tracks
Designed for multi-spec wooden pallets, GMA, and Euro pallets where bottom skids vary in width or board placement. Heavy-wall zinc-plated steel tubes guarantee continuous structural contact, eliminating pallet hang-ups caused by broken bottom deck boards or fastener snags.

Dual & Triple Track Split Rollers
Optimized for standardized pallet fleets, high-density plastic runners, and slave board systems. Utilizing high-capacity precision bearings spaced specifically along the bottom runners minimizes deadweight, conserves raw material costs, and reduces friction across medium-duty loads up to 1,200 kg.

Cold Chain & Freezer Grade Systems
Engineered for walk-in blast freezers and cold storage down to -30°C. Upgraded with low-temperature synthetic ester lubricating greases, stainless steel internal ball assemblies, and hot-dip galvanized or epoxy zinc-rich finishes to resist condensation frost and thermal contraction fatigue.
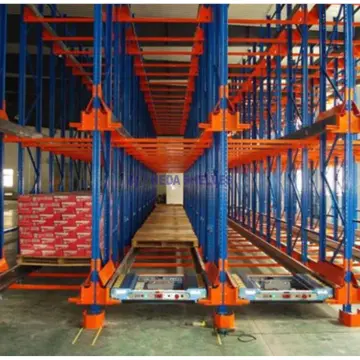

Deep-Lane Flow with Safety Separators
For high-throughput shipping consolidation and lanes running 10 to 25 pallets deep. Integrates heavy-duty pneumatic or mechanical pallet separators that isolate the front discharge pallet from the cumulative rear line pressure, allowing forklift operators to extract loads with zero friction drag.
Future Procurement Trends: How Modern Supply Chains Are Sourcing Dynamic Flow Racks
The global logistics environment is witnessing sharp structural shifts driven by warehouse footprint costs, cold storage demand surges, and higher order velocities. Global buyers are transitioning from basic static storage toward intelligent, energy-efficient dynamic flow racks.
1. Decoupling Operating Energy from High Density (Zero-Power Automation)
With escalating industrial electricity costs and strict corporate carbon reduction targets, logistics operators are re-evaluating power-hungry automated storage systems. While automated shuttle systems and mini-load ASRS have their place, their continuous electrical consumption, complex sensor suites, and scheduled software upkeep add recurring operating costs.
Procurement teams increasingly choose gravity flow pallet racks as a robust alternative or hybrid counterpart. Gravity racking delivers the storage density of deep automated lanes with zero operational power draw, utilizing passive gravitational potential energy to sequence pallets seamlessly across multi-shift facilities.
2. Seismic Resiliency and International Code Harmonization
Global logistics hubs—especially in earthquake-prone zones such as western South America, the Pacific Rim, and Southern Europe—demand rigorous structural engineering compliance. Procurement contracts no longer accept generic rack designs. Buyers require dynamic seismic response analysis factoring in live dynamic roller payloads.
At Guangzhou Heda Shelves Co., Ltd., all structural calculation files incorporate project-specific ground acceleration spectra, dynamic live load amplification factors, upgraded heavy-duty base plates, cold-formed Q235B/Q355B steel upright profiles, and chemical shear anchoring verified against RMI MH16.1, EN 15512, and regional codes.
3. Integration with AMR and Automated Guided Vehicle (AGV) Fleets
Warehouse automation is no longer confined to static rack configurations. Supply chain integrators are pairing gravity flow discharge buffers directly with autonomous mobile robots (AMRs) and counterbalanced AGVs. In this setup, human forklift operators load full production batches at the charging side, while laser-guided AGVs pick pallets from the discharge face on demand.
This hybrid methodology eliminates forklift labor inside staging zones and requires precision rack manufacturing: millimeter-accurate end-stop tolerances, integrated optical sensor cutouts, and dependable pallet separation to prevent vehicle docking errors.
4. Total Landed Cost (TLC) Optimization and Modular Factory Pre-Assembly
International freight volatility and local assembly labor shortages make container loading efficiency and fast jobsite installation critical purchasing parameters. Forward-thinking procurement directors favor manufacturers capable of delivering factory-tested, modular roller-track subassemblies that drop directly onto crossbeams without intensive on-site drilling or welding.
By nesting structural upright frames and utilizing custom container load packing, shipping space utilization is maximized while preventing transit abrasion on electrostatic powder coatings.
Technological Advancements in Gravity Flow Pallet Rack Systems
Decades of practical engineering refinements have transformed dynamic flow racking into a safe, controllable, and reliable warehousing solution. Discover how component innovations guarantee trouble-free continuous flow.
Self-Regulating Centrifugal Brakes
Internal planetary gear flyweights generate counteracting friction proportional to pallet speed. Whether a unit load weighs 400 kg or 1,500 kg, terminal speed is held steadily below 0.3 m/s, preventing hazardous high-speed runaway inside long dynamic channels.
Non-Contact Eddy Current Deceleration
For high-cycle and sub-zero cold operations, contactless magnetic eddy-current brake rollers offer a game-changing maintenance leap. Operating entirely via electromagnetic induction without internal mechanical brake pads, they eliminate wear, friction dust, and cold temperature freeze-ups.
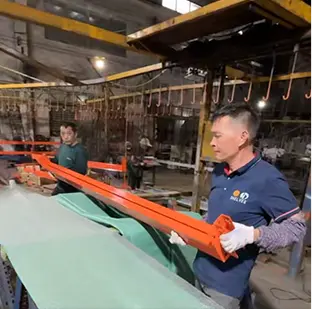
Line-Pressure Release Separators
In lanes exceeding 5 pallets deep, trailing loads exert heavy cumulative pressure against the front pallet, increasing forklift lift resistance and damaging product packaging. Automatic mechanical floor separators trap trailing pallets 300mm behind the first position, releasing them only after the front unit is fully cleared.
Structural Ramp Stops & Impact Guides
Discharge terminal ends feature heavy-gauge cold-formed steel ramp stops equipped with dual polyurethane shock dampers. These cushion the deceleration impact of incoming loads, preserving pallet integrity, structural beam stability, and building floor slab connections.
10 Precision Fabrication Steps Behind Every HEDA Racking Project
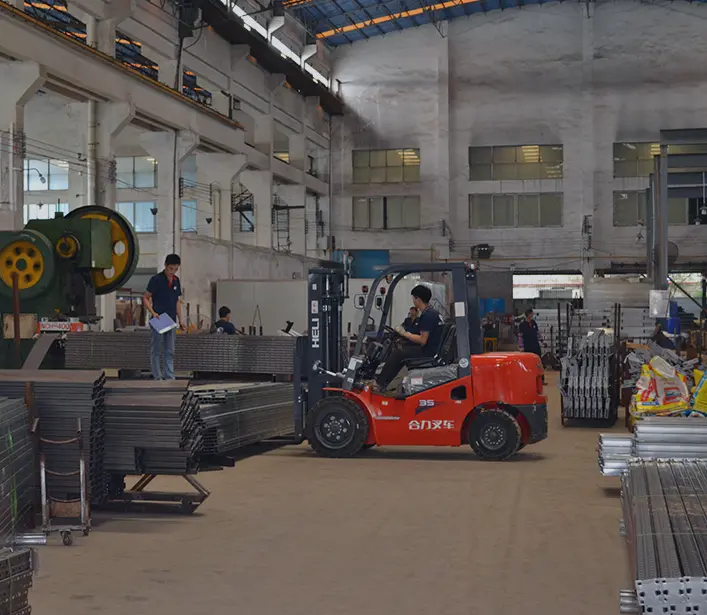
Every structural upright, support beam, and heavy-duty flow track is manufactured in-house at our 30,000 m² facility under certified CE and ISO 9001:2015 quality control regimens.
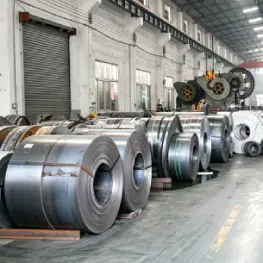 01
Raw Materials Batch Testing
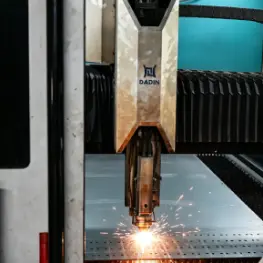 02
Precision Laser Slitting
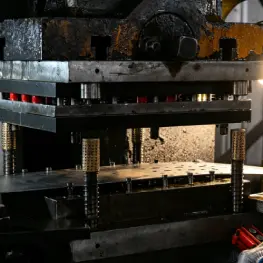 03
Automated Column Punching
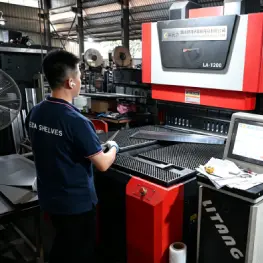 04
Cold Roll Profile Forming
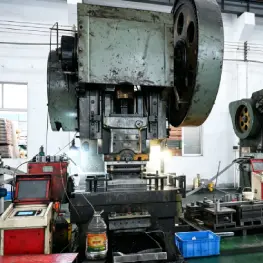 05
Step Beam Forming
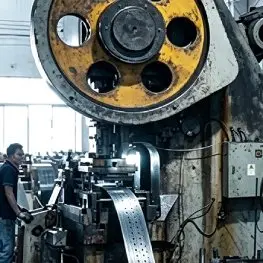 06
Automated Surface Polishing
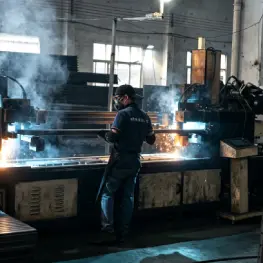 07
Robotic Structural Welding
 08
Pickling & Phosphating
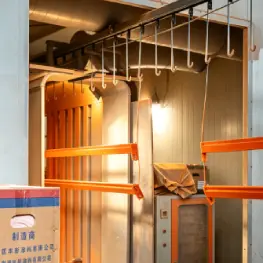 09
Electrostatic Powder Coating
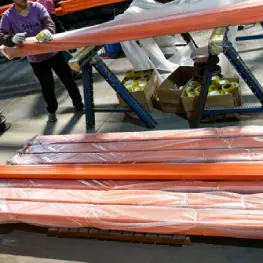 10
QC Inspection & Export Stowing
Frequently Asked Questions: Global Procurement of Gravity Flow Pallet Racks
Critical technical, mechanical, and logistical questions asked by warehouse directors, EPC contractors, and procurement executives evaluating dynamic gravity pallet racking systems.
Get a QuoteWhat pallet specifications and quality levels are required for reliable gravity flow racking?
How does pitch angle and centrifugal brake roller placement prevent pallet runaway and load jams?
Can gravity flow pallet racks operate effectively in sub-zero cold chain and frozen storage rooms (-25°C)?
How does pallet flow compare to Drive-In and Push-Back racking systems for procurement ROI?
What engineering documentation and seismic calculations are supplied with international orders?
What is the production lead time and ocean shipping protocol for full container loads?
Why Global Importers Partner with Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized steel profiling workshop into an internationally recognized warehouse storage manufacturer trusted across more than 120 countries.
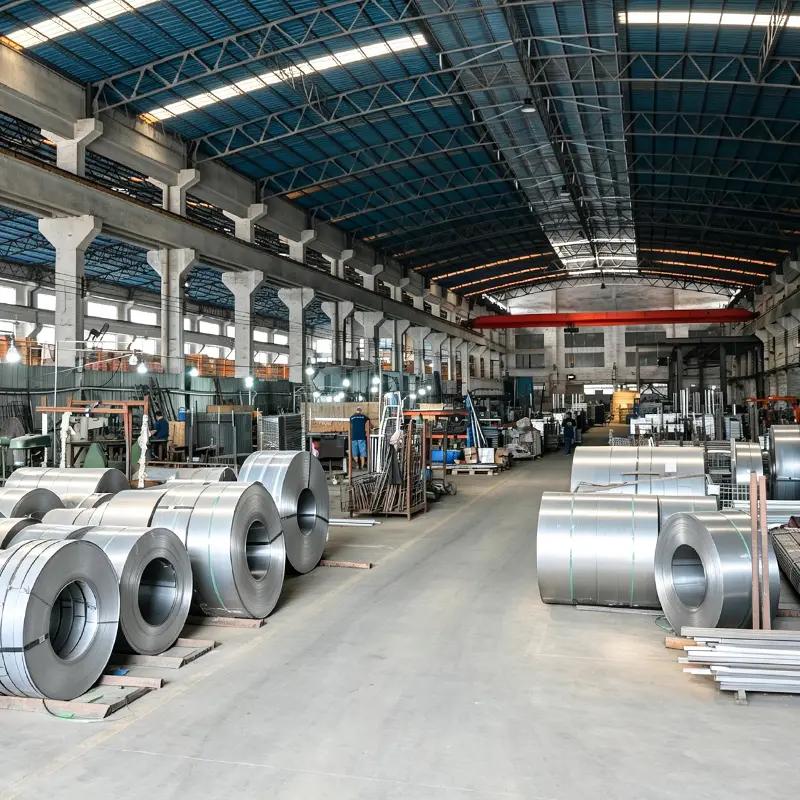
For more than 25 years, Guangzhou Heda Shelves Co., Ltd. has set rigorous standards in material selection, structural safety, and bespoke layout engineering. Our 30,000 m² advanced manufacturing facility houses state-of-the-art automated roll-forming lines, automated continuous CNC punching machinery, multi-axis robotic welding stations, and an environmentally compliant multi-stage automated electrostatic powder coating line.
When sourcing dynamic gravity flow pallet rack installations, precision manufacturing tolerances are critical. A 1mm deviation in track alignment or an unverified beam deflection can cause pallet stalling across 20-meter lanes. Our 300+ highly trained technical professionals enforce continuous batch quality testing—from raw hot-rolled steel tensile validation to bearing dynamic runout verification—ensuring that every component delivered to your destination port fits cleanly and performs predictably for decades.
International Certifications & Structural Safety Accreditations
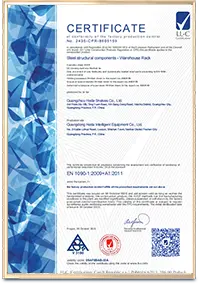
Global warehouse projects demand documented engineering compliance to satisfy local safety inspectors, institutional lenders, and industrial property insurers. Guangzhou Heda Shelves Co., Ltd. holds rigorous, independently verified accreditations available for project audit submissions:
- CE Marking: Certificate No. 2435-CPR-8605159 (EN 1090-1 Structural Steel Execution)
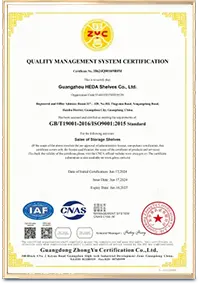
- ISO 9001:2015: Certificate No. 18624Q00169R0M (Design, Production & Quality Management)
- RoHS & REACH: Heavy-metal free electrostatic powder coatings for food and pharma


"A dependable gravity flow pallet rack demands exact balance among pitch slope, dynamic bearing friction, and line-pressure relief. We engineer every lane to preserve your loads and protect your teams."
Lead Engineering Director, Guangzhou Heda Shelves Co., Ltd.Request Your Custom Gravity Flow Layout & Engineering Quotation
Contact our engineering specialists today to receive a free 3D CAD dynamic storage layout, load analysis, and landed freight estimate within 24 working hours.
- Warehouse clear height & layout
- Pallet dimensions (W x D x H)
- Maximum & minimum pallet weights
- Operating temperature (Ambient / Freezer)