Featured Industrial Storage Systems & Heavy-Duty Pallet Racking
Explore our certified product matrix designed to maximize volumetric storage efficiency, ensure warehouse safety compliance, and streamline high-density material handling.
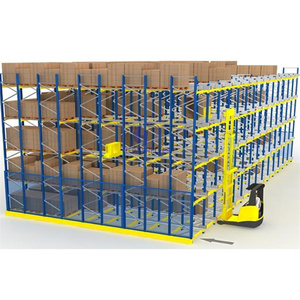
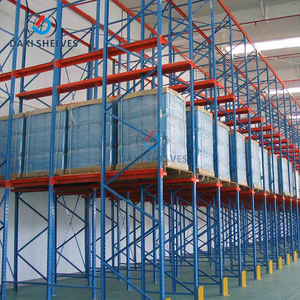
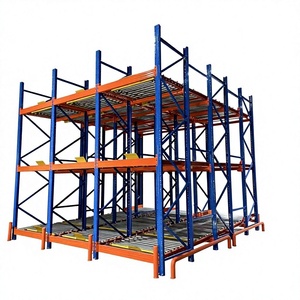
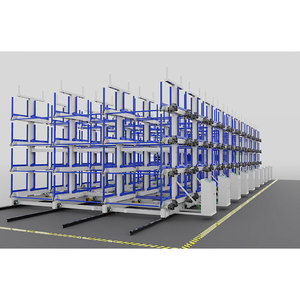
Structural Mechanics and Technical Specification of CE-Certified Drive-In Systems
An authoritative technical analysis of continuous cantilever rail design, omega upright profiles, frame buckling prevention, and EN 15512 safety compliance under heavy industrial loading.
Cantilever Rail Geometry & Load Dissipation
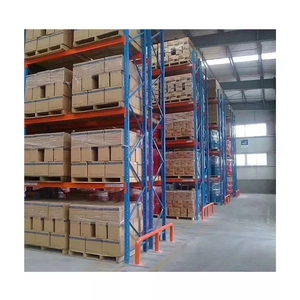
Drive-in racking eliminates conventional horizontal load beams across aisles. Instead, pallets rest on continuous cold-formed cantilever load rails supported by reinforced brackets. HEDA Shelves utilizes one-piece stamped support arms with dual-lug engagement to eliminate eccentric torsion during forklift entry and exit, ensuring zero dynamic slippage even under 1,500 kg per pallet placement.
Omega Upright Profile & High-Yield Metallurgy
Fabricated from certified Q355B high-tensile cold-rolled steel, our uprights feature an advanced 11-fold omega cross-section. This unique geometry shifts the neutral axis outwards, dramatically enhancing torsional rigidity and second moment of area ($I_x, I_y$). Uprights resist column buckling under combined vertical deadweight, live pallet surge, and wind or seismic horizontal shear.
Three-Dimensional Bracing & Top-Tie Rigidity
Because drive-in lanes lack front cross beams, global warehouse rack stability relies on upper horizontal portal beams and cross-diagonal overhead bracing. Our engineering integrates rigid back vertical K-bracing (in First-In-Last-Out drive-in bays) or overhead tie structures (in Drive-Through systems), creating a monolithic rigid box that meets strict EN 15620 sway deflection limits.
| Engineering Parameter | HEDA Drive-In Specification | Standard Market Alternative | Operational Value & Compliance Benefit |
|---|---|---|---|
| Steel Grade & Yield Strength | Certified Q355B ($f_y \ge 355\text{ N/mm}^2$) | Commercial Q235B ($f_y \approx 235\text{ N/mm}^2$) | +51% higher yield strength; smaller dead load; superior dynamic factor ($k_d$). |
| Compliance Certification | CE CPR No. 2435-CPR-8605159; EN 15512 | Uncertified / Non-CPR self-declaration | Full structural accountability; seamless building permit approval in EU & Americas. |
| Upright Forming Geometry | 11-bend cold-formed omega column | Single-channel or 6-bend post | Enhanced resistance to forklift side impact and torsional column twist. |
| Surface Pre-Treatment | 10-stage pickling, phosphating & silane wash | Manual solvent wipe down | Zero pinhole corrosion, powder-coat adhesion $> 10\text{ MPa}$ for cold rooms. |
| Floor Guidance System | Full-run hot-rolled angle steel or embedded rails | Unanchored rubber stops or none | Guarantees 100% straight forklift travel; zero rail collision damage. |
Drive-In Racking Procurement Trends (2025–2030)
How global supply chain leaders, 3PL logistics giants, and cold-chain operators are shifting their capital expenditure models to maximize cubic space and hedge against soaring real estate costs.
Cold-Chain Energy Density Optimization
With commercial electricity tariffs and industrial refrigeration costs escalating globally, cold-storage warehouses in Brazil, Chile, North America, and Europe can no longer afford wide aisles. Drive-in systems increase pallet storage capacity by up to 75% within identical cubic dimensions compared to standard selective pallet racking. This dramatically cuts refrigeration thermal loss per stored metric ton, lowering daily cold-room kilowatt-hour consumption by 32% to 40%.
Hybrid Modular Transition Paths (Drive-In to Shuttle)
Forward-thinking logistics directors are commissioning "Future-Shuttle Ready" drive-in configurations. By engineering pallet support brackets and channel geometries that allow rapid conversion to semi-automated radio shuttle tracks without dismantling main structural upright upright frames, operators safeguard their investments against future automation retrofits while minimizing initial CapEx.
Total Landed-Cost (TCO) & Green Steel Mandates
Procurement officers are shifting from simple per-kilogram pricing to rigorous Total Cost of Ownership metrics. Structural longevity, resistance to cyclic forklift impact, anti-corrosive electrostatic finishes under high humidity, and certified container stuffing efficiency (which cuts transpacific and transatlantic ocean freight fees by up to 22%) now govern multinational supply agreements.
Technological Innovations in High-Density Storage Engineering
Explore the structural enhancements, anti-collision metallurgy, and digital telemetry tools revolutionizing modern drive-in warehouse durability and worker safety.
High-Yield Polymer Impact Dampeners
Drive-in lanes experience repetitive forklift mast friction. Our newest upright shields incorporate energy-dissipating elastomeric cores coupled with 5mm heavy-gauge manganese steel sleeves, neutralizing 85% of dynamic kinetic collisions without stressing anchor bolts.
Seismic Dissipation Baseplates
Engineered specifically for active seismic regions (such as Chile's NCh 2369, Peru's E.030, and Colombia's NSR-10), our ductile dual-anchor base assemblies absorb horizontal ground motion, preventing catastrophic anchor bolt shear during severe earthquakes.
Full Cold-Room Hot-Dip Galvanizing
For deep-freezer warehouses operating at -25°C to -35°C with severe condensation risk, HEDA supplies continuous hot-dip galvanized components (BS EN ISO 1461), delivering a 70–85 micron zinc barrier impervious to micro-crack oxidation.
Digital Twin CAD & FEA Stress Mapping
Every drive-in project undergoes finite element analysis (FEA) simulating asymmetrical pallet loads, seismic spectra, and floor slab settlement, allowing our engineers to optimize steel thickness without structural over-weighting.
10 Controlled Manufacturing Stages Behind Every HEDA Rack
From certified metallurgical raw coil intake to precision roll forming and automatic electrostatic polymer curing, our 30,000 m² Guangzhou facility enforces zero-defect fabrication.
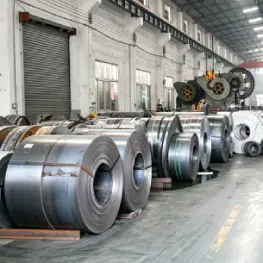
Raw Material QA
Mill test certificates (MTC) verified for yield, elongation, and chemical purity.
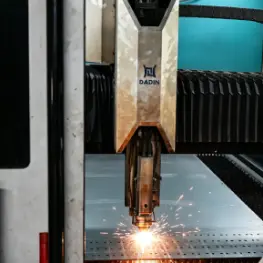
CNC Slitting
High-speed automatic rotary shearing maintaining tight ±0.2mm tolerances.
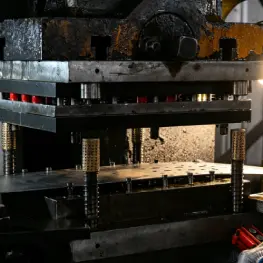
Punching Lines
Multi-ton mechanical press punch indexing 50mm / 75mm pitch holes precisely.
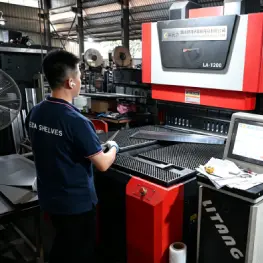
Cold Bending
Multi-roller forming stations shaping brackets and heavy support arms.
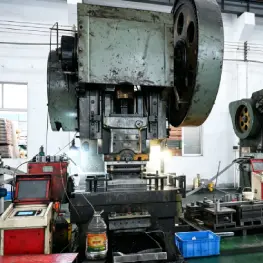
Roll Forming
Continuous computerized 24-station cold roll formers producing omega uprights.
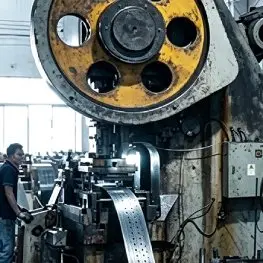
Laser & Polish
Automated seam deburring and surface preparation for uniform coating grip.
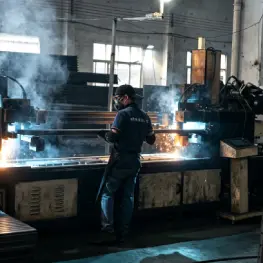
Robotic Welding
Gas-shielded robotic CO2 welding for seamless, high-penetration footplate bonds.
Phosphating
Deep acid pickling, rust removal, and dense zinc phosphate anti-rust conversion.
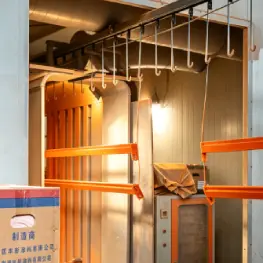
Powder Coating
Automatic electrostatic polymer spray cured in 200°C baking tunnels.
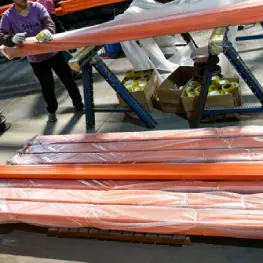
QC & Packing
Dry film thickness (DFT) checks, cross-cut adhesion tests, export wrapping.
Why Multinationals & Supply Chain Integrators Partner with HEDA
Established in 2001, Guangzhou Heda Shelves Co., Ltd. blends 25 years of structural fabrication heritage with unmatched ocean logistics support for the global racking trade.
Certified CPR CE & ISO 9001:2015
Fully accredited under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 (No. 18624Q00169R0M). Our structural load ratings are independently calculated in accordance with EN 15512, satisfying European and American insurance mandates.
Free 3D Layout & CAD Load Checks
Share your facility floor plan, clear building heights, pallet specifications, and forklift model. Within 24 business hours, our 300+ engineering team provides complete 3D warehouse simulations, structural stress checks, and container load calculations.
Global Direct Ocean Port Logistics
We manage end-to-end full container loads (FCL) to key global hubs: Santos, Valparaíso, Callao, Buenaventura, Rotterdam, Hamburg, Los Angeles, and Melbourne. Every container is 3D bundled to eliminate ocean transport vibration damage.
Comprehensive Regional Seismic Engineering
We actively customize baseplates, anchor tensile embedments, and top-portal ties according to local seismic hazard codes, including Chile's NCh 433, Peru's E.030, and Colombia's NSR-10, enabling turnkey sign-off by local structural engineers.
Frequently Asked Technical & Logistics Questions
Direct answers on structural engineering criteria, seismic calculations, lead times, corrosion protection, and container loading for procurement professionals.
Q How do Drive-In systems differ structurally from Drive-Through systems?
Drive-In racking utilizes a single entry/exit aisle under a First-In-Last-Out (FILO) logic, allowing the rear of the bay to be anchored with rigid full-height diagonal X-bracing. Drive-Through racking permits forklift access from both ends to enable First-In-First-Out (FIFO) turnover; however, because rear vertical bracing cannot be installed across through-aisles, the structure must be engineered with reinforced top-tie portal beams and oversized column baseplates to counteract lateral sway.
Q What parameters do your engineers need to prepare a 3D layout & structural check?
To deliver an audit-ready CAD layout and load calculation, we require: warehouse architectural drawings showing clear heights under joists, slab load capacity ($kN/m^2$), pallet dimensions including maximum overhang and bottom runner orientation, gross pallet weights, forklift chassis outer width, mast collapsed and extended heights, operational temperatures, and the project site location for seismic factor allocation.
Q How is CE compliance under EN 15512 verified on imported racking?
HEDA Shelves operates under CE Certificate No. 2435-CPR-8605159 in conformity with the European Construction Products Regulation (CPR 305/2011). Our cold-formed profiles are structurally calculated using finite element methods verified by physical stub column compression tests, connector shear tests, and beam bending tests according to EN 15512:2020. Mill test certificates (MTC) accompany every export container.
Q What anti-corrosion protection is recommended for cold storage & high humidity?
For standard dry food distribution, our automated 10-stage phosphating and electrostatic powder coating (60–80 μm) provides excellent durability. For cold storage freezers (-20°C to -35°C) or coastal port warehouses subject to severe condensation, we supply hot-dip galvanized components (BS EN ISO 1461) or specialized anti-microbial, low-temperature epoxy-polyester coatings to prevent zinc flaking and underfilm oxidation.
Q Can HEDA engineering accommodate heavy seismic zones in South America?
Yes. Our engineering department routinely designs racking structures compliant with regional seismic codes including Chile (NCh 433 / NCh 2369), Peru (Norma Técnica E.030), and Colombia (NSR-10). We adjust the upright profile gauge, expand baseplate footprint surface areas, specify Hilti or Fischer chemical wedge anchors, and add heavy top-truss bracing to absorb ground accelerations up to $0.45g$.
Q What is your monthly capacity and standard delivery lead time?
With an active workshop area of 30,000 m² and a dedicated team of over 300 manufacturing personnel, our monthly output exceeds 30,000 metric tons. Standard drive-in racking orders of 5 to 20 full containers typically complete production within 14 to 28 calendar days following final approval of engineering drawings.
Q How are structural components packed to prevent damage during ocean transit?
Upright frames and pallet rails are bundled using heavy-duty steel strapping, padded with corrugated corner guards, and wrapped in industrial moisture-barrier stretch film. Structural accessories, baseplates, cantilever brackets, and hardware are crated in fumigated solid-wood or steel pallet cases. Every shipping container includes a detailed digital 3D loading blueprint ensuring balanced weight distribution.
Q How is overseas on-site installation supported?
Each shipment includes comprehensive component numbering corresponding to CAD erection drawings and step-by-step assembly manuals. We provide continuous remote video engineering assistance to local installation crews, and for large distribution facilities or complex multi-tier platforms, we can dispatch seasoned installation supervisors directly to the job site.
Get Your Custom Drive-In Warehouse Layout & Quotation
Connect directly with HEDA Shelves' technical department. Send us your storage objectives, warehouse footprint, and pallet load profiles. Our engineers deliver an optimized 3D CAD design, load capacity certificate, and landed freight estimate within 24 hours.
Factory Direct Contact
Guangzhou Heda Shelves Co., Ltd.
No. 133-1, Tingyuan Road, Xingang East Road, Haizhu District, Guangzhou, China
Production Capacity: 30,000 Tons/Month
Quality Accreditations: CE CPR & ISO 9001:2015