Engineered Heavy-Duty Racking & High-Density Storage Solutions
Explore our precision-fabricated warehouse systems. Each system is cold-formed from certified high-tensile structural steel (Q235B / Q355B / S355JR), electrophoretically pre-treated, and electrostatic powder-coated for heavy industrial duty, cold chain operations, and seismic installations.
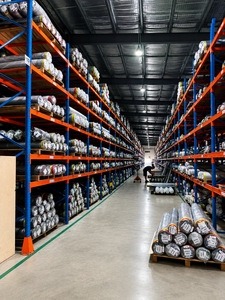
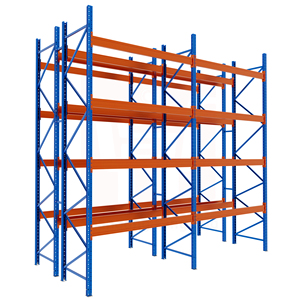
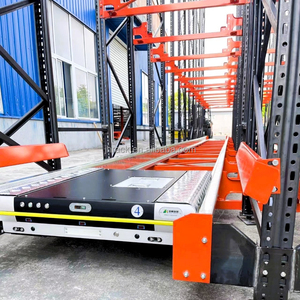
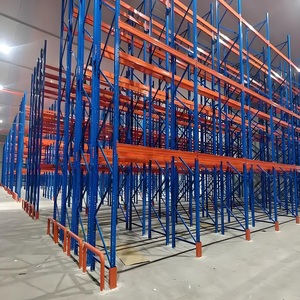
Kinematic Design & Structural Architecture of Movable Pallet Racking
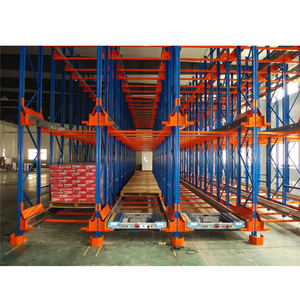
Movable pallet racking (also referred to as motorized mobile pallet racking) mounts standard heavy-duty superstructure uprights onto electrically driven motorized chassis that slide along embedded ground guide rails. By converting fixed service aisles into a single, dynamically mobilized operating aisle, movable racking expands static storage capacity by 80% to 100% within the exact same structural warehouse footprint.
Certified Compliance: EN 15095 & Machinery Directive 2006/42/EC
Because movable racking comprises powered moving machinery carrying hundreds of metric tons of dynamic live load, it is legally classified in the European Single Market as industrial machinery. HEDA Shelves engineers each movable base under EN 15095 (Power-operated mobile racking and shelving, carousel storage, and lift equipment safety requirements), incorporating redundant optical light curtains, chassis emergency bumpers, trip bars, and interlocked PLC safety circuits. Structural framing follows EN 15512:2020 limit state analysis and EN 1998-1 seismic load design combinations.
Motorized Chassis & Wheel Bogies
Fabricated using structural hollow box sections (Q355B steel) with precision-machined modular wheel assemblies. Driven by decentralized helical-bevel gearmotors with variable frequency drive (VFD) soft-start and soft-stop acceleration curves that prevent pallet displacement or tipping under full load.
Multi-Tier Safety Interlock Array
Integrated Class 4 active optoelectronic safety light grids across all aisle entrances, dual photoelectric safety sweeps mounted 50mm above the floor along the mobile base length, and dead-man physical emergency stop pushbuttons situated on every rack column face.
Floor Rail Guidance & Leveling Grouting
High-tensile steel guide rails and flat weight-distribution rails are embedded into floor slab recesses, adjusted using heavy-duty micro-leveling jacking bolts to ±1mm over 10 meters, and encased in high-strength non-shrink epoxy grout to withstand high point wheel loads.
| Storage Topology | Space Utilization Factor | Direct Pallet Accessibility | Cold Chain Energy Efficiency | Forklift Fleet Efficiency | Capital Investment (CAPEX) |
|---|---|---|---|---|---|
| Movable Pallet Racking (Motorized) | 85% – 92% Floor Cube | 100% Direct Selective Access | Maximum (Cuts refrigerated volume by up to 50%) | Standard Reach or Counterbalance Trucks | Medium – Rapid Payback (< 24 Months) |
| Standard Selective Racking | 40% – 45% (Multiple Dedicated Aisles) | 100% Direct Selective Access | Poor (High wasted volume cooled) | High forklift travel distance | Low Initial Equipment Cost |
| Drive-In / Drive-Through | 65% – 75% Floor Cube | Poor (Strict LIFO / Block Stacking) | Good, but high pallet honeycombing | Risk of truck impact inside bays | Low-Medium |
| Fully Automated ASRS (Crane High-Bay) | 90% – 95% Floor Cube | 100% Computerized Access | High efficiency, high thermal envelope | Zero manned trucks inside structure | Very High (Complex software & civil build) |
Future Procurement Trends in Industrial Storage & Movable Racking
Procurement leaders across international logistics hubs, 3PL facilities, and pharmaceutical manufacturing plants are shifting procurement criteria from raw material weight to total lifecycle engineering, ESG footprint, and digital integration capabilities.
1. Automated WMS & IoT Fleet Orchestration
Modern mobile racking systems are no longer isolated mechanical islands. Enterprise procurement contracts demand bidirectional REST API and OPC-UA connectivity between the mobile rack PLC controller and warehouse management systems (WMS). Aisles open automatically via radio-frequency tags as the forklift operator approaches, reducing cycle waiting times by up to 35%.
2. Cold-Chain Optimization & Sub-Zero ESG Mandates
With industrial refrigeration consuming up to 60% of cold store operational expenditure, compressing thermal volume is a primary decarbonization lever. Movable pallet systems in temperatures down to -30°C eliminate redundant air volume, reducing refrigeration energy loads by 40-50% while utilizing specialized cryogenic steel grades and synthetic low-temperature gear lubricants.
3. Decoupled Supply Chain & Modular Standardization
Global project planners are transitioning from monolithic proprietary installations to modular, standardized EN 15512 framing. Buyers prefer pre-engineered beam-to-column connectors with 50mm pitch adjustability, allowing warehouse reconfiguration, frame height extensions, and chassis repositioning without structural rebuilding when tenant SKU mixes shift.
Technological Development Trajectories in Heavy-Duty Mobile Storage
Continuous mechanical refinement and sensor integration are unlocking unprecedented levels of safety, energy regeneration, and speed in motorized mobile rack deployments.
Brushless DC & Regenerative Braking Systems
Next-generation mobile chassis utilize high-efficiency IE4 synchronous motors and regenerative power bus units. Kinetic energy dissipated during braking is recycled into capacitor banks or back-fed into the power grid, decreasing peak electrical load surges during simultaneous rack movements.
Predictive Structural Health Monitoring (SHM)
Integrated MEMS strain gauges, optical deflection sensors, and 3-axis vibration accelerometers track live loading variations and potential forklift impacts in real time. Cloud telemetry alerts maintenance teams to micro-misalignments or overloaded pallet beams before structural fatigue occurs.
Autonomous Mobile Robot (AMR) & AGV Symbiosis
Rather than relying solely on manned narrow-aisle forklifts, mobile racking systems are now built with floor safety radar that interfaces directly with autonomous counterbalanced lifters and automated guided vehicles (AGVs), enabling fully dark, lights-out warehouse operation.
Why Global Importers Partner with Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a state-of-the-art 30,000 m² production facility staffed by over 300 experienced structural engineers, automated roll-forming specialists, and international project managers.
Accredited CE & ISO Quality Control
Strict structural adherence to CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Certification No. 18624Q00169R0M, and RoHS compliant non-toxic electrostatic surface finishing.
Full In-House Fabrication Facility
CNC precision steel coil slitting, continuous automated multi-station cold roll-forming lines, automated punching, robotic plasma welding, and continuous phosphating pre-treatment lines.
Free 3D Layout & Seismic Engineering
Our senior structural team provides complimentary 3D rendering, CAD floor layout optimization, static finite element analysis (FEA), and seismic load calculations for local building codes.
Export Packaging & Ocean Logistics
Optimized container bundling with anti-abrasion protective wrapping minimizes ocean freight cubic displacement to key ports in South America, Europe, the Middle East, and Southeast Asia.
Frequently Asked Questions for Movable Racking Procurement
Critical engineering criteria, civil floor tolerances, lead times, and compliance benchmarks answered by our engineering directors.
What specific European safety and machinery standards govern movable pallet racking? +
Unlike standard static racking which is classified solely as a steel storage structure (under EN 15512, EN 15620, and EN 15635), movable pallet racking systems are classified as powered industrial machinery. Therefore, compliance with the following standards is mandatory for legal importation and operation within the EU and reputable global sites:
- Machinery Directive 2006/42/EC: Governs mechanical risk assessment, safety interlocks, control systems, and CE declaration of conformity.
- EN 15095: Specifically covers safety requirements for power-operated mobile shelving and racking systems.
- EN 60204-1: Dictates the electrical safety, grounding, and control circuit integrity of industrial machines.
- EN 15512 / EN 15620: Specifies cold-formed steel structural design, beam deflection limits (≤ L/200), and floor clearance tolerances.
What concrete floor slab specifications and rail installation methods are required? +
Because the cumulative weight of the mobile base, upright frames, and multiple tiers of pallets is concentrated onto steel wheel bogies, movable racking imposes high dynamic point loads on the concrete slab. Standard requirements include:
- Concrete Strength: Minimum compressive strength of C28/35 or C30/37 with steel fiber or rebar mesh reinforcement designed to handle concentrated wheel loads up to 40–80 kN per wheel.
- Floor Flatness: In accordance with DIN 18202 Table 3 Line 4 or EN 15620 tolerance classifications, rail levelness must achieve ±1 mm per 1000 mm.
- Installation Techniques: Rails can be cast directly into concrete slab troughs during new construction or retrofitted into diamond-cut floor trenches (typically 120–150mm depth) and anchored with micro-leveling jacking screws before filling with high-strength non-shrink epoxy grout.
How do motorized mobile racking systems perform in cold storage and blast freezers? +
Movable pallet racking is considered the industry benchmark for refrigerated and cold storage logistics (-20°C to -30°C). Refrigerated space is exceptionally costly to construct and cool. By eliminating 80% of empty access aisles, storage capacity within the cooled envelope is doubled.
For sub-zero environments, HEDA Shelves utilizes specialized low-temperature alloy steels that resist cold brittleness, IP65-rated drive motors, low-temperature synthetic lubricants formulated for -40°C, heated control cabinet PLC enclosures to prevent internal condensation, and heavy-duty polyurethane or low-temperature hardened steel wheels.
Can movable pallet racking be designed to withstand seismic activity? +
Yes. In earthquake-prone zones (such as Chile, Peru, Colombia, Japan, and Southern Europe), dynamic seismic actions can amplify the lateral sway of heavy upright frames mounted on movable bases. HEDA Shelves integrates seismic site parameters into our structural calculation models based on Eurocode 8 (EN 1998-1), Chilean NCh 2369, and Peruvian E.030.
Engineering upgrades include widening base chassis profiles, deploying ductile dual-flange wheel guides with anti-jump retainers, heavy horizontal and vertical X-bracing along the spine and frame bays, and automatic seismic shut-off sensors that isolate motor power and lock all chassis brakes instantaneously when ground tremor thresholds are detected.
What are the typical project lead times, shipping configurations, and installation processes? +
With our Guangzhou manufacturing plant delivering up to 30,000 metric tons per month, standard engineering and fabrication cycles for an average 3,000 to 10,000 pallet-position system range between 3 to 5 weeks following signed approval of CAD drawings.
All beams, uprights, and chassis components are precision-numbered with barcoded packing lists and nested to optimize container cubing. We provide full bilingual engineering packages: electrical schematics, foundation civil drawings, step-by-step assembly guides, and optional on-site commissioning engineers or live remote video inspection support.
What information is required to receive a comprehensive 3D layout and formal quotation? +
To enable our engineering department to configure an optimal layout and structural bill of materials, please provide:
- Architectural warehouse floor plan (DWG or PDF) noting clear interior heights, columns, utility clearances, and docking doors.
- Pallet dimensions (W × D × H including overhang) and maximum gross weight per pallet.
- Forklift make, type (counterbalance, reach truck, or articulated), lift height, and minimum turning radius.
- Operating ambient temperature (ambient, air-conditioned, or sub-zero cold room).
- Project geographic location for local seismic and wind code consideration.
Request an Engineered 3D Layout & Factory-Direct Quotation
Collaborate with HEDA Shelves' certified structural engineers. Send your warehouse floor plan today to receive a complete CAD design, structural load calculation, and comprehensive system catalog.