Engineered Heavy-Duty Racking & Containment Systems
Precision-manufactured pallet racks, shuttle systems, cantilever arrays, and integrated safety net assemblies designed to prevent rear pallet push-through, falling debris, and operational hazards in high-throughput distribution hubs.
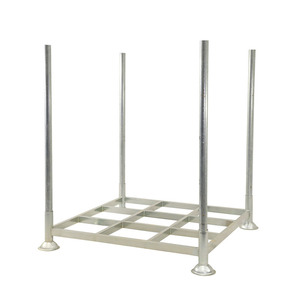
Customizable Heavy Duty Galvanized Stacking Rack Warehouse Factory Logistics Steel Pallet Rack Stillage
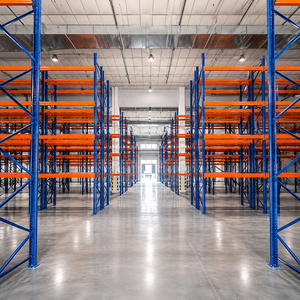
Heavy Duty Pallet Rack 1000KG 2000KG Per Level Metal High Density Free 3D Design Q235B Steel Shelving
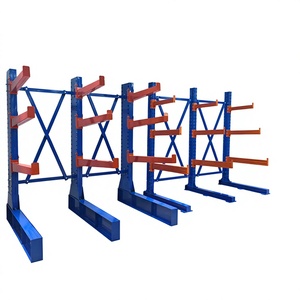
Single/Double Side Heavy Duty Cantilever Rack System Warehouse Storage Long Item Pipes Lumber Steel with Adjustable Arm Rack
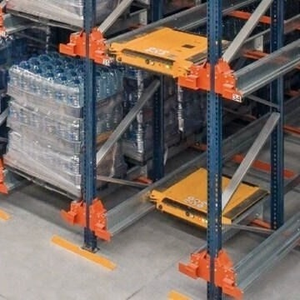
Fully Automated Radio Shuttle Racking Featuring High-Speed Shuttle Cart for Modern Logistics Distribution Centers
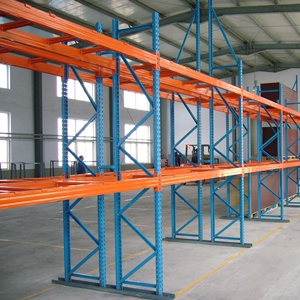
Adjustable Heavy Duty Pallet Rack Shelf Two Levels Custom High Load Capacity Industrial Warehouse Storage Pallet Racking System
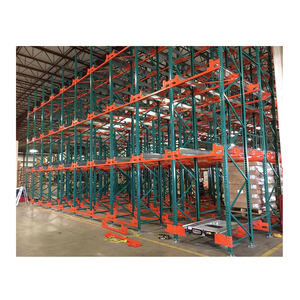
Heavy Duty Automatic Radio Shuttle Rack High Efficiency Automated Pallet Storage Racking System FILO/FIFO
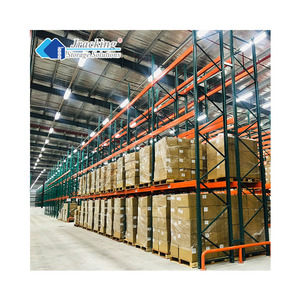
JRACKING Heavy Duty Industrial Warehouse Shelves Steel Teardrop Pallet Racking System For Logistics Center Storage
Steel Structure Factory Building Prefab Warehouse Commercial Office Hangar Prefabricated Steel Workshop Buildings
Engineering Whitepaper: The Critical Mechanics of Pallet Racking Fall Containment
In modern multi-tier warehousing and high-bay distribution centers, pallet rack safety extends far beyond load-bearing column capacities. The sudden displacement of loose cartons, shrink-wrap failures, or forklift over-push incidents in selective, drive-in, or radio shuttle bays represent catastrophic hazards to personnel and inventory. As an internationally certified CE certified pallet racking nets manufacturer & exporter, Guangzhou Heda Shelves Co., Ltd. pioneers integrated dynamic containment solutions designed in accordance with European Norms (EN 1263-1, EN 15512) and OSHA 1910.176(b) material handling safety directives.
Technical Authority Takeaway: Pallet rack nets do not simply function as passive barriers; they act as engineered energy-absorption membranes. When an unstable 1,200 kg pallet shifts at a 9-meter elevation, the net's tensile elongation must absorb dynamic kinetic energy without shearing anchors or transferring eccentric torsion to structural racking uprights.
Material Science: High-Tenacity Polypropylene (HTPP) vs. Knotted Polyamide vs. Steel Mesh
Specifying pallet racking nets requires an empirical understanding of polymeric tensile behavior, environmental degradation, and elongation mechanics under shock loading. Unlike traditional rigid steel wire partitions that permanently buckle upon forklift tine collision or product impact, synthetic polymeric netting distributes kinetic impact across high-energy multi-filament cords:
| Material Specification | Tensile Strength (Mesh Cord) | Elongation at Break | Cold Chain (-30°C) Resilience | Primary Industrial Application |
|---|---|---|---|---|
| Knotless HTPP (High-Tenacity Polypropylene) | 2.8 kN – 4.2 kN per cord | 18% – 25% (Elastic Recovery) | Exceptional (Zero embrittlement) | Universal high-bay rack rear fall containment |
| High-Tenacity Polyester (PET) Webbing | 15.0 kN – 25.0 kN per strap | 12% – 15% (Controlled deflection) | High stability across thermal cycles | Heavy unit load push-through restraint (bay front/rear) |
| High-Strength Polyamide (Nylon 6,6) | 3.5 kN – 5.0 kN per cord | 28% – 35% (High deflection) | Moderate (Moisture absorption risk) | Overhead conveyor and high-velocity carton lines |
| Galvanized Wire Mesh Screen (Rigid) | Yield 350 N/mm² (Welded joint) | < 3% (Plastic deformation) | Prone to weld fatigue under vibration | Secure tool rooms, hazardous chemical cages |
Our manufacturing facility utilizes UV-stabilized, high-tenacity knotted and knotless polypropylene mesh cord diameters ranging from 3.0mm to 5.0mm, paired with mesh aperture dimensions of 25mm to 100mm. Every batch undergoes rigorous elongation-at-break validation and pendulum impact destruction tests under CE compliance certificate No. 2435-CPR-8605159, ensuring consistent resistance against heavy box blow-outs and pallet over-travel.
Strategic Procurement & Future Industry Trends
Global supply chain expansion, automation retrofits, and stringent warehouse labor safety compliance are fundamentally transforming pallet rack containment procurement across the Americas, Europe, and Asia-Pacific.
1. Shift from Rigid Steel Screens to Dynamic Polymer Netting
Procurement directors are actively decommissioning traditional welded steel backstops in favor of modular, cable-tensioned polymer netting. Netting systems offer up to 70% lighter dead-load on racking columns, rapid retrofitting without hot-work permits, and complete resistance to permanent indentation from minor pallet taps, slashing lifecycle maintenance costs.
2. AS/RS and Radio Shuttle Deep-Lane Integration
With the meteoric rise of Automated Storage and Retrieval Systems (AS/RS) and radio shuttle configurations, high-speed automated carriers demand fail-safe containment at the dead-ends of deep lanes. Modern procurement mandates high-tension safety nets capable of catching high-speed runaway pallets without disrupting photoelectric sensors.
3. Strict CE & Third-Party Audit Enforcement
Insurance underwriting bodies and warehouse audit boards across South America (Brazil, Chile, Peru, Colombia) and the EU now mandate traceable batch testing certificates. Buyers reject generic uncertified nettings, standardizing exclusively on CE certified, flame-retardant (DIN 4102 B1 compliant), and UV-stabilized solutions.
4. Turnkey Bundled Procurement: Racks + Engineered Netting
Global procurement teams no longer source racks from steel mills and safety barriers from separate hardware brokers. Bundling structural racking—such as selective beams, teardrop uprights, and shuttle rails—with pre-engineered, factory-drilled safety netting kits guarantees exact mechanical compatibility, precise standoff bracket offsets, and uniform seismic certifications.
Seismic Zone Adaptation & Cold Chain Environmental Durability
Exporting warehouse storage systems to seismic corridors—including the Andean fault zone across Chile (NCh 2369 / NCh 433), Peru (Norma E.030), and Colombia (NSR-10)—imposes severe structural dynamics. During a seismic event, high-bay racking systems undergo horizontal sway, inter-story drift, and dynamic harmonic oscillations. Rigid retaining walls can fail at joint weldments, sending full pallets crashing into pedestrian picking aisles.
HEDA Shelves engineers integrate high-elasticity safety netting arrays directly into the structural calculation models. By utilizing precision-tensioned stainless steel aircraft cables (Grade 304/316) anchored via heavy-duty offset standoff brackets (ranging from 75mm to 300mm), the netting system allows pallets to shift within tolerable structural clearance envelopes without falling off the rear beam, thereby preventing catastrophic progressive rack collapse.
In refrigerated storage facilities (-25°C to -35°C), low-grade polymers undergo severe glass transition crystallization, becoming brittle and snapping under minimal contact. Our cold-chain certified polypropylene and nylon blends incorporate advanced aliphatic additives, ensuring full kinetic energy absorption and flexibility even in blast-freezer conditions.
Why Global Importers Partner with HEDA Shelves
Direct factory control, 25 years of engineering mastery, and end-to-end accountability from raw coil steel slitting to global freight container loading.
30,000 m² Production Base
Fully equipped in-house manufacturing lines: automated roll forming, computerized CNC column punching, robotic welding cells, and high-speed electrostatic powder coating tunnels.
Free 3D Layout & Structural FEA
Experienced warehouse designers generate complete CAD architectural blueprints, 3D realistic renderings, and finite element stress calculations customized to your forklift fleet and floor slab.
30,000 Tons Monthly Capacity
High-volume processing capacity ensures standard racking and safety net hardware orders ship in 2 to 4 weeks, with phased batching configured for mega-project construction schedules.
Certified International Standards
Full regulatory adherence: CE Mark (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management certification (No. 18624Q00169R0M), and SGS material compliance audits.
Anti-Corrosion Pretreatment
Steel components undergo industrial 8-stage automated pickling and phosphating before electrostatic curing, guaranteeing superior adhesion in tropical and coastal shipping hubs.
Optimized Sea Freight Packing
Precision container load plans maximize cubic meter utilization, utilizing custom steel cradles and protective wrapping to safeguard powder finishes through 30-45 day ocean voyages.
Tailored OEM & ODM Support
We engineer customized dimensions, bespoke bracket geometry, distinct color schemes, and private-label packaging for regional racking distributors and safety equipment importers.
Remote & On-Site Guidance
Every export delivery features numbered component labeling, clear assembly schematics, video guidance protocols, and optional on-site engineering supervision for complex mezzanines.
Pallet Racking Safety Nets & Storage Procurement FAQ
Authoritative technical answers to assist warehouse operators, facility managers, and international procurement specialists.
What European and international safety standards govern pallet rack safety netting? +
How do I calculate the correct mesh size, cord diameter, and bracket offset for my racks? +
Can safety nets be retrofitted onto existing selective and teardrop pallet racks? +
How do synthetic polymer nets perform in cold storage and freezing facilities? +
What information is required to receive a comprehensive CAD design and quotation? +
What are your sea freight logistics, lead times, and port handling capabilities? +
Ready to Engineer a Safer, High-Density Storage Facility?
Consult directly with our senior warehouse racking engineers. Receive complimentary 3D visual renderings, finite element structural calculations, and competitive factory-direct pricing for CE certified pallet racking safety netting and industrial storage systems.
Inquire Now