Engineered High-Bay & Mezzanine Storage Systems
Precision-manufactured in compliance with EN 15512 and FEM 10.2.02 racking standards, serving cold chain facilities, agricultural distributors, heavy industrial hangars, and automated fulfilment centers.
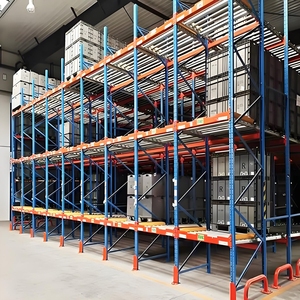
Industrial Heavy-Duty Drive-In Pallet Rack Solution
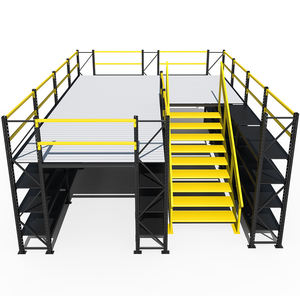
Steel Mezzanine Floor Warehouse Storage Racking
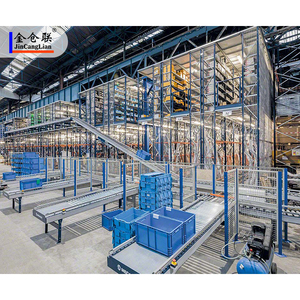
Intelligent Radio Shuttle Robot Pallet Racking
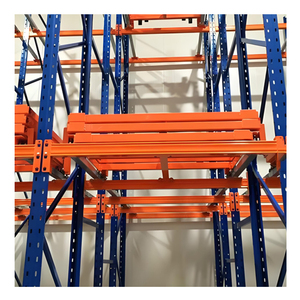
Heavy Duty Push-Back Roller Cart Pallet Rack

Prefabricated Structural Steel Warehouse & Workshop
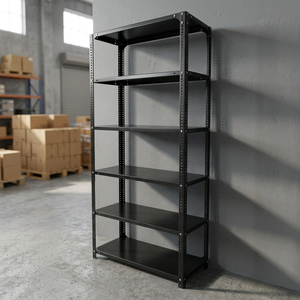
Precision Slotted Angle Industrial Storage Rack
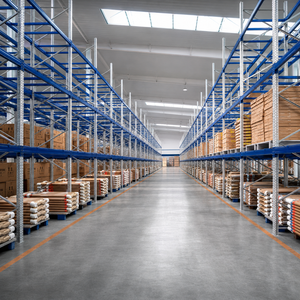
Schwerlastregal Adjustable Multi-Level Pallet Shelving
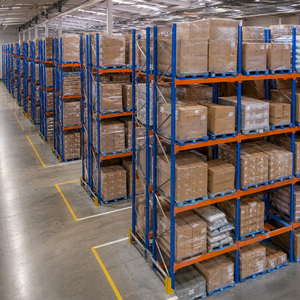
Heavy Duty Q235B E-Commerce Pallet Racking System
Structural Rigidity, CE Verification & Metallurgical Integrity
When selecting an industrial racking manufacturer, engineering documentation and mechanical load validations must be transparent. Here is how our certified fabrication process mitigates structural risk.
Q235B & Q355B Certified Steel
We source prime mill-tested coils with verified yield strengths (minimum 235 to 355 MPa) and guaranteed elongation rates over 26%, essential for energy absorption during dynamic seismic events.
- 3.1 Mill Test Inspection Certificates
- No recycled composite or mixed-grade billets
- Charpy V-Notch impact tested for cold chains
CE Mark: EN 15512 & EN 1090-1
Factory Production Control (FPC) audited under European harmonized standards. Our calculations ensure upright frame deflection does not exceed H/200 and beam deflection remains safely inside L/200 under maximum rated load.
- Declaration of Performance (DoP) on batch runs
- EN 15620 operational clearance alignment
- 1.5x structural safety coefficient factored
Corrosion & Surface Treatment
Every profile undergoes continuous chemical pickling, alkaline degreasing, and zinc phosphating before electrostatic curing with TGIC-free polyester resin powder at 200°C for superior chemical resistance.
- 60 to 80 μm certified coating thickness
- 500-hour ASTM B117 salt spray compliance
- HDG (Hot Dip Galvanized) options available
Seismic Design Protocol for High-Risk Fault Zones
Pacific Rim & Andean Alignment
Racking systems deployed across seismic hotspots require ductile moment connections and upgraded chemical anchor diameters (M12 to M16) rated for uncracked concrete conditions.
X & K-Bracing Sizing
Vertical frame bracing profiles are engineered based on finite-element modal analysis, neutralizing horizontal torsional shear forces during peak ground acceleration (PGA > 0.4g).
Baseplate Thickness & Spacing
Upright bottom anchor plates are increased up to 10-14mm thickness with dual-hole patterns, dispersing down-aisle dynamic loads directly into foundation slabs.
Warehouse Racking Procurement Trends (2025–2030)
Global supply chain leaders are fundamentally transforming racking procurement from simple steel commodity buys into technologically integrated capital investments.
ASRS & Shuttle-Ready Engineering
Procurement teams are shifting away from traditional static selective racking toward four-way radio shuttle channels and Autonomous Mobile Robot (AMR) top-deck mezzanines. Millimeter-accurate beam level tolerances (±1.5mm) ensure uninhibited automated robotic movement.
Low-Carbon Steel & Circularity
Driven by corporate ESG targets and European CBAM carbon border mechanisms, procurement briefs now prioritize electric arc furnace (EAF) steel sourcing, non-toxic heavy metal-free powder coatings, and modular bolt-together frames designed for zero-waste warehouse redesigns.
Thermal Efficiency Compression
Escalating industrial refrigeration costs demand maximum density per cubic meter. Drive-in and multi-deep pallet flow systems designed for -30°C freezer facilities prevent frost-heave buckling and structural brittleness through low-temperature modified alloy engineering.
Why Global Importers Partner Directly With Our Factory
Direct accountability from cold coil slitting through robotic welding and final port container stuffing ensures lower landed costs and zero quality disputes.
30,000 m² Production Base
Equipped with 10 high-speed rolling production lines, 8 continuous CNC stamping punches, and dual automatic powder coating tracks yielding 30,000 metric tons monthly capacity.
Free 3D Layout & Structural BIM
Submit your warehouse AutoCAD dwg files. Our structural team provides customized 3D spatial renders, aisle turn radius calculations, and structural static simulations within 24 hours.
Dual CE & ISO 9001:2015
Full CE Certificate compliance (No. 2435-CPR-8605159) and ISO 9001:2015 registration guaranteeing third-party traceable steel origins, dimensional accuracy, and weld integrity.
Optimized Container Load Plans
Computer-optimized container bundling minimizes ocean freight per pallet position while protecting powder coatings against sea-freight moisture and transit damage.
Frequently Asked Questions by Industrial Racking Buyers
Straight answers on certifications, structural engineering validations, lead times, ocean container logistics, and on-site assembly.
What is the practical difference between Q235B and European S235JR steel?
Q235B and EN 10025-2 S235JR share comparable mechanical properties, both featuring minimum yield strengths of 235 N/mm² and ultimate tensile strengths of 370–510 MPa. Our Q235B is tested for Charpy impact resistance at 20°C, ensuring compliance with European racking design codes (EN 15512).
Can your engineers calculate seismic parameters for Chile, Peru, or the US?
Yes. Our engineering office performs structural calculations accounting for site-specific ground acceleration (PGA), soil response spectra, and seismic risk tiers. We design upgraded footings, anchor embedment depths, and bracing in accordance with NCh 2369 (Chile), E.030 (Peru), or RMI ANSI MH16.1 (USA).
How do you guarantee finish durability in coastal and humid facilities?
We apply a multi-stage pre-treatment starting with hot acid pickling and zinc phosphating to eliminate surface scale. We then apply an electrostatic dry powder coating baked at 200°C. For extreme humidity, marine zones, or outdoor applications, hot-dip galvanizing (HDG) per ISO 1461 is available.
What is the standard production lead time for full-container projects?
Standard pallet racking orders of 1 to 5 40ft HQ containers are fabricated in 15 to 25 business days following final CAD sign-off. Engineered heavy mezzanine structures or specialized automated shuttle tracks are produced in scheduled batches of 20 to 35 days matching construction site readiness.
How is mechanical installation handled in overseas destination markets?
Every consignment features piece-marked structural components keyed to comprehensive 2D/3D assembly schematics and packing lists. We provide remote video engineering support for local millwright teams and can dispatch senior project supervisors to oversee large-scale high-bay installations.
What specific details are needed to generate an exact layout proposal?
To produce an optimized CAD proposal, provide your building floor plan (clear height to lowest ceiling obstruction), pallet footprint (L x W x H inclusive of cargo overhang), maximum gross pallet weight, forklift model and mast lift capability, and your target operational throughput (FIFO vs. LIFO).
Accelerate Your Warehouse Capacity With Direct Manufacturer Engineering
Send your warehouse dimensions or cargo handling parameters to our engineering desk. Receive an EN 15512 compliant layout plan, capacity analysis, and direct factory pricing within 24 hours.
Inquire Now