Industrial Storage Architecture: Total Safety, Precision Engineering & Global Compliance
In the contemporary omnichannel fulfillment landscape, modern distribution centers, cold stores, and industrial staging hubs require substantially more than off-the-shelf shelving. The modern supply chain mandates CE-certified, structurally validated racking systems capable of withstanding dynamic live pallet loadings, continuous material handling equipment (MHE) impact cycles, and site-specific seismic accelerations. As a leading manufacturer founded in 2001, Guangzhou Heda Shelves Co., Ltd. (operating an expansive 30,000 m² automated production facility with a monthly capacity exceeding 30,000 tons) engineers advanced structural solutions compliant with rigorous European Standards (EN 15512, EN 15620, EN 15629, and Construction Products Regulation CE Certificate No. 2435-CPR-8605159).
Selecting an international racking exporter requires calculating the Total Cost of Ownership (TCO), which factors in certified high-tensile steel grades (such as Q355B and S355JR), zinc phosphate pre-treatment anti-corrosion chemistries, finite element design analyses (FEA), and optimal 40ft High Cube container volumetric packaging. This technical whitepaper establishes the criteria for evaluating heavy-duty storage configurations, details procurement trends for 2026–2030, and provides technical teardowns of 8 primary industrial configurations engineered for high-throughput global operations.
Engineered Heavy-Duty Racking & Warehouse Infrastructure
Every system is custom-profiled from certified high-yield hot and cold-rolled structural steel, treated through an automated 10-stage process, and tailored to pallet metrics, forklift mast dimensions, and local seismic parameters.
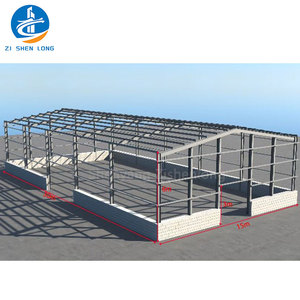
Metal Frame Structure Prefabricated Warehouse/ Workshop/ Hangar/ Steel Structure Building
- Grade: High-yield Q355B / Q235B Primary Beams
- Seismic: Wind load up to 150 km/h, seismic Grade 8
- Scope: Complete portal frame, purlins, roof/wall cladding
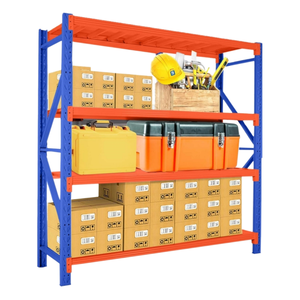
Bolted Longspan Detachable Multi-Level Steel Corrosion Protection Industrial Shelves Heavy Duty Pallet Racking For Warehouse
- Capacity: 1,000 kg – 4,500 kg per beam level
- Pitch: 50mm / 75mm multi-claw interlock connectors
- Surface: Epoxy powder coating (60–80 microns)
High Efficiency Auto Rack Shuttles Warehouse Racking Stacking Racks & Shelves Storages Rack Pallet Shuttle System
- Speed: 0.8m/s (unloaded), 0.6m/s (loaded up to 1500kg)
- Battery: 48V Lithium-ion with quick-swap cart architecture
- Logistics: Dual FIFO & LIFO capability, WMS integration
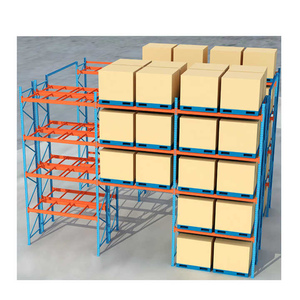
Direct Factory Sale High-Density 5-Layer Metal Drive-In Racking System for Warehouse Storage 2000kg Load Capacity
- Floor Utilization: Up to 80% footprint reduction
- Rails: Single/double side cantilever structural guide rails
- Environment: Cold-storage resilient down to -30°C
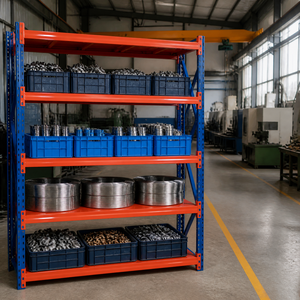
Custom Adjustable Anti-Rust Storage Metal Stacking Racks Pallet Racking System Steel Shelving VNA Racking Narrow Aisle Rack
- Aisle Width: Ultra-narrow 1,600mm – 1,800mm operating aisle
- Height: Clear lift heights to 15+ meters with wire guidance
- Access: 100% individual pallet selectivity
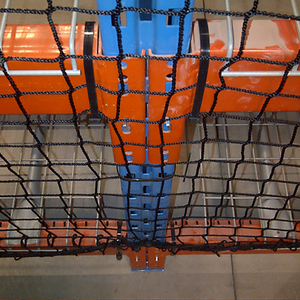
Heavy Duty Warehouse Storage Protection Pallet Rack Safety Net
- Material: High-tenacity knotless polypropylene (PP) / PE
- Impact Resistance: Designed to contain 1,500kg carton slips
- Fastening: Heavy-duty snap hooks and galvanized aircraft cables
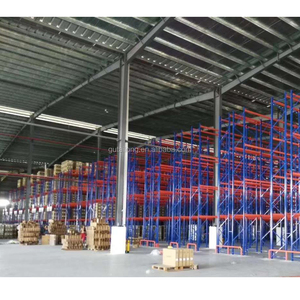
Drive-Through Pallet Racking Heavy Duty Steel Corrosion Protection 3-Layer High Capacity Adjustable Plug-In Industrial Rack
- Strategy: FIFO throughput with dual forklift access points
- Protection: Structural floor guide angles & bollards included
- Upright Frame: Omega section 90mm/100mm/120mm profile
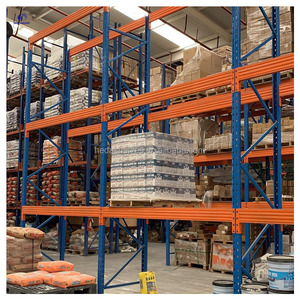
Commercial Warehouse Racking Material Handling Racking Systems Warehouse Racking Supplies
- Components: Mesh decking, pallet support bars, row spacers
- Safety Factor: Conforming to FEM 10.2.02 and EN 15512
- Customization: Custom RAL color matching & galvanized finishes
Engineering Verification: Why CE Certification Dictates Warehouse Safety
Racking collapses rarely result from manufacturing defects alone; they stem from incomplete structural finite element modeling, incorrect base plate anchoring, and neglecting lateral displacement forces. Here is how rigorous certification ensures facility safety.
EN 15512 & CE 2435-CPR Compliance
Under European Standard EN 15512:2020, rack load-bearing capacities cannot be estimated by theoretical column calculations alone. Upright frames, beam connector brackets, and mechanical locking pins undergo continuous stub-column compression tests and cyclic connector shear tests. HEDA Shelves holds accredited CE Certificate No. 2435-CPR-8605159, certifying full compliance for structural steel storage racks.
Dynamic Seismic Resistance (P-Delta Effects)
For installations situated in high-seismic zones—such as the Andean Belt (Chile NCh 2369, Peru E.030, Colombia NSR-10) or Southern Europe—standard racking without diagonal bracing fails under lateral accelerations. Our engineering team incorporates dynamic second-order (P-Delta) structural modeling, upgrading base plate surface area, anchoring embedment depth, and moment-resisting portal frames.
Full 3D CAD & Structural Design Support
Every industrial project begins with a complimentary comprehensive 3D layout and structural analysis tailored to your building clear height, slab thickness, column grid, MHE turning radius, and SKU throughput velocity. We supply full CAD fabrication sets and calculation verification sheets to satisfy municipal building inspectors and insurance underwriters worldwide.
| Evaluation Parameter | Generic Non-Certified Steel Racking | HEDA Shelves CE-Certified Infrastructure | Operational Safety & Business Impact |
|---|---|---|---|
| Steel Grade & Yield Strength | Commercial grade Q195 / mixed scrap (Yield ≤ 215 MPa) | Certified prime Q235B / Q355B (Yield ≥ 355 MPa, Tensile to 510 MPa) | 65% greater resistance to beam deflection and lateral column buckling under peak static loads. |
| Punching Precision & Pitch | Mechanical single punch, pitch tolerances ±1.5mm | Continuous CNC multi-station hydraulic punching (±0.1mm tolerance) | Zero beam distortion, uniform weight transfer to uprights, elimination of localized shear failure. |
| Surface Pre-Treatment | Manual solvent degreasing or basic spray wipe | Automated 10-stage chemical pickling & zinc phosphating line | Eliminates micro-oxidation beneath paint; 500+ hours salt spray resistance (ASTM B117 compliant). |
| Seismic Calculation Verification | Static gravity load calculations only | Dynamic spectral analysis modeled against regional building codes | Full structural insurance approval and zero seismic failure across 10,000+ worldwide sites. |
| Container Loading Architecture | Loose packing, hand-stacked with wood dunnage | Custom structural steel dunnage & shrink-film bundle engineering | Eliminates transit scuffing, bent flanges, and maximizes 40HQ container cube utilization to 98%. |
10 Controlled Production Stages Behind Every Component
From raw coiled steel from certified domestic mills to multi-layer protective packaging for trans-oceanic transit, our 30,000 m² factory operates under an ISO 9001:2015 certified Quality Management System (Certificate No. 18624Q00169R0M).
Raw Steel Inspection
Spectrometer analysis, tensile coupon testing, and ultrasonic thickness verification of incoming coils.
Precision Slitting
High-speed laser slitting with CNC edge deburring to ensure uniform flange geometry across all components.
Automated Punching
Continuous hydraulic stamping producing teardrop, diamond, and butterfly connector slots at exact 50/75mm pitches.
Cold Roll Forming
Multi-stand roll forming mills shaping complex multi-bend Omega uprights with structural hardening ribs.
Box-Beam Interlock
Continuous twin-C seam welding forming rigid tubular box beams that eliminate torsional twisting.
Robotic Arm Welding
ABB six-axis robotic weld cells attaching multi-claw end connectors with complete weld bead penetration.
Surface Polishing
Automated shot-blasting and mechanical scale removal to achieve SA 2.5 surface roughness profiling.
Chemical Phosphating
Multi-stage immersion bath: alkaline degreasing, acid pickling, rust removal, and dense microcrystalline phosphating.
Electrostatic Coating
Nordson automated powder coating booth using lead-free epoxy-polyester cured in 200°C infrared baking tunnels.
Export Pack & QC
Batch cross-hatch adhesion testing, ultrasonic dry film thickness checks, and modular steel-band bundle strapping.
Global Procurement & Technology Trends Shaping Racking Infrastructure
Logistics procurement executives and EPC contractors face shifting supply-chain realities. Aligning your capital expenditure with next-generation automated trends yields operational advantages across the asset lifecycle.
AS/RS & Shuttle Transition
Rising labor and warehouse footprint costs are accelerating the migration from pure selective forklift racking to semi-automated pallet shuttle systems and mini-load AS/RS crane infrastructure. Future-proofing requires procuring rack columns with tighter manufacturing tolerances capable of automated vehicle guidance.
Cold Chain Thermal Efficiency
With global agribusiness, seafood, and pharma cold chains expanding, refrigerated warehouses represent high capital investments. High-density radio shuttle and deep drive-in racks maximize usable cubic meters, cutting refrigeration power consumption by up to 35% per stored pallet position.
Steel Volatility Hedging
Forward-thinking supply chain directors manage raw material fluctuations by partnering directly with scaled manufacturers holding substantial coil inventories. Direct factory sourcing eliminates domestic middleman markups and guarantees price stabilization throughout multi-month construction phases.
Smart Deflection Sensors
Modern warehouse asset managers are piloting structural sensor arrays mounted on high-bay uprights to capture real-time MHE collisions, floor subsidence, and dynamic load deflections. HEDA Shelves engineers systems with mounting channels ready for industrial IoT sensor integrations.
Frequently Asked Questions for Warehouse Racking Importers & EPCs
Direct answers to the structural, logistical, and commercial inquiries routinely reviewed during international procurement evaluations.
Ready to Optimize Your Logistics Footprint?
Whether you are constructing a 50,000 m² regional distribution center, upgrading an agricultural cold-storage facility, or expanding industrial parts storage, consult directly with HEDA Shelves' dedicated engineering team. We deliver certified structural precision, factory-direct manufacturing savings, and end-to-end container logistics support.
Connect with an Engineer
Access our comprehensive 2026 warehouse racking technical catalog, load capacity matrices, and material test reports.
Get Catalog