Engineered Warehouse Storage & Medium-to-Heavy Duty Solutions
Custom-fabricated cold-rolled profiles engineered to optimize cubic storage volume, reduce order fulfillment latency, and withstand demanding seismic and dynamic cycles across logistics hubs.
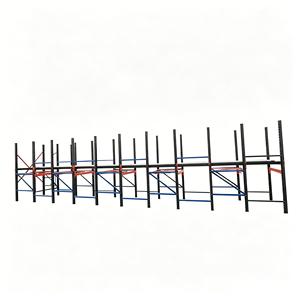
Custom Heavy Duty Drive-In Storage Rack, High Strength High Load Through Type Warehouse Pallet Racking
Continuous drive-through bay architecture removing working aisles for up to 80% footprint utilization in cold storage and high-batch SKUs.
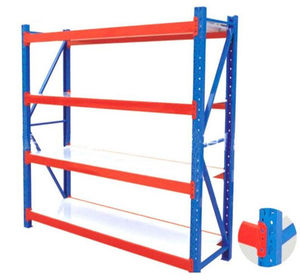
High Warehouse Adjusted Heavy Duty Pallet Racking Stacking Racks From Chinese Supplier Store Display Stand Heda Shelf Super Mall
50mm/75mm adjustable pitch beam connectors with 5-tooth security locks offering instant access to every SKU across FMCG distribution.
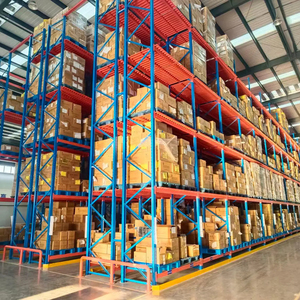
3000kg Capacity Pallet Racking System for Manufacturing Workshop Bolted Connection Load Accept OEM & ODM
Heavy structural box-beam configurations with high-tensile 8.8-grade bolted base frames, built for stamping dies and automotive subassemblies.
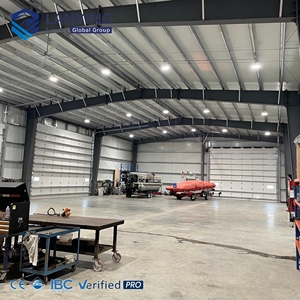
Versatile Industrial Steel Structure Warehouse For Logistics Distribution Center And Large Scale Cargo Storage
Rack-clad building structures where upright columns carry both inventory dead loads and exterior roof/wall wind resistance profiles.
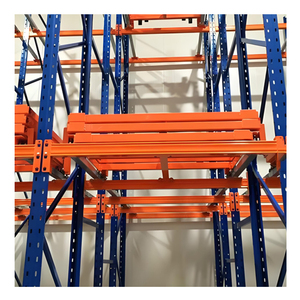
DJ Heavy Duty Pallet Racking Storage System Steel Warehouse Gravity Push Back Roller Sliding Rack with Corrosion Protection
Telescoping nested gravity carts operating on inclined steel rails, enabling 2 to 6-deep pallet storage without forklift bay entry.
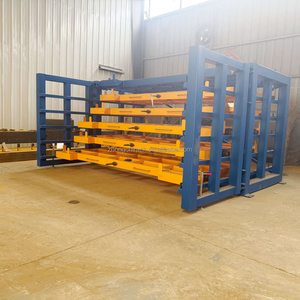
Heavy Duty Drawer Style Sheet Metal Rack Industrial Storage Rack for Workshop Material Handling
100% roll-out cantilever drawers allowing overhead crane access for metal plate packs, laser cutting stock, and heavy fixtures.
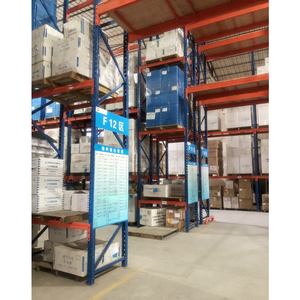
Custom Height Layer Beam Pallet Racking Rust Proof Surface Treatment Heavy Duty Warehouse Cargo Stacking Rack
Pre-treated with automated 9-stage pickling and phosphating lines followed by outdoor-grade thermosetting powder coat to resist marine salt-fog.
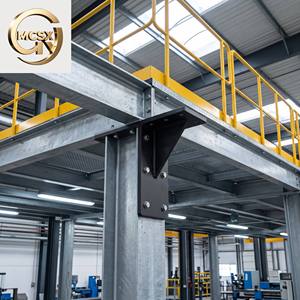
Powder-Coated Iron T-Frame Support - Custom Welded Structural Components for Industrial Shelving
Heavy-gauge welded structural T-frame assemblies for multi-tier picking towers, intermediate mezzanines, and high-density archive shelving.
Engineering Selection: Medium-Duty vs. Heavy-Duty Racking Architectures
In modern industrial intralogistics, specifying racking systems requires strict structural differentiation between medium-duty shelving and heavy-duty pallet networks. Selecting under-engineered upright profiles leads to beam deflection and localized buckle under cyclical forklift impacts, while over-engineering wastes CapEx.
As verified by our 300+ engineering staff at Guangzhou Heda Shelves Co., Ltd., medium-duty systems (typically defined as holding 200 kg to 800 kg per shelf tier uniformly distributed load [UDL]) utilize cold-rolled C-channel or stepped-beam profiles with butterfly or teardrop hole pitches. Heavy-duty pallet installations (exceeding 1,000 kg to 4,000 kg per level) mandate closed-box beams, multi-clamping connector teeth with safety locking pins, and baseplates anchored directly into dynamic C25/30 foundation slabs.
Structural Comparison & Procurement Parameter Matrix
| Technical Parameter | Medium-Duty Longspan Shelving | Heavy-Duty Selective Pallet Racking | High-Density Shuttle / Drive-In |
|---|---|---|---|
| Typical Load Limit | 200 – 800 kg / layer UDL | 1,000 – 4,500 kg / beam tier | 500 – 2,000 kg / pallet lane |
| Column Profile (mm) | 55×47×1.5 or 60×50×1.8 | 80×60×2.0 to 120×95×2.5 | 90×70×2.0 to 120×95×3.0 |
| Handling Methodology | Manual picking / AGV flat cart | Counterbalance, Reach truck, VNA | Semi-automated shuttle car / Drive-in truck |
| Surface Pre-Treatment | Electrostatic powder coat (60μm) | 9-Stage pickling & phosphating + Powder | Galvanized option for cold storage (-30°C) |
| Seismic Compliance | Basic floor expansion anchors | Seismic footplates (NCh 2369, NSR-10) | Engineered portal bracing & back ties |
Macro Trends Shaping Global Racking Procurement (2025–2030)
Global logistics executives face rising warehouse square-meter costs, stricter regional seismic zoning, and rapid automation retrofits. Purchasing decisions from Chinese tier-1 manufacturing hubs are transitioning from raw steel weight pricing to whole-lifecycle system compatibility.
1. Dynamic Structural Analysis
Buyers across South America's Pacific Rim and North America now require finite element analysis (FEA) calibrated to regional codes (e.g., Chilean NCh 433/2369, Colombian NSR-10, and US RMI specifications) rather than generic static capacity charts.
2. Automation-Ready Hybrid Tolerances
Manual longspan and pallet racks are increasingly engineered with tighter millimeter tolerances (±1.0mm) to allow drop-in deployment of Autonomous Mobile Robots (AMRs) and automated radio shuttles without replacing structural uprights.
3. Corrosion-Resistant Chemistry
With massive cold-chain expansion across Latin America and Southeast Asia, procurement has pivoted away from cheap air-dry paints toward certified eco-friendly thermosetting powders cured at 180°C–200°C, and sendzimir galvanized zinc coatings resistant to acid condensation.
Guangzhou HEDA Shelves: 25 Years of Direct-Factory Manufacturing Rigor
Headquartered in Guangzhou since 2001, Guangzhou Heda Shelves Co., Ltd. controls a modern 30,000 square meter production facility. Unlike trading intermediaries, we execute all critical manufacturing processes in-house across automated continuous production cells:
From automated CNC precision punching lines that stamp upright hole pitches with sub-millimeter repeatable accuracy, to multi-roll cold bending profiling mills, automated robotic MIG welding stations, and a closed-loop automated 9-stage pickling, phosphating, and electrostatic powder coating plant.
All fabricated batches undergo tensile yield checks, cross-hatch adhesion testing (DIN EN ISO 2409), and 100% component verification matching the issued structural engineering drawings before export dispatch.
Frequently Asked Questions by Industrial Racking Importers
Direct technical answers from our engineering desk to guide procurement diligence.
We supply comprehensive structural calculation sheets based on FEM 10.2.02 and EN 15512 standards, mill test certificates (MTC) verifying raw material chemical composition (Q235B/Q355B), and third-party CE certificate No. 2435-CPR-8605159 and ISO 9001:2015 audit reports.
Clients provide site coordinates, soil class, and peak ground acceleration values. Our design team adjusts column thickness, expands baseplate footprints, specifies seismic anchor bolts (Hilti/Fischer equivalent embedment), and models vertical X-bracing to prevent dynamic resonant collapse.
Backed by our 30,000-ton monthly capacity, standard medium-duty and selective racking runs of 1 to 5 full container loads (40HQ) are completed within 14 to 21 business days following CAD drawing sign-off and color code confirmation.
For ambient warehouses, our multi-stage electrostatic powder coating provides durable resistance. For cold-storage applications below -20°C or high-salinity coastal ports, we supply pre-galvanized components or hot-dip galvanizing per ASTM A123 to permanently prevent rust creep.