Precision-Engineered Industrial Pallet Racking Portfolio
Heavy-duty OEM configurations manufactured to exact architectural and payload tolerances. Built for modern fast-throughput distribution centers, cold-storage logistics, and high-density industrial staging hubs.
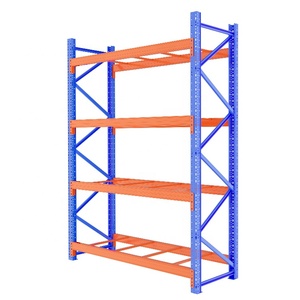
4 Layers 1000kg OEM Heavy Duty Industrial Warehouse Racking Shelves for Warehouse Storage Racking System
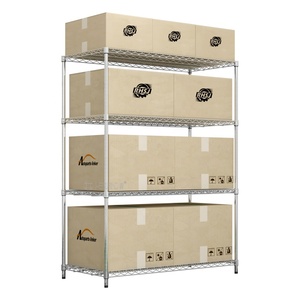
Versatility 4 Tiers NSF Approval Chrome Plated Racking Solid Steel Wire Shelving Storage System for Garage Warehouse
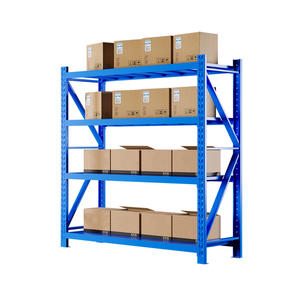
Industrial Warehouse Storage 5-Layer Pallet Racking System with Tire Rack Slotted Angle Rack Stacking Racks & Shelves
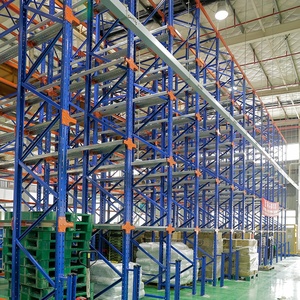
Shibang Heavy Duty Drive-In Pallet Rack System Warehouse with LIFO Storage High-Capacity Adjustable Drive-Thru Shelving
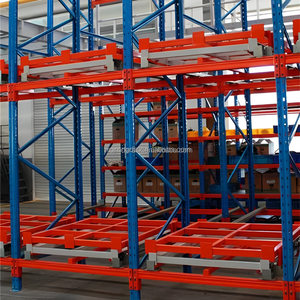
Warehouse Storage Adjustable Push Back Pallet Racking Manufacturer Steel Rack
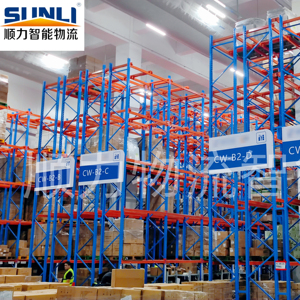
ShunLi Adjustable Steel Powder Coated High-Density Storage Warehouse Rack Double Deep Selective Pallet Racking Shelf Beam Racks
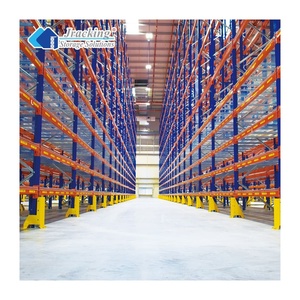
Jracking Euro Standard Steel Vertical Warehouse Storage Racks Heavy Duty Selective Pallet Racking System
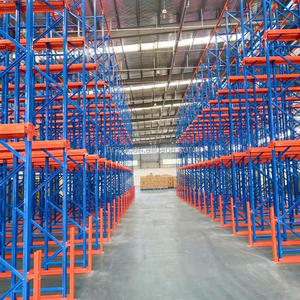
Wholesale Price Industrial Storage Shelf Drive-In Rack Steel Stacking Pallet Racking Vendors For Chemical Industry Warehousing
Technological Evolution: The Shift from Static Racks to Automated Intralogistics
Warehousing infrastructure has transitioned from passive structural framing into active, cyber-physical fulfillment cores. Engineering teams must evaluate load paths, steel plasticity, and automation interfaces.
1. High-Tensile Cold-Rolled Metallurgy
Traditional hot-rolled structural shapes are giving way to advanced cold-formed micro-alloy steels (Q355B and high-yield Grade 50). Continuous roll-forming lines integrate online CNC hydraulic punching, ensuring hole-pitch tolerances within ±0.1mm. This structural optimization reduces rack self-weight by up to 18% while enhancing torsional resistance under seismic loads.
2. ASRS & Radio Shuttle Integration
High real estate costs have made selective single-deep layouts non-viable for mega-fulfillment centers. Modern facilities require hybrid push-back and 4-way radio shuttle channels. Structural beams now feature integrated sensor conduits, anti-jump guides, and ultra-precise docking flanges to seamlessly house automated guided vehicles (AGVs) and autonomous mobile robots (AMRs).
3. Seismic Performance Modeling (FEA)
Seismic engineering no longer relies on static tables. Finite Element Analysis (FEA) models non-linear beam-to-column connector stiffness, base-plate anchor elongation, and frame second-order P-Delta phenomena. Installations in active zones (such as Chile, Peru, and the American Pacific rim) utilize thickened footplates, oversized chemical wedge anchors, and energy-dissipating dynamic bracing.
| Storage Topology | Space Utilization | SKU Selectivity | Cycle Speed | Seismic Resilience | Optimal Industry Application |
|---|---|---|---|---|---|
| Standard Selective Pallet | 40% - 45% | 100% Direct Access | Rapid / Immediate | High Flexibility | FMCG, 3PL Distribution, Multi-SKU Retail |
| Double-Deep Reach Rack | 55% - 65% | 50% (Pantograph reach) | Moderate | Good Base Stability | Dry Goods, Pharmaceuticals, Paper Production |
| Drive-In / Drive-Through | 70% - 80% | Low (LIFO / FIFO Lanes) | Controlled Forklift Run | Requires Rigid Top-Bracing | Cold Storage, Beverage Bottling, Raw Commodities |
| Dynamic Push-Back (Cart) | 65% - 75% | Medium (1 SKU per lane) | High Operator Speed | Self-Contained Rail Forces | Frozen Food Staging, Automotive Parts Assembly |
| Semi-Automated Radio Shuttle | 80% - 90% | Programmable Batching | Automated Carrier Rapid | Engineered Box Structure | High-Throughput Agro-Export, Meat Processing |
Future Global Sourcing & Procurement Directives
Key sourcing trends transforming how warehouse directors, structural engineers, and supply chain managers specify heavy industrial steel storage systems.
Direct-From-Mill Traceability
Tier-1 logistics buyers no longer accept unverified steel origins. Modern procurement documents demand full Mill Test Certificates (MTC EN 10204 3.1) tracing hot-rolled coils back to primary blast furnaces. This ensures guaranteed chemical limits on carbon, silicon, and sulfur to avoid brittle failure in freezing environments.
BIM & Digital Twin Handover
OEM procurement now requires full BIM (Building Information Modeling) Level 2 deliverables. Supplier engineering divisions supply parametric Revit and IFC models detailing structural deflections, floor anchor point coordinates, and sprinkler pass-through paths, integrating directly into enterprise WMS platforms.
Total Landed-Cost (TLC) Packaging
Ocean freight economics dictate component design. High-capacity suppliers engineer teardrop, slot, and beam profiles that nest compactly inside 40ft High Cube containers. Optimized bundle designs achieve a 95%+ shipping volume utilization without damaging powder-coated or galvanized surface finishes.
Why Global Importers Partner with Our Manufacturing Base
With over 25 years of specialized manufacturing experience, our 30,000 m² automated facility engineers, fabricates, tests, and exports high-performance racking across the Americas, Europe, and Asia.
In-House Tooling & Rolling
We operate 16 continuous automatic cold roll-forming lines, high-speed automated hydraulic punch presses, and robotic welding cells that ensure tight beam-to-connector locking tolerances.
Seismic Design Expertise
Our dedicated structural engineering team calculates seismic anchorages tailored to local geological codes (such as Chile NCh 2369, Peru E.030, and Colombia NSR-10), delivering turnkey stamped FEA reports.
Advanced Surface Finishing
Our 9-stage pre-treatment line includes automatic acid pickling, zinc phosphating, and electrostatic epoxy-polyester powder coating, backed by rigorous 500-hour ASTM B117 salt spray corrosion testing.
Certified International Quality
Every fabrication batch conforms to CE (EN 15512), ISO 9001:2015, and RoHS standards. Raw coil steel sheets undergo tensile, yield, and elongation verification before entering the profiling line.
The 10-Stage Controlled Quality Production Cycle
Complete vertical integration ensures that material chemistry, profile geometry, weld integrity, and coating adhesion are verified before container loading.
01. Raw Coil Assay
Q235B/Q355B mill coil inspection for yield strength, tensile limits, and thickness tolerance.
02. Precision Slitting
High-speed longitudinal slitting lines cutting coil stock into exact upright and beam blanks.
03. CNC Punching
Automated multi-station punch presses stamping diamond, teardrop, or Euro pitch slots at ±0.1mm accuracy.
04. Roll-Forming
Continuous cold roll-forming with up to 24 roller passes creating stiff omega upright profiles.
05. Box Beam Seaming
Twin C-channel interlocking with high-frequency continuous automated seam-welding.
06. Robotic Welding
Automated 6-axis robotic arms welding multi-claw end connectors onto beam ends with deep gas-shielded penetration.
07. Pickling & Phosphating
Chemical immersion bath degreasing and phosphating to eliminate surface oxidation and maximize resin bonding.
08. Electrostatic Coating
Automated powder spray booths applying 60-80 micron thick lead-free thermoset epoxy-polyester powder.
Frequently Asked Technical & Sourcing Questions
Critical insights for project engineers, procurement directors, and warehouse operations executives.
What essential architectural and operational parameters are required for a customized layout and load calculation?
How are structural seismic forces engineered into upright frames and baseplates for high-risk zones?
What surface treatment systems are utilized to prevent oxidation in high-humidity or cold-chain environments?
How does your factory protect components during export packing to guarantee damage-free overseas transit?
What are typical production lead times, and can large projects be delivered in phased batches?
Accelerate Your Storage Efficiency with Custom OEM Engineering
Send your warehouse floor plan, pallet specs, and storage criteria. Our structural engineers will deliver a free 3D layout, CAD proposal, and factory-direct quotation within 24 hours.
Contact Us