High-Density Double Deep Pallet Racking Architecture
A rigorous engineering and procurement reference for supply chain architects, distribution center operations managers, and warehouse racking importers seeking optimal footprint utilization and engineered structural integrity.
 VNA System
High Density Narrow Aisle Pallet Racking Adjustable Beam Steel Storage System Powder Coated for Warehouses
- Upright Pitch: 50mm / 75mm Adjustable
- Load Range: 1,000kg - 4,500kg / beam level
- Finish: Electrostatic Epoxy-Polyester
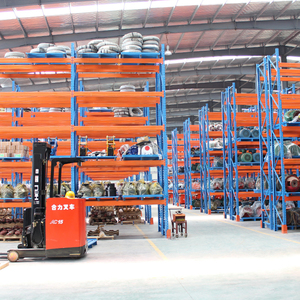 Drive-In Matrix
Best Selling Customized Warehouse Drive in Rack Steel Pallet Racking System Heavy Duty Industrial Warehouse Steel Rack
- Utilization: Up to 85% volumetric ratio
- Pallet Guide Rails: Formed galvanised steel
- Structural Code: FEM 10.2.02 standard
 Multi-Layer Rack
Durable Cold Rolled Steel Heavy Duty Multi-Layer Pallet Rack Warehouse Storage Solution High Loading Capacity Epoxy Racking
- Steel Grade: Q235B / Q355B cold rolled
- Safety Factor: 1.5 - 1.8 static design
- Column Sections: 90mm, 100mm, 120mm
 Logistics Beam
Adjustable Warehouse Storage Rack System Heavy Duty Pallet Rack Steel Shelf Steel Storage Rack for Logistics Storage
- Connector: 3, 4, 5-claw high rigidity
- Beam Profile: Box beam / Step beam
- Safety Locking Pins: High shear grade
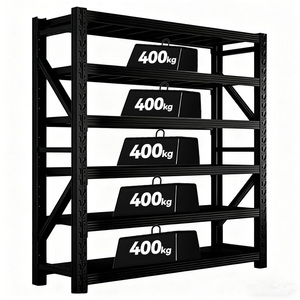 Multi-Tier Light/Heavy
5/6 Layer Heavy Light Duty Steel Warehouse Rack Adjustable Industrial Shop Storage 400kg Garage Metal Workshop Shelf
- Shelf Capacity: 200kg - 800kg UDL
- Decking: Steel plate / wire mesh / plywood
- Assembly: Boltless interlocking system
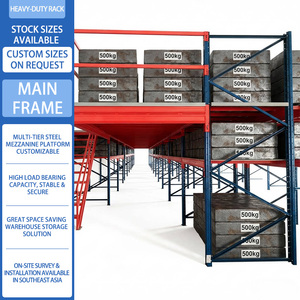 Industrial Pallet Rack
China Manufacturer Heavy Duty Cold Rolled Steel Pallet Rack System 300kg/sqm Load Capacity Boltless/Beam Type Industrial Storage
- Framing: Heavy cold roll profile Omega
- Bay Clear Span: Up to 3,900mm
- Pre-treatment: Zinc phosphating bath
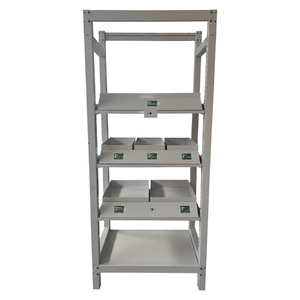 IoT Smart Sensing
Smart Modern Multi-Function Weighing Shelf System Gravity Sensor Medical Consumables Storage Rack for Hospital
- Weight Accuracy: ±1-5g sensor threshold
- Cloud API: WMS / ERP real-time syncing
- Integration: Cleanroom hospital pharma
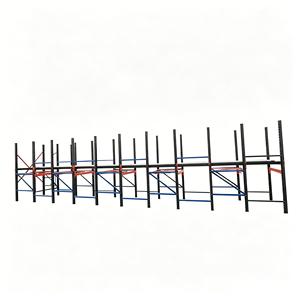 Drive-Through
Custom Heavy Duty Drive-In Storage Rack, High Strength High Load Through Type Warehouse Pallet Racking
- Depth Capacity: 2 to 10 pallets deep
- Arm Cantilever: One-piece stamped steel
- Rotation Mode: FILO & FIFO options
Engineering Principles of Double Deep Pallet Racking Systems
A double deep racking configuration positions two pallet loads in back-to-back pairs, cutting floor aisle counts in half relative to conventional selective pallet racking. This setup unlocks superior volumetric storage density while maintaining 50% immediate pallet selectivity.
Upright Frame Mechanics & Torsional Rigidity
Double deep configurations impose compound eccentric shear stresses and lateral moment forces onto upright frames during retrieval of rear-position pallets. To counteract horizontal torsional loads, Guangzhou Heda Shelves utilizes proprietary cold-rolled Omega (Ω) profile columns engineered with 8 to 12 cold-bent flanged returns.
Fabricated exclusively from premium structural carbon steel grade Q355B (Yield Strength fy ≥ 355 MPa) or Q235B (fy ≥ 235 MPa), each frame integrates continuous welded tubular horizontal and diagonal cross-bracing in K-truss or Warren truss configurations. This eliminates buckling modes across unsupported column heights exceeding 12 meters.
Baseplates are engineered with dynamic anchor bolt patterns designed to resist floor shearing forces generated under intense pantograph reach cycles, fully conforming with European Standard EN 15512:2020 and American RMI (Rack Manufacturers Institute) MH16.1 design codes.
Beam Load Deflection & Connection Moment
Beam deflection under maximum design loading (UDL) represents the core structural safety metric. While general industry thresholds allow deflections up to L/200, Guangzhou Heda Shelves engineers double deep load beams to a stiffer criterion of L/250 to L/300 to ensure operational clearances during rear-slot reach pantograph retraction.
Beams are continuously roll-formed as interlocking twin-C box profiles or custom step profiles seam-welded by automated robotic lines. Each beam connector is fabricated with 4 to 5 precision cold-stamped claws that wrap securely around the column face.
Coupled with spring-loaded safety locking pins resistant to vertical dislodgment forces greater than 1,000 kg, the connection provides high moment-rotation stiffness, preserving the global stability of multi-tier installations without requiring extensive overhead portal ties.
| Storage System Type | Floor Space Utilization | Pallet Selectivity | Material Handling Equipment | Aisle Width (AST) | Relative CAPEX / Pallet |
|---|---|---|---|---|---|
| Standard Selective Racking | 40% - 45% | 100% (Direct Instant Access) | Standard Counterbalance / Reach Truck | 3,200mm - 3,800mm | Baseline (1.0x) |
| Double Deep Pallet Racking | 60% - 65% | 50% (2 Pallets Deep per Bay) | Pantograph Reach Truck / Telescopic Mast | 3,000mm - 3,400mm | Optimal Balance (1.15x) |
| Drive-In / Drive-Through | 75% - 85% | 15% - 20% (LIFO / Strict Batch) | Counterbalance / Spec Drive-in Reach | Continuous Lane | 1.35x - 1.50x |
| Very Narrow Aisle (VNA) | 55% - 60% | 100% (Direct Immediate Access) | Articulated Truck / Guided Turret Truck | 1,600mm - 1,900mm | 1.60x - 2.20x |
| Automated Radio Shuttle | 80% - 90% | 20% - 40% (FIFO / LIFO Automated) | Standard Forklift + Radio Carrier Shuttles | 3,000mm - 3,200mm | 2.40x - 3.20x |
Guangzhou Heda Shelves Co., Ltd.: Integrated Manufacturing Workflow
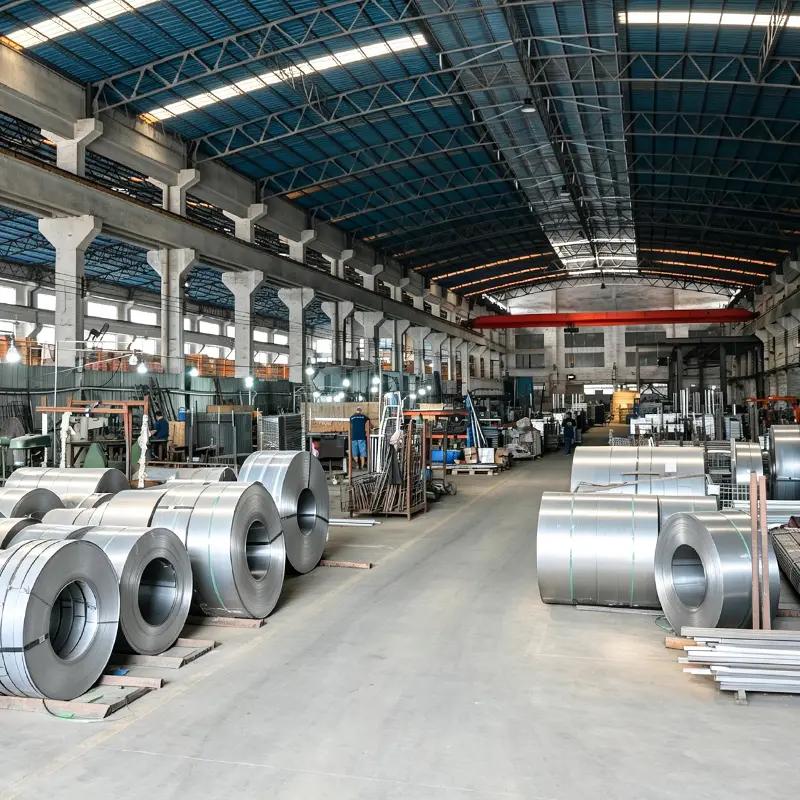
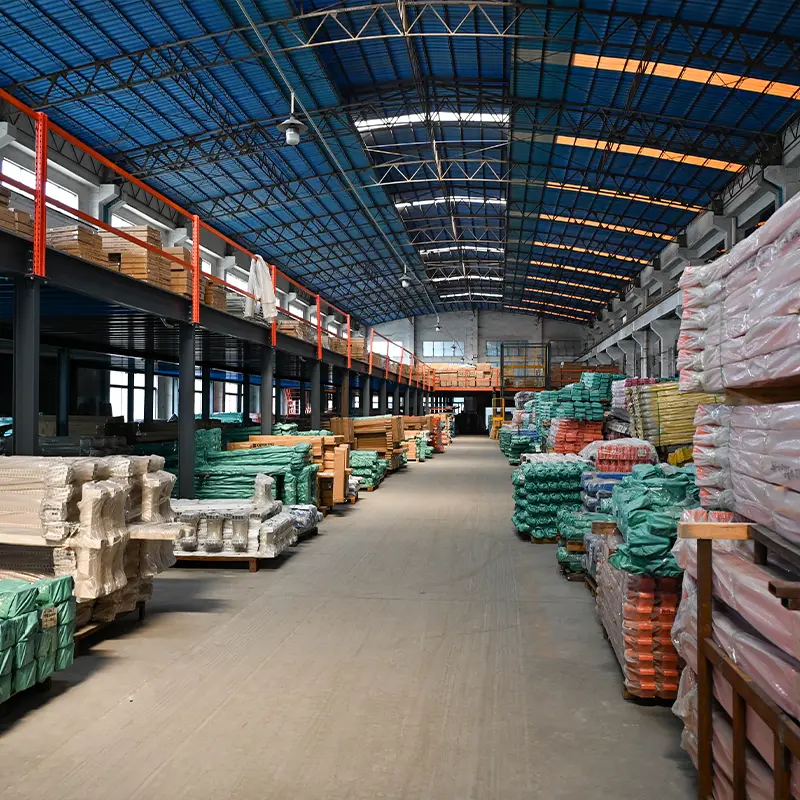
Operating a state-of-the-art 30,000 m² heavy-steel fabrication center staffed by over 300 experienced engineers and technical roll-forming specialists, our monthly production capacity reaches 30,000 metric tons. Our 10-step quality-controlled production chain guarantees structural integrity from coil slitting to overseas maritime crating.
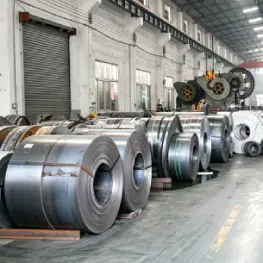 Step 01
Raw Steel Assay
Spectrometric tensile and metallurgical chemical verification of incoming prime hot and cold-rolled steel coils.
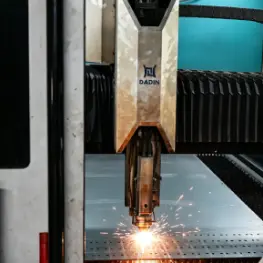 Step 02
CNC Slitting
Automated uncoiling and high-speed CNC shear slitting calibrated to tight dimensional tolerances (±0.2mm).
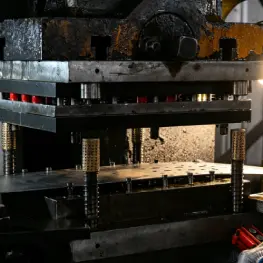 Step 03
Progressive Punching
Multi-ton mechanical presses execute automated pitch hole patterns (50mm/75mm) for structural drop-in connectors.
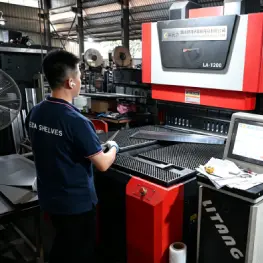 Step 04
Roll-Forming
24-stage continuous cold roll-forming lines shape multi-angle Omega uprights without micro-fracturing cross-sections.
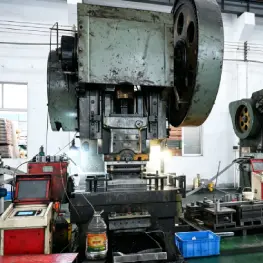 Step 05
Beam Profiling
Continuous twin-C interlock profiling creates rigid tubular box beams with uniform wall thicknesses.
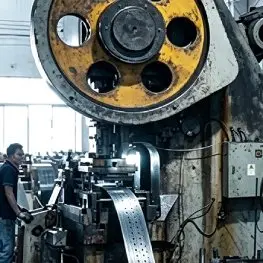 Step 06
Edge Deburring
Mechanical rotary wire-brush deburring and precision grinding ensure clean edges and personnel safety.
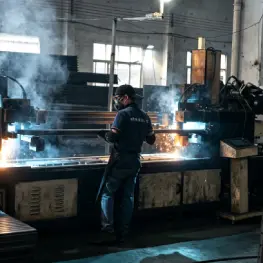 Step 07
Robotic Welding
Panasonic multi-axis robotic CO2 gas shielded welding ensures deep penetration connector joining.
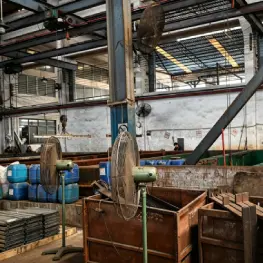 Step 08
Surface Pretreatment
9-stage chemical wash line: acid pickling, ultrasonic degreasing, and dense zinc-phosphating micro-coating.
 Step 09
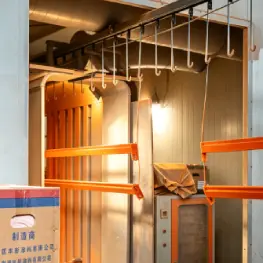
Powder Coating
Automated GEMA electrostatic powder application cured at 200°C produces a durable 60-90μm corrosion-resistant finish.
 Step 10
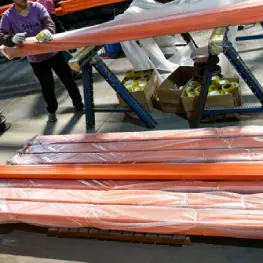
QC & Ocean Bundling
100% batch tolerance verification, thickness checks, drop tests, and nested steel bundling for container stuffing.
Over 2 Decades of Engineering Excellence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has evolved from a specialized tooling workshop into a global industrial racking designer and exporter. We have successfully delivered more than 10,000 turn-key warehouse projects across 120+ nations worldwide.
Our deep bench of structural engineers evaluates every project against localized geotechnical parameters, operating temperatures, and inventory rotation methodologies.
Complimentary 3D CAD & Structural FEA
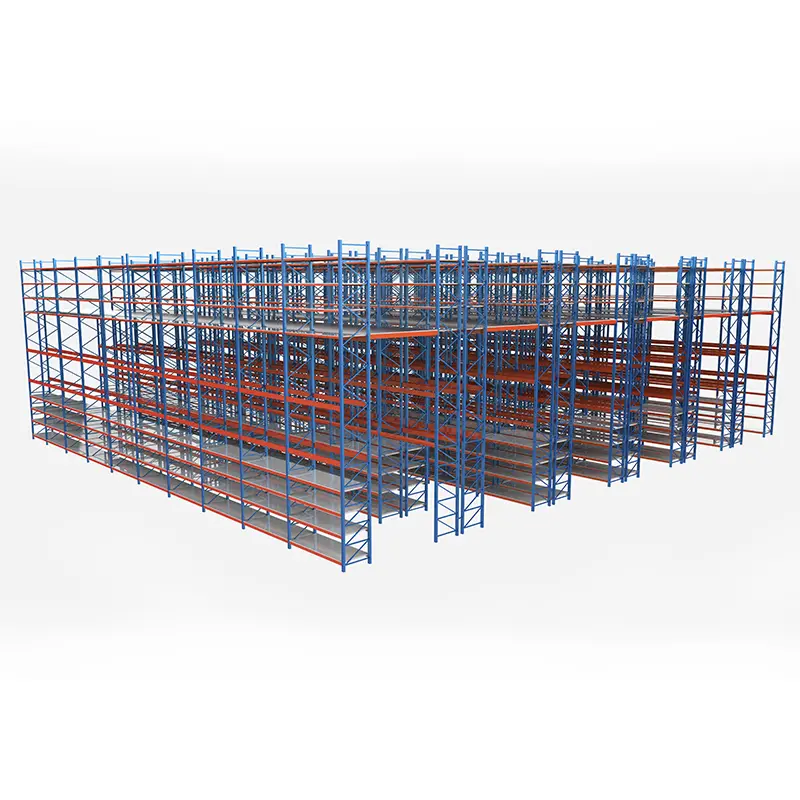
We provide complimentary warehouse spatial design, AutoCAD bay layouts, and detailed 3D digital renderings for all qualified procurement inquiries. Our engineering department conducts comprehensive Finite Element Analysis (FEA) to confirm stability margins.
From slab capacity analysis to forklift turning radiuses, our layouts eliminate installation surprises and maximize available vertical cubic storage space.
CE Certified & ISO 9001:2015 Audited
Quality assurance is backed by accredited international certifications, including CE Certificate (Factory Production Control No. 2435-CPR-8605159) and ISO 9001:2015 Quality Management System Certification (No. 18624Q00169R0M).
All finished powder coatings comply with RoHS directives, ensuring environmentally sound, heavy-duty abrasion resistance across food, cold storage, and chemical industries.
Future Sourcing & Technological Trends in Industrial Racking
Industrial warehousing is undergoing significant structural shifts driven by automated logistics integration, stricter seismic building codes, and decarbonization mandates. B2B procurement leaders should incorporate these forward-looking engineering criteria into their racking RFQs.
Autonomous Reach Truck & AGV Integration
Warehouses are increasingly pairing double deep racking with automated guided vehicles (AGVs) and vision-guided automated reach trucks. This requires tighter beam deflection tolerances (L/300) and laser-guided slot positioning to prevent handling collisions in second-pallet-deep pockets.
Regional Seismic Code Upgrades
Global procurement teams are prioritizing supplier-engineered seismic compliance. Structural designs must adapt to Pacific Rim and Andean seismic regimes (such as Chile NCh 2369, Peru E.030, Colombia NSR-10, and US IBC/ASCE-7), requiring reinforced baseplate anchors and dynamic diagonal bracing.
Cold Chain & Controlled Atmosphere
Surging global cold chain volumes for perishables and biologics are driving adoption of double deep configurations to minimize refrigerated cubic volume. Advanced pre-treatment and low-temperature-cured powder coatings are required to resist embrittlement and corrosion at -30°C.
ESG Compliance & Green Steel
Enterprise procurement now tracks Scope 3 embedded carbon emissions in warehouse infrastructure. Heda Shelves utilizes resource-efficient continuous roll-forming lines and recyclable low-VOC powder coatings to support green building standards like LEED and BREEAM.
Export Packaging, Safe Ocean Stowage & Port Logistics
Exporting structural steel racking across deep-sea container routes demands meticulous packaging engineering. Guangzhou Heda Shelves maximizes 40ft High Cube (40HQ) container utilization up to 26 metric tons while safeguarding powder-coated surfaces against transoceanic transit vibration and sea-spray humidity.
Engineered Load Planning & Interlocking Bundles
Uprights are nested back-to-front and securely strapped with high-tensile steel banding onto hardwood skids. Heavy corrugated paper edge protectors and non-abrasive expanded polyethylene (EPE) foam cushioning eliminate metal-to-metal rubbing that could compromise corrosion-inhibiting powder coats.
Every sea container is optimized through 3D container packing software, arranging beam bundles by length to balance container center of gravity and ensure easy, damage-free unloading via counterbalance forklifts at the destination terminal.
Global Shipping Corridors & Full Documentation
We handle export operations out of major South China ports (Guangzhou / Nansha / Shenzhen), delivering to principal container hubs globally: Santos, Callao, San Antonio, Valparaíso, Buenaventura, Rotterdam, Hamburg, Los Angeles, and Jebel Ali.
Each container shipment includes bilingual assembly manuals, marked piece-tag manifests, mill test certificates (MTC), certified loading diagrams, and structural warranty dossiers to simplify customs clearance and site assembly.
Frequently Asked Questions on Double Deep Pallet Racking
Detailed engineering, logistical, and operational answers for supply chain directors and procurement managers.
What specialized forklift equipment is required for double deep racking?
Double deep racking requires reach trucks fitted with pantograph scissor extensions or double-reach telescopic forks capable of picking the rear pallet position. Operators benefit from mast-mounted wireless cameras and laser height indicators to ensure accurate second-deep pallet positioning at elevations above 6 meters.
How does inventory rotation function in a double deep layout?
Double deep operates on a Last-In, First-Out (LIFO) basis per individual storage lane, because the outer pallet must be retrieved before accessing the rear unit load. However, when managed via Warehouse Management Systems (WMS) tracking twin-pallet SKU pairs, overall operations achieve efficient First-Expired, First-Out (FEFO) and high inventory turnover.
Can you provide custom engineering calculations for high-risk seismic zones?
Yes. Our engineering department incorporates local site coordinates, ground acceleration coefficients, and soil spectral classifications. We calculate baseplate anchors, column gauge thicknesses, and cross-bay portal ties to ensure compliance with relevant seismic codes such as Chile NCh 2369, Peru E.030, Colombia NSR-10, and US RMI MH16.1.
What is the standard production lead time for full-container export orders?
Standard production lead time for orders between 1 to 5 full 40HQ containers is 15 to 25 business days following formal approval of fabrication shop drawings. For multi-thousand pallet high-bay distribution centers, production runs are scheduled in coordinated maritime batches aligned with your site construction schedule.
How are damaged components repaired or replaced over time?
We archive every project's detailed engineering drawings, punch tooling geometries, and color codes indefinitely. If a forklift impacts an upright or beam, replacement components matching original roll-formed cross sections, connection teeth, and powder hues can be fabricated and shipped quickly, alongside heavy-duty wrap-around post protectors.
What critical dimensional data is required to generate a custom 3D layout?
To deliver an optimized CAD layout and structural load assessment, our engineers need: (1) warehouse boundary drawings with column grids, clear eave height, and dock locations; (2) pallet dimensions (width, depth, overall height including cargo overhang); (3) maximum pallet weights; (4) forklift make, model, and reach height; and (5) operating environment temperatures.
Ready to Maximize Your Warehouse Cubic Efficiency?
Connect directly with our senior structural engineering team. We deliver comprehensive AutoCAD bay layouts, Finite Element Analysis (FEA) load reports, and transparent factory-direct pricing within 24 to 48 hours.
- Free 3D CAD Warehouse Space Layout
- Certified Structural Load Capacity Reports
- ISO 9001:2015 & CE Quality Guaranteed
- Direct Manufacturer Pricing (Save 20-30%)
Request Engineering Consultation
Speak with our factory engineers about custom specifications, load ratings, or container freight planning.
Get a Quote