Architecting Vertical Density: The OEM/ODM Multi-Tier Advantage
Modern supply chains face unprecedented spatial constraints, surging industrial land values, and escalating logistical overhead. Standard single-tier warehousing layouts waste up to 60% of clear vertical cube volume. As an industry-leading OEM/ODM multi tier pallet racking manufacturer and certified structural factory, Guangzhou Heda Shelves Co., Ltd. re-engineers intra-facility logistics through bespoke multi-level mezzanines, automated shuttle channels, and seismic-certified high-load structural frameworks designed to maximize vertical volume without increasing physical ground footprints.
Featured Multi-Tier Pallet Racking & Mezzanine Platforms
Explore 8 precision-engineered storage architectures fabricated using premium Q235B/Q355B cold-rolled steel, high-durability electrostatic polymer powders, and automated continuous-roll forming technology.
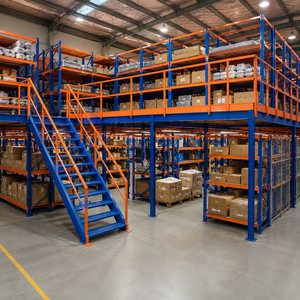
Heavy Duty Pallet Rack Supported Mezzanine Platform
Integrated structural platform utilizing heavy-duty upright frames as primary load columns. Supports overhead open flooring for picking, packing, or light manufacturing while retaining heavy bulk pallet storage underneath.
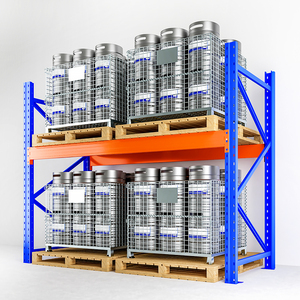
Industrial Heavy Duty Pallet Storage Rack Units (5000KG)
Certified structural pallet shelving engineered for ultra-heavy bulk loads. Features 7-bend Omega upright posts, reinforced safety locking pins, and custom step beams built to withstand high-impact forklift loading.
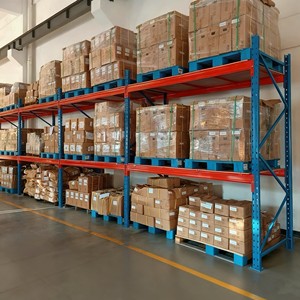
Heavy Duty Boltless Multi-Tier Metal Shelving System
Rapid-assembly modular boltless design with precision rivet-and-keyhole interlocking slots. Optimized for multi-tier e-commerce fulfillment hubs requiring agile, tool-free vertical tier adjustments.
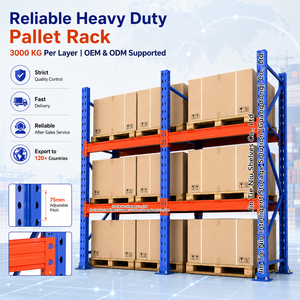
Corrosion-Protected Multi-Level Pallet Racking (3000KG)
Multi-tier high-bay pallet racking featuring an advanced 4-stage pretreatment process: acid pickling, phosphating, electrostatic epoxy-polyester coating, and thermal curing for severe humidity and coastal environments.
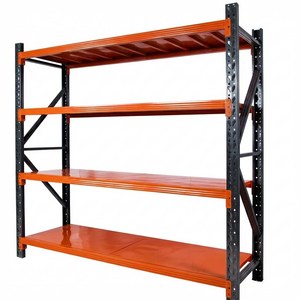
Multi-Layer Cold Rolled Steel Pallet Racking Solution
High-tensile cold-rolled steel profiles engineered for structural stability across tall vertical elevations. Equipped with dynamic cross-bracing and oversized seismic footplates for maximum structural integrity.
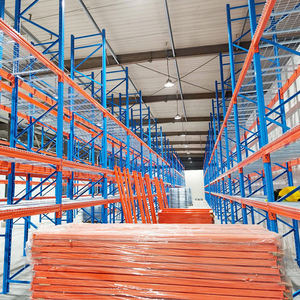
Multi-Level Steel Mezzanine Attic Storage Platform
Engineered mezzanine attic structures designed to convert unused overhead air rights into functional second- and third-story staging floors. Fully fitted with industrial staircases, perimeter handrails, and safety swing gates.
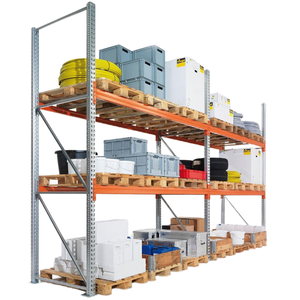
Adjustable Selective Multi-Layer Workshop Pallet Racks
The gold standard in warehouse versatility, delivering 100% direct accessibility to every pallet location. Accommodates varied pallet geometries, wire decking panels, pallet support bars, and drop-in steel dividers.
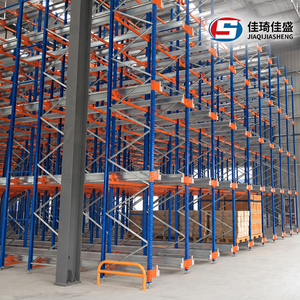
Multi-Level Two-Way Radio Shuttle High-Density Racking
Semi-automated deep-lane pallet shuttle system. Self-powered robotic shuttles transport pallets within dedicated running rails, eliminating forklift entry into internal storage channels to dramatically improve safety and cycles.
Why Global Procurement Officers & Engineering Contractors Partner with HEDA
Procuring structural warehouse infrastructure requires verifiable manufacturing excellence, audited quality control, and rigorous engineering design. HEDA Shelves integrates complete vertical supply manufacturing from raw steel coil slitters to on-site commissioning.
Full In-House Manufacturing Control
With 30,000 m² of automated workshops, we handle raw steel slitting, precision CNC multi-station column punch pressing, automated 18-stage cold roll forming, robotic welding, and automated continuous powder coating without third-party outsourcing.
Bespoke OEM/ODM Engineering
We support industrial distributors, logistics developers, and corporate facility operators with tailor-made OEM branding, custom pitch punchings (50mm, 75mm, 76.2mm teardrop), specialized steel alloy selections, and proprietary architectural integrations.
Accredited International Quality
Fully certified under CE (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 standards. Every production heat undergoes destructive tensile testing, weld ultrasonic checks, coating thickness analysis, and deflection tolerance benchmarking.
Complimentary 3D Layout & Static Calculations
Our dedicated engineering team of over 30 structural specialists produces complimentary CAD architectural layouts, warehouse throughput flow charts, and finite element analysis (FEA) structural stress reports within 24 hours of requirement submission.
Rigorous Seismic Zone Adaptations
Extensive project engineering across the Pacific Rim and Andean seismic belts. Systems are custom-calculated to resist dynamic lateral and torsional forces according to regional codes including Chile NCh 2369, Peru E.030, Colombia NSR-10, and Eurocode EN 15512.
Optimized Export Logistics & Packing
Direct multimodal shipments to primary international ports across the Americas, Europe, Middle East, and Southeast Asia. We employ custom bundle crating, protective scratch-resistant wrapping, and 3D container load plans to minimize shipping damage and maximize cube efficiency.
Future Procurement Trends in Multi-Tier Racking (2025–2030)
Procurement methodologies for high-density warehouse storage are shifting from basic commodity pricing toward total lifecycle cost evaluation, structural resilience, and automation readiness.
1. Hybridization of Mezzanine Platforms with Mobile Robotics (AMRs)
The rapid growth of multi-level pick towers has revealed human ergonomic limitations. The future of multi-tier storage relies on AMR-compatible decking. Floor spans are transitioning from standard wood particleboards to high-tolerance, textured, cold-rolled steel composite planks. These surfaces provide optimal electrostatic discharge (ESD) protection, high surface friction, and minimal deflection required for automated guided vehicles, robotic sorting arms, and robotic order-picking fleets operating seamlessly on elevated tiers.
2. Stringent Environmental Pretreatment & Zero-VOC Coatings
Industrial supply chains face strict ESG metrics and corporate decarbonization targets. Traditional solvent-based solvent painting is entirely obsolete. Procurement specifications now dictate heavy metal-free chemical bath pretreatments (zirconium-based or closed-loop phosphating) paired with 100% reclaimable, zero-VOC electrostatic polyester-epoxy powders. In cold chain food distribution and pharmaceutical validation environments, anti-microbial and non-off-gassing finishes are rapidly becoming mandatory tender criteria.
3. High-Tensile Micro-Alloy Steels for Weight-Optimized Seismic Design
Rather than relying simply on heavier steel gauges to achieve structural capacity, progressive manufacturers are engineering racking using advanced high-strength micro-alloy steels (e.g., Q355B and specialized cold-forming grades). By engineering complex multi-bend profile geometries—such as 7-bend and 9-bend Omega columns—engineers can lower total deadweight by 12% to 18% while simultaneously increasing torsional rigidity and yield strength. This substantially lowers seismic inertia loads, resulting in smaller baseplates and shallower concrete foundation footings.
4. Structural Health Monitoring & Smart Collision Telemetry
Future-ready high-bay multi-tier installations are incorporating IoT structural monitoring sensors. Compact, battery-free RFID and BLE shock sensors are embedded within perimeter upright protectors and critical portal beam connections. When a heavy reach truck or counterbalanced forklift impacts an upright, automated telemetry instantly sends alerts to the facility management system with the location and impact force, streamlining routine inspections and preventing catastrophic progressive collapses.
| System Architecture | Typical Clear Height | Load Capacity Range | Floor Space Utilization | Accessibility & Rotation | Best Application Scenarios |
|---|---|---|---|---|---|
| Rack-Supported Mezzanine | 5,000 – 12,000 mm | 300 – 1,000 kg/m² | 180% – 280% (Double/Triple) | 100% SKU Access / FIFO | E-commerce fulfillment, spare parts, apparel sorting |
| Heavy Duty Multi-Tier Selective | 3,000 – 14,000 mm | 1,000 – 5,000 kg/level | 40% – 55% Floor Footprint | 100% Direct Selective Access | High SKU variety, 3PL logistics, retail FMCG hubs |
| Two-Way Radio Shuttle High-Bay | 4,000 – 16,000 mm | 500 – 1,500 kg/pallet | 75% – 85% Deep Lane Footprint | Automated Batch FIFO or LIFO | Cold storage, food & beverage, raw material buffering |
| Heavy Cantilever Mezzanine | 4,000 – 9,000 mm | 500 – 3,000 kg/arm | 60% – 70% Cube Density | Direct Crane / Forklift Access | Steel pipes, timber, PVC conduit, architectural profiles |
Frequently Asked Technical & Purchasing Questions
Essential technical, compliance, and logistical clarifications for engineering consultants, project architects, and global procurement specialists.