High-Density Industrial Storage & Stackable Rack Assemblies
Engineered for third-party logistics (3PL), automotive assembly lines, cold chain preservation, and high-throughput distribution centers. Every component is produced from certified Q235B/Q355B structural steel.
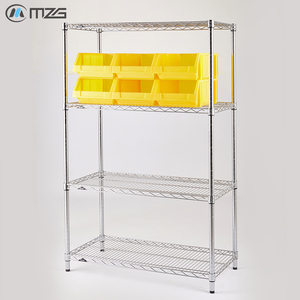
MZG Bulk Heavy Duty Warehouse Garage Industrial Chrome Multi-Layer Metal Wire Shelving with Storage Bin
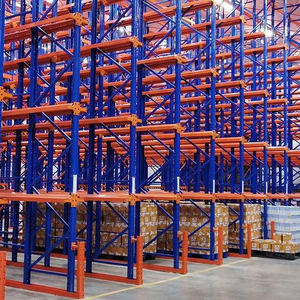
EBILMETAL 5 Steel Very Narrow Aisle Pallet Racking | OEM/ODM Adjustable Heavy Duty VNA Warehouse Racking
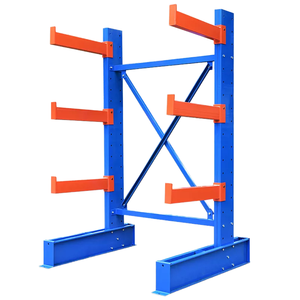
Double Cantilever Steel Storage Racking Shelving Unit Galvanized Electrostatic Powder Coating Plug-In Installation
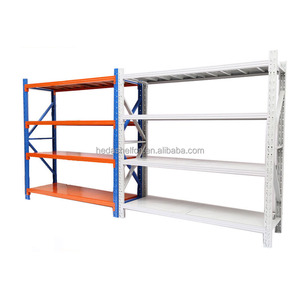
Wholesale Price Industrial Boltless Storage Rack 4 Tier Metal Shelving Units Warehouse Steel Stacking Racks
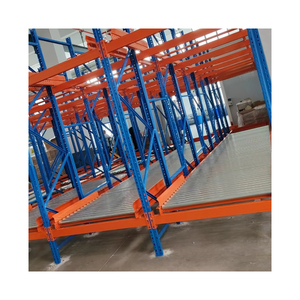
High Quality FIFO Gravity Carton Flow Rack Pallet Rack System Pallet Flow Racking Warehouse Equipment
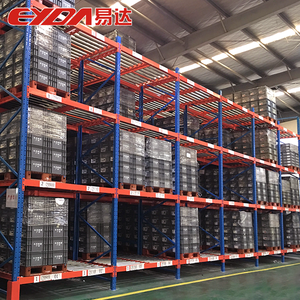
5 Layer Metal Pallet Flow Rack Gravity Storage Racks Heavy Duty Multi-Level Warehouse Industrial Cargo Storage
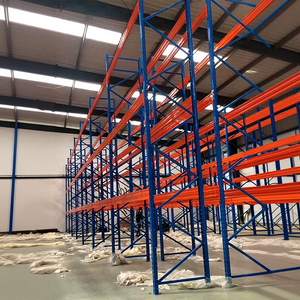
Heavy Duty Metal Racking 4 Tier Boltless Adjustable Warehouse Racking Steel Warehouse Storage Garage Storage
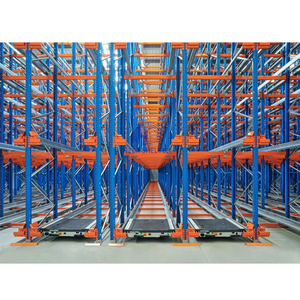
Warehouse High-Density Shuttle Rack System Asrs 4-Way Shuttle Racking for Cold Storage FIFO & LIFO
Structural Metallurgy, Deflection Thresholds & FEA Modeling
A rigorous examination of section modulus design, cold-form post buckling behavior, and dynamic load mitigation across modern stackable racking systems.
Material Selection: Q235B vs. Q355B Hot-Rolled Coils
The foundation of structural warehouse rack integrity resides in base coil chemistry. While budget suppliers utilize commercial-grade Q195 strip steels, premium OEM manufacturing mandates continuous-cast Q235B or micro-alloyed Q355B with verified yield strengths (σy ≥ 355 MPa).
- Controlled carbon equivalent (CEV ≤ 0.38) ensuring crack-free robotic MIG weldments.
- Charpy V-notch impact toughness certified to withstand -30°C embrittlement in blast freezers.
- Stringent cross-sectional gauge tolerances (±0.05mm) maintaining roll-form seam uniformity.
Section Modulus & Post Buckling Stability
Modern upright frames undergo complex multiaxial stress when loaded to maximum height. We deploy proprietary omega-shaped and teardrop upright sections engineered with 11-13 cold-formed bend radiuses to shift principal stresses toward corner flanges.
- Euler column buckling calculations strictly conform to RMI MH16.1 and EN 15512 codes.
- Beam connector claws feature 3-to-5-prong drop-forged teeth with tapered wedge angles.
- Safety lock pins withstand upward displacement thrusts exceeding 10 kN to prevent accidental dislodgement.
Deflection Limits (L/200) & Seismic Dissipation
Under design loading conditions, horizontal beam deflection is rigorously constrained to a maximum of L/200 (where L is the clear span length). For automation-assisted systems (VNA and ASRS), deflection tolerances tighten to L/300 to avoid shuttle jamming.
- Dynamic finite element analysis (FEA) simulates peak ground acceleration (PGA) up to 0.45g.
- Heavy-duty anchor footplates with dual anchor holes dissipate seismic shear loads safely.
- Horizontal and diagonal bracing geometries prevent frame twisting under eccentric forklift loads.
| Racking Architecture | Cubic Space Efficiency | Selectivity Ratio | Max Load / Bay (kg) | Seismic Adaptability | Ideal Handling Equipment |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Direct Access | Up to 15,000 | High (Universal baseplate ties) | Standard Counterbalance, Reach Trucks |
| Very Narrow Aisle (VNA) | 70% – 85% | 100% Direct Access | Up to 18,000 | Critical (High-mast sway dampening) | Man-Up / Man-Down Turret Trucks |
| Dynamic Pallet Flow (FIFO) | 80% – 90% | Lane Dependent | Up to 24,000 | Medium (Requires rigid row spacers) | Standard Reach / Forklifts at entry/exit |
| Radio Shuttle System (4-Way) | 85% – 95% | Batch / SKU Channel | Custom Unlimited | Superior (Low center of gravity structure) | Automated Shuttles + High-Reach Trucks |
| Structural Cantilever | 55% – 70% | Direct Column Face | 1,000 – 3,000 / Arm | Engineered (Braced backbone columns) | Side Loaders, 4-Directional Forklifts |
Global Sourcing Trends & Strategic Supply Chain Evolution
How supply chain executives, logistics developers, and plant directors are recalibrating their warehouse capital expenditures (CapEx) in response to geopolitical realignments and warehouse real estate costs.
Total Landed Cost Optimization Over Initial FOB Unit Price
Global procurement teams have moved beyond evaluating raw FOB metric-ton pricing. Modern supplier selection evaluates Total Cost of Landed Ownership (TCLO), emphasizing packing cubic nesting to fit 24-26 metric tons into 40ft High Cube containers without freight-wasting dead air space.
Additionally, modular pre-welded connectors and standardized connector punchings reduce site erection hours by up to 35%, slashing costly mechanical installation team bills on site in destination markets like the Americas and Europe.
Regulatory Certification & Seismic Code Harmonization
Specifying warehouse racking in earthquake-prone belts—such as the South American Pacific Rim (Chile NCh 2369, Peru E.030, Colombia NSR-10) or US West Coast (IBC/Seismic Design Category D-F)—mandates documented structural validation. Importers avoid generic steel fabricators who lack localized calculation methodologies.
Enterprise buyers now insist on independent mill test certificates (MTC 3.1), CE Declaration of Performance (DoP), and fully verifiable structural analysis documentation stamped by certified structural engineers.
Hybrid Modular Systems: Combining Pallet Density with Mezzanines
With industrial land leasing premiums soaring globally, warehouse operators are moving away from single-tier static installations. The fastest growing CapEx segment is hybrid multi-tier rack-supported platforms.
By transforming ground floors into heavy pallet storage and utilizing upper cantilever or longspan mezzanine levels for high-SKU manual e-commerce picking, operations effectively double or triple operational floor space without expanding physical warehouse building envelopes.
10-Stage Precision Production & Quality Assurance
Guangzhou HEDA Shelves maintains complete vertically integrated control over every manufacturing milestone to eliminate steel micro-fissures and guarantee flawless coating adhesion.
Spectrometric Steel Verification
Spectrometric testing of hot-rolled coils to verify carbon, silicon, and manganese chemistries prior to processing.
CNC Slitting & Uncoiling
Continuous automated uncoiling and precision slit-edge trimming to eliminate raw material burrs and edge stress risers.
Automated Post Punching
High-speed mechanical stamping presses punching pitch holes (50mm/75mm) with optical tolerances under ±0.1mm.
Continuous Roll Forming
Multi-stand precision cold-bending mills forming complex omega upright and box-beam structural geometries.
Robotic MIG Welding
Multi-axis Panasonic robotic welding cells executing spatter-free, deep-penetration welds on beam claw connectors.
Surface Pickling & Degreasing
Multi-stage immersion cleaning in acid baths to completely strip scale, oil, and atmospheric rust before coating.
Zinc Phosphating Treatment
Nanotechnology zinc-phosphate bath generating a dense crystalline conversion barrier for maximum corrosion resistance.
Electrostatic Powder Spray
Automated Gema powder spray booths applying 60-80 μm thermoset polyester powder coating for tough abrasion defense.
Frequently Asked Questions on Warehouse Racks & Sourcing
Direct technical answers addressing structural calculation standards, ocean freight logistics, cold storage metallurgy, and custom OEM/ODM parameters.
What structural calculations are provided for regional seismic codes?
How do you calculate safe working loads (SWL) and deflection limits?
What steel grade is specified for sub-zero cold storage operations?
What is the standard production lead time for FCL ocean shipments?
How are components bundled and protected for trans-oceanic shipping?
What technical data is required to generate a custom 3D warehouse layout?
Request Your Engineered Warehouse Racking Layout & Quotation
Connect directly with our senior application engineers. Receive a comprehensive CAD floor layout, structural stress calculation summary, and containerized freight estimate within 24 business hours.