Engineered Heavy-Duty Industrial Storage & Pallet Racking Systems
Precision roll-formed from premium Q235B and Q355B structural steel, our industrial warehouse shelving systems provide seismic-tested durability, zero-loss vertical space optimization, and certified load-bearing performance for international distribution centers.
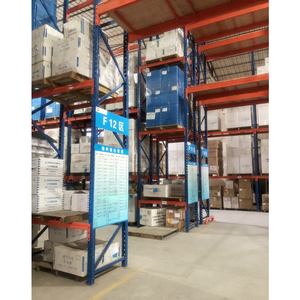
Custom Height Layer Beam Pallet Racking Rust Proof Surface Treatment Cargo Stacking Rack
- Capacity: Up to 5,000 kg / Beam Pair
- Steel: High-Tensile Q235B / Q355B
- Pitch: 50mm / 75mm Adjustable
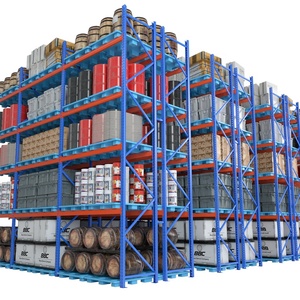
Pallet Multilevel Racking Heavy Duty Warehouse Storage Shelf System Stacking Rack
- Multi-Tier Vertical Density (Up to 12m)
- 100% Direct Selective Pallet Access
- Phosphate Wash + Electrostatic Powder
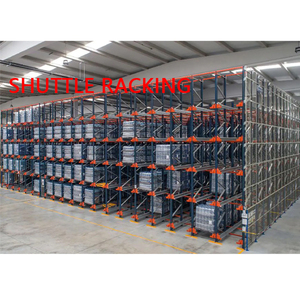
High-Density Radio Shuttle Racks System ASRS 4-Way Shuttle Racking Pallet Rack
- Space Utilization: Up to 85% Volumetric
- FIFO / LIFO Software-Controlled Logic
- Cold-Store Ready (-30°C Battery Pack)
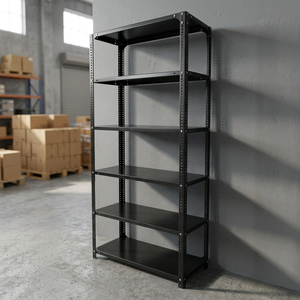
FinePunch Slotted Angle Rack FP-SA-MSPC-001 for Industrial and Storage Applications
- Precision CNC Punching Pitch Patterns
- Rapid Boltless / Bolted Modular Assembly
- Ideal for Maintenance, Tools & Hardware
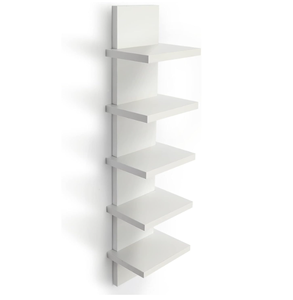
5 Layer Detachable Customizable Wooden Wall Shelf Unit Large Capacity Vertical Shelf
- Hybrid Structural Steel & Wood Decking
- Rapid Detachable Flat-Pack Shipping
- Industrial Showroom & Light Staging
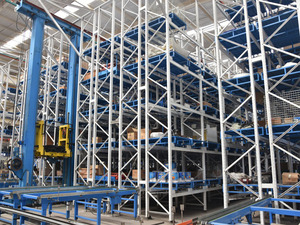
Heavy Duty Double Deep Steel Pallet Racking with Shuttle Drive-In for Cold Rooms
- 50% Reduction in Forklift Aisle Space
- Hot-Dip Galvanized / Epoxidized Finish
- Heavy Section Upright Posts (90/100/120)
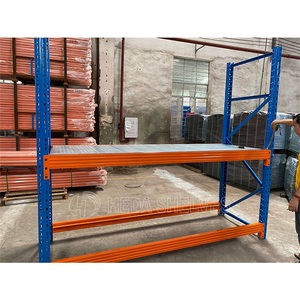
1500kg Per Layer Heavy Duty Shelves Storage Rack Warehouse Pallet Racking System
- Guaranteed 1500kg Uniform Distributed Load
- Interlocking Box Beams with Safety Pins
- Heavy-Duty Wire Mesh Decking Options
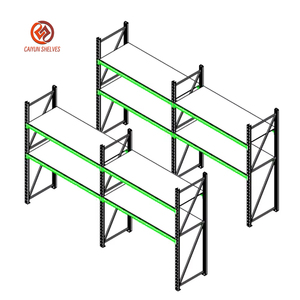
Industrial Storage Rack System - Steel Grow Shelves with Reinforced Wood Platforms
- High-Load Agritech & Commercial Staging
- Corrosion-Resistant Powder Coating
- Fully Modular Width, Depth, & Clearance
Guangzhou Heda Shelves Co., Ltd. — Setting the Benchmark in Heavy Logistics Racking
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into an internationally recognized powerhouse in structural warehouse racking and automated intralogistics infrastructure. Operating across a cutting-edge 30,000 m² production complex with an in-house monthly output exceeding 30,000 metric tons, we bridge the gap between heavy structural engineering and precision industrial storage.
Our core engineering competency centers on direct-from-mill raw material procurement from China's Tier-1 steel corporations (including Baosteel and Shougang Group). Every coil of cold-rolled Q235B and high-yield Q355B steel undergoes rigid mechanical yield verification, spectrometer chemical profiling, and automated multi-stage roll-forming with zero cumulative dimensional drift.
- Free 3D CAD & Structural FEA Layouts
- Seismic Zone Design (Chile, Peru, USA, Japan)
- Automated 60-Meter Powder Coating Tunnel
- Full Container Packing Optimization Plan
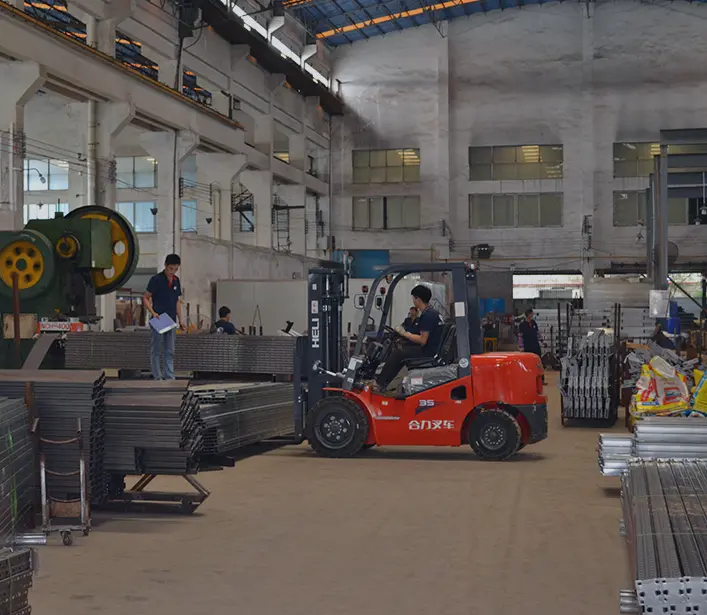
Industrial Shelving Engineering Standards: Comparing Materials & Structural Safety
For global logistics project directors and procurement executives, choosing the correct material grade and manufacturing tolerance determines operational safety, beam deflection margins under cyclic forklift handling, and facility insurance compliance.
| Engineering Parameter | HEDA Standard (Q235B) | HEDA High-Load (Q355B) | US RMI MH16.1 Benchmark | EU FEM 10.2.02 Benchmark |
|---|---|---|---|---|
| Yield Strength ($f_y$) | $\ge 235 \text{ N/mm}^2$ | $\ge 355 \text{ N/mm}^2$ | $\approx 230 - 345 \text{ N/mm}^2$ | $\ge 235 - 355 \text{ N/mm}^2$ |
| Tensile Strength ($f_u$) | $370 - 500 \text{ N/mm}^2$ | $470 - 630 \text{ N/mm}^2$ | $400 - 550 \text{ N/mm}^2$ | $360 - 510 \text{ N/mm}^2$ |
| Elongation at Break ($\delta_5$) | $\ge 26\%$ (High Ductility) | $\ge 22\%$ (Seismic Resilient) | $\ge 20\%$ | $\ge 22\%$ |
| Beam Deflection Limit | 1/200 to 1/250 Span Max | 1/250 to 1/300 Span Max | 1/180 Span Max | 1/200 Span Max |
| Safety Factor Margin | 1.65 to 1.80 Overload Margin | 1.85 to 2.10 Overload Margin | 1.67 Design Factor | 1.50 Partial Safety Factor |
| Surface Pretreatment | 7-Stage Acid Phosphating Wash | Continuous Shot Blasting (Sa 2.5) | Standard Chemical Degrease | Standard Chemical Rinse |
| Coating Thickness & Salt Spray | $60 - 90\,\mu\text{m}$ (ASTM B117 > 500h) | Hot-Dip Galv $\ge 70\,\mu\text{m}$ (> 1000h) | Commercial Powder ($40-60\,\mu\text{m}$) | Standard Polyester Powder |
Future Procurement Trends in Industrial Warehouse Shelving (2025–2030)
Global supply chain uncertainty, escalating warehouse real estate rents per square meter, and warehouse automation are radically altering how industrial shelving systems are purchased, engineered, and amortized.
1. Total Landed Cost (TLC) & Knock-Down Shipping Density
Procurement teams are shifting analysis from simple Ex-Works (EXW) component pricing to holistic Total Landed Cost (TLC). With volatile international container freight rates, warehouse buyers demand high-density knock-down (KD) upright packaging. Designing bolted modular upright frames instead of welded upright ladders reduces container freight requirements by up to 38%, delivering immediate bottom-line project savings upon arrival at regional seaports.
2. Automation-Ready Hybrid Infrastructure (ASRS & Shuttle Synergies)
Modern distribution centers no longer invest in standalone static storage that risks early obsolescence. Procurement contracts increasingly mandate "automation-ready" structural engineering. Selective racking must feature tight structural deflection tolerances (FEM 9.831 / FEM 10.2.02) capable of integrating pallet runners, guide rails, autonomous 4-way radio shuttles, or robotic automated storage and retrieval system (ASRS) cranes without replacing upright structural columns.
3. Environmental ESG Mandates & Low-Carbon Steel Supply Chains
Corporate ESG benchmarks and European CBAM (Carbon Border Adjustment Mechanism) regulations are accelerating demand for transparent Scope 3 carbon tracking in structural steel fabrication. Forward-looking procurement policies penalize high-waste manual fabrication in favor of manufacturers employing electric arc furnace (EAF) scrap-integrated steel coils, lead-free non-toxic epoxy coatings, and fully closed-loop powder recovery filtration lines.
Product Development & Technological Trends in Warehouse Shelving
Racking engineering has transcended simple roll-formed profiles. Modern intralogistics demands active safety sensors, complex seismic finite-element modeling, and ultra-high-yield metallurgy.
FEA-Driven Seismic Resiliency & High-Yield Thin-Wall Roll-Forming
Using ANSYS and SAP2000 3D Finite Element Analysis (FEA), HEDA's structural engineers simulate static and dynamic torsional-buckling stress. By applying multi-bend stiffening ribs into upright columns (up to 12 cold-rolled folding edges), structural stiffness increases by 24% while simultaneously saving deadweight. This high strength-to-weight ratio allows taller upright heights (over 16 meters) in high seismic acceleration zones (e.g., Chile NCh 2369, Peru E.030, and US UBC Zone 4).
IoT-Equipped Smart Racking & Deflection Telemetry
The next generation of high-bay warehouse shelving features embedded strain-gauge micro-sensors and RFID load tags. Real-time optical and strain telemetry monitor continuous live beam deflection. If an overloaded pallet exceeds the permissible structural limit ($L/200$) or an inadvertent forklift impact destabilizes an upright base plate, the central Warehouse Management System (WMS) triggers immediate aisle-quarantine alerts, mitigating catastrophic collapse risks before they occur.
Polymer Nano-Coating & Ultra-Low Temp Cold Chain Durability
With the rapid boom in bio-pharmaceutical cold chains and frozen food trade, standard paint finishes suffer embrittlement, peeling, and corrosion under continuous $-30^\circ\text{C}$ to $-40^\circ\text{C}$ condensation cycles. R&D advancements in zinc-epoxy composite powder coatings with polymer-crosslinked nano-additives prevent moisture penetration. For high-corrosion marine coastal warehouses, specialized automated hot-dip galvanizing lines achieve seamless molecular zinc adhesion exceeding $85\,\mu\text{m}$.
The 10-Stage Precision Manufacturing Workflow Behind Every HEDA Rack
Total quality management is built into our shop floor. From coil slitting to pre-shipment container lashing, our in-house ISO 9001:2015 protocol enforces dimensional verification at every single station.
Raw Steel Spectrometry
Mill Test Certificate verification and chemical spectrometry analysis for C, Si, Mn, P, S composition across every raw coil batch.
Precision CNC Slitting
Automated uncoiling and high-speed rotary shear slitting maintaining ultra-tight width tolerances of $\pm 0.1\text{mm}$.
Multi-Die Punching
High-tonnage continuous hydraulic punching lines stamp 50mm / 75mm tear-drop or butterfly pitch patterns without edge burrs.
Continuous Roll-Forming
Progressive 22-roller cold bending forming machines shape heavy-duty upright sections and interlocking box beams without internal micro-cracks.
Robotic Laser Welding
Automated multi-axis robotic welding cells attach beam connector claw hooks with deep-penetration shield-gas welding, eliminating cold joints.
Surface De-Burring & Polish
Mechanical tumbling and shot-polishing clean weld seams, edges, and corners to prevent snagging during manual carton handling.
7-Stage Acid Phosphating
Full chemical immersion: Alkaline degreasing, clean water rinse, rust-inhibiting acid pickling, surface conditioning, and zinc phosphating.
Electrostatic Powder Spray
Swiss Gema automated powder coating booth delivers uniform $70-90\,\mu\text{m}$ dry film thickness with $180-200^\circ\text{C}$ curing ovens.
Destructive Batch QC
Random destructive sample testing: Upright axial compression, beam four-point bending deflection tests, and cross-hatch coating adhesion checks.
Seaworthy Export Packing
Bundle strapping with corner protective steel sleeves, moisture-barrier shrink wrap, timber blocking, and computer-modeled container weight distribution.
Frequently Asked Questions by Global Logistics & Racking Buyers
Get direct, technically rigorous answers from our chief structural engineers on material standards, seismic calculations, import logistics, and quality assurance protocols.
How do you verify the seismic load capacity for facilities in earthquake-prone regions?
What is the real difference between Q235B and Q355B steel in heavy-duty racking applications?
How do you optimize container loading to prevent damage and reduce ocean freight landed cost?
Can HEDA Shelves manufacture custom upright profiles compatible with existing warehouse racks?
What surface finishing options do you recommend for refrigerated and cold storage environments?
What design data do you need from us to generate a free 3D CAD layout and quotation?
How do you guarantee beam deflection compliance under maximum uniform distributed loads?
What is your production lead time, and how is international on-site assembly handled?
Request Your Free 3D Warehouse CAD Layout & Static Calculation Report
Collaborate directly with our certified structural racking engineers. Send your warehouse floor plan, clear ceiling height, and pallet parameters to receive a zero-obligation 3D rendering, detailed CAD storage layout, and factory-direct price quotation within 24 hours.
Connect with an Engineer
Get immediate technical feasibility support and container freight estimates.
Contact Us