Featured Movable & Mobile Warehouse Racking Solutions
Discover our primary heavy-duty mobile carriages, compact mechanical archives, radio shuttle mobile racks, and industrial space-saving solutions engineered for maximum footprint utilization.
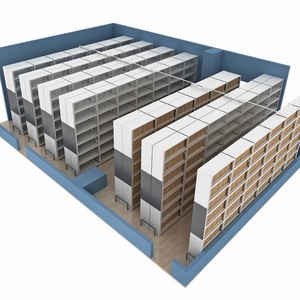
Steel Large Archives Mobile Shelving & Movable Compactor System
- Payload: 80–120 kg per shelf tier
- Drive: High-torque manual mechanical handwheel
- Ideal for: Document storage, healthcare, archives
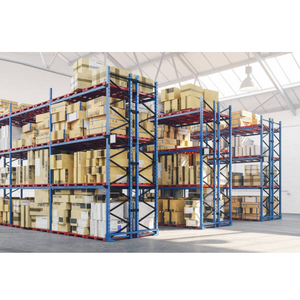
HEDA Heavy Duty Movable Pallet Rack Storage Equipment
- Payload: 1,000–3,000 kg per pallet tier
- Drive: Embedded motorized guide-rail base
- Ideal for: Heavy ceramics, building products, tiles
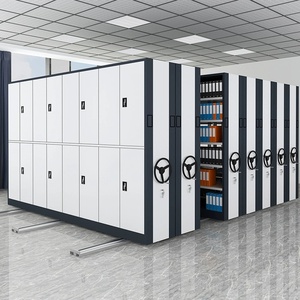
Space-Saving High-Density Compact Shelving System
- Capacity: Up to 500 kg per storage level
- Floor Saving: 50% aisle space elimination
- Ideal for: Electronics, pharma, parts distribution
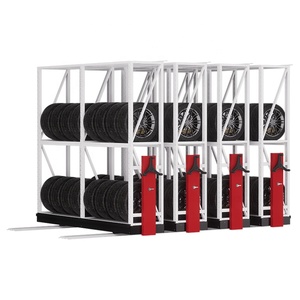
Manual Steel Tire Mobile Racking & Cabinet System
- Profile: Angled beam configuration for cylindrical loads
- Safety: Mechanical track locks and anti-tip devices
- Ideal for: Tire logistics hubs, auto 4S centers
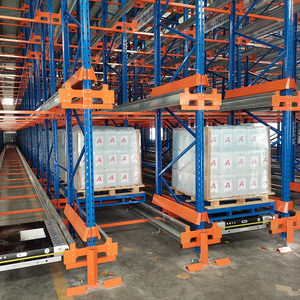
Automatic Heavy-Duty Mobile Pallet Shuttle Racking
- Control: PLC + Wireless Radio Shuttle Integration
- Efficiency: 85% storage density increase
- Ideal for: Cold chain (-25°C), high-throughput FMCG
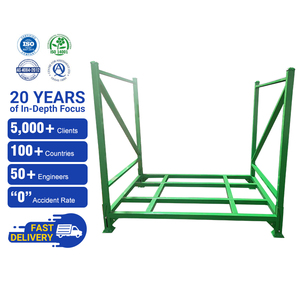
Industrial Heavy Duty 5-Layer Folding Stacking Rack
- Structure: Collapsible, stackable 4 to 5 units high
- Finish: Industrial anti-corrosive powder coat
- Ideal for: Seasonal buffers, containerized logistics
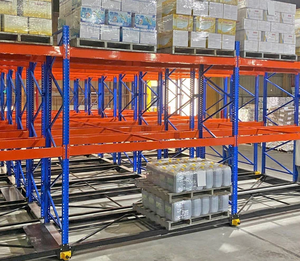
Heavy Load Industrial Mobile Racking (Up to 8,000 Lbs)
- Carriage: High-tensile fabricated mobile steel base
- Access: Single dynamic aisle opens on command
- Ideal for: Heavy machinery, stamping dies, raw steel
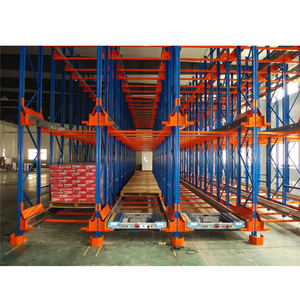
Movable Pallet System with Automated Radio Shuttle
- Kinematics: 1.2 m/s shuttle travel inside channels
- Software: RFID tracking & FIFO / LIFO dynamic routing
- Ideal for: High-turnover food, beverage, deep-freeze
Why Global Supply Chains Source Movable Racking from HEDA Shelves
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into China's premier manufacturer and exporter of heavy-duty industrial racking, mobile racking, and automated warehouse systems.
Seismic-Certified Engineering
We design full movable racking structures to comply with stringent seismic codes globally, including Europe's EN 16681, Chile's NCh 2369 / NCh 433, Peru's E.030, and Colombia's NSR-10. Base plates, ground rails, and anti-derailment bogies are structurally reinforced against seismic dynamic acceleration.
Complimentary 3D & CAD Layouts
Never commit to unverified estimates. Our engineering department prepares complimentary 3D visual renderings, full AutoCAD dimensional floor plans, beam deflection models, and structural calculation reports within 24 to 48 hours based on your facility's clear height and forklift specs.
Full-Line Surface Finishing
All steel uprights and beams undergo automated chemical pickling, ultrasonic degreasing, and phosphating prior to electrostatic powder coating. For cold room facilities (-30°C) and coastal high-humidity hubs, we provide certified hot-dip galvanizing complying with ASTM A123 / ISO 1461 standards.
Rigorous Independent Testing
Backed by CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 accreditation (No. 18624Q00169R0M). Every production batch undergoes destructive testing, tensile yield point verification (Q235B / Q355B grades), and welding seam micro-flaw detection before port dispatch.
Rapid Turnaround & Direct Logistics
With a 30,000-ton monthly capacity, standard movable rack production runs are fulfilled in 14–25 days. Container load optimization software calculates bundle distribution to maximize ocean freight container cubes (40HQ) without transit deformation.
Global Installation Supervision
We provide color-coded numbered component maps, multi-language CAD installation manuals, and live video structural guidance for local contractor teams. Senior site engineers can be dispatched worldwide to supervise rail embedment, leveling, and PLC electrical commissioning.
Kinematics & Volumetric Space Efficiency Comparison
Evaluating mechanical compactors, motorized electric mobile pallet racks, and static selective racking across footprint footprints, accessibility parameters, and lifecycle ROI.
| Storage System Type | Aisle Space Requirement | Floor Space Utilization | Pallet Capacity Gain | Drive Mechanism | Power Consumption | Optimal Industry Application |
|---|---|---|---|---|---|---|
| Standard Selective Pallet Racking | Multiple fixed aisles (3.2m–3.8m each) | 35% – 42% | Baseline (100%) | Static (None) | Zero | High SKU variety, fast pallet velocity |
| Manual Movable Compactor Racking | 1 Floating aisle (0.8m–1.2m) | 70% – 80% | +80% to +100% (Light) | Gear-reduction handwheel & chain | Manual | Archives, pharma, small auto parts, tires |
| Electric Heavy-Duty Mobile Racking | 1 Dynamic aisle (3.0m–3.5m) | 80% – 88% | +85% to +110% | 3-phase AC motorized bogey base | 0.75kW–1.5kW per carriage | Cold storage, industrial components, dies |
| Mobile Base + Automated Radio Shuttle | 1 Consolidated operating aisle | 88% – 94% | +120% to +160% | Motorized mobile base + 24V Shuttle | Dual-system hybrid electric | High-throughput deep freeze, agro-export |
Rail Tolerances & Slab Settlement
Heavy-duty movable pallet racking puts massive point loads on the concrete slab. Floors must comply with DIN 18202 Group 3 or ASTM E1155 F-min 75 standards. HEDA Shelves utilizes laser-leveled embedded tracks anchored with chemical resin studs to prevent rail deflection under 20-ton carriage payloads.
Photoelectric Curtains & Emergency Stops
Safety is paramount when moving tons of steel. Our motorized carriages feature optical safety light curtains along the aisle floor line, proximity bumper switches, and mushroom emergency cutoffs. If an operator or forklift breaks the optical beam during movement, braking occurs instantly within ≤100 milliseconds.
WMS Handshake & Remote Radio Control
Modern movable racking does not rely on operators running back and forth to push buttons. HEDA mobile systems interface directly with Warehouse Management Software (WMS). Forklift drivers trigger aisle opening via RF cabin remotes while approaching, slashing order-picking cycle times by 38%.
Future Procurement Trends for Movable Warehouse Racking (2025–2030)
As land costs surge and logistics operators prioritize carbon efficiency, movable racking procurement is shifting rapidly toward automated, energy-conscious, and modular systems.
Rapid Expansion of Cold-Chain Mobile Bases
Refrigerated and blast-freezer warehouse spaces (-20°C to -30°C) represent the highest utility costs in modern logistics. Every cubic meter of uncooled dead air in fixed aisles burns excessive energy. Procuring electric mobile racking in refrigerated distribution centers reduces electricity consumption per pallet spot by up to 45% by condensing the thermal footprint.
Micro-Fulfillment and High-Bay Urban Warehousing
Last-mile delivery centers positioned near metropolitan borders face severe square-footage constraints. Procurement managers are prioritizing high-bay mobile racking reaching 8 to 12 meters in clear height. These setups combine multi-level mobile carriages with articulated narrow-aisle forklifts or reach trucks to maximize vertical cube density.
Smart IoT Diagnostics & Predictive Maintenance
Smart carriages equipped with vibration sensors, cycle counters, and thermal motor monitoring are rapidly replacing basic electromechanical units. Procurement contracts now demand onboard PLC telemetry that reports motor amperage spikes, rail alignment deviations, and chain lubrication cycles directly to maintenance dashboards before hardware failures occur.
Decarbonized Steel & Sustainable Manufacturing
Global procurement standards under Scope 3 carbon auditing are forcing supply chain directors to verify manufacturer sustainability. HEDA Shelves leads this shift through certified electric arc furnace (EAF) steel sourcing, non-toxic heavy-metal-free powder coatings, and regenerative motor drives that return kinetic braking energy into the facility grid.
Modular Hybrid Configurations
Rigid, monolithic systems are giving way to adaptable configurations. Buyers are specifying modular mobile bases capable of switching between pallet beams, cantilever arms, and tire racks as seasonal inventories rotate. Modular wheel-load bogies allow future bay expansions without replacing existing rail beds or electrical control panels.
Strict Seismic Verification on Imported Steel
With major warehouse growth throughout the Pacific Rim (Chile, Peru, California, Japan), international insurers refuse coverage without third-party seismic sign-offs. Procurement directors now mandate full dynamic finite element analysis (FEA) showing beam connector rotational stiffness and anchor pullout calculations under site-specific ground accelerations.
Critical Engineering Checklist for Movable Racking Procurement
Ensure smooth deployment, structural integrity, and flawless operational handoffs by verifying these mechanical, civil, and electrical parameters before issuing purchase orders.
Slab Load-Bearing Capacity & Flatness
Movable racking consolidates entire warehouse storage blocks into concentrated moving point loads. Verify that your concrete slab has a minimum compressive strength of 30–35 MPa and can sustain wheel loadings of 30 kN to 60 kN per wheel. Embedded rails must be leveled to ±1mm over 10 meters to prevent carriage motor binding.
Motor Sizing & Synchronized Drive Shafts
Dual-motor or centralized continuous drive shafts must deliver balanced torque across all wheel bogies. Ensure carriages utilize soft-start variable frequency drives (VFD) to prevent pallet jolts or tipping during startup and deceleration. Carriage speeds should be calibrated between 4.0 and 5.5 meters per minute.
Fire Protection & Night Park Mode
Movable racks must integrate directly with facility fire suppression systems. Upon receiving an alarm signal from ceiling smoke or heat sensors, the system must automatically activate "Night Park" mode, opening equal ventilation gaps between all mobile carriages to allow in-rack sprinklers to penetrate the stacks.
Steel Metallurgy & Cold-Chamber Resilience
For sub-zero cold room environments, ordinary structural steels (Q235A) risk brittle fracture along weld lines. Mandate high-impact Q355D or Q355E certified structural steels tested for Charpy V-notch impact energy at -20°C and -40°C, paired with low-temperature motor lubricants and freeze-resistant cabling.
Movable Warehouse Racking Procurement FAQ
Clear, definitive answers to the most common technical, logistics, and operational questions asked by international supply chain directors and warehouse owners.
What makes movable warehouse racking more cost-effective than building a warehouse expansion?
Can HEDA Shelves engineer movable racking systems for active seismic zones?
What happens if there is an electrical power outage while using motorized mobile racking?
What are the floor slab requirements for installing heavy-duty mobile racking?
How is overseas shipping, container stuffing, and damage prevention handled?
What are typical manufacturing lead times and production capacities?
Can we customize rack beam heights, load capacities, and powder coat colors?
What safety systems protect personnel and equipment in the dynamic aisle?
Request Your Free 3D Movable Racking Layout & Cost Model
Send our senior engineering team your warehouse dimensions, ceiling clearance, and pallet specifications. We deliver an engineered AutoCAD drawing, 3D visualization, and detailed CIF/FOB quote within 24 hours.