Featured Industrial Rack & Shelving Systems
Manufactured from high-tensile certified Q235B and Q355B cold-rolled structural steel. Every system is precision-punched, robotic-welded, and electrostatically powder-coated to deliver maximum seismic resilience and long-span load capacity.
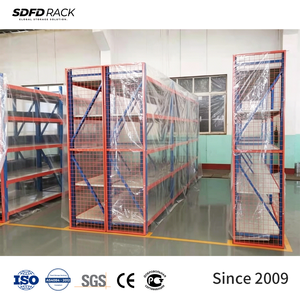
Wholesale 2400x600x2200 Medium Duty Longspan Shelves (4 Layers / 400kg Capacity)
Upright Pitch: 50mm adjustable
Decking: Cold-rolled steel / wire mesh
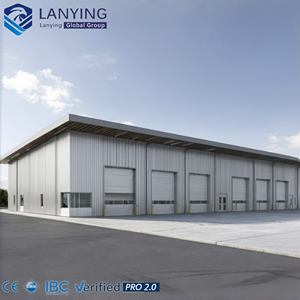
Industrial Prefab Steel Structure Warehouse Building for Logistics & Storage
Clear Span: 18m–36m column-free
Wind/Seismic: Up to 140km/h & Zone 4
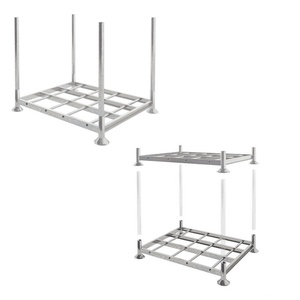
Heavy Duty Steel Pallet Racking & Metal Stacking Truck Tire Storage Rack
Config: 4 to 6 tiers stackable
Mobility: 4-way forklift entry
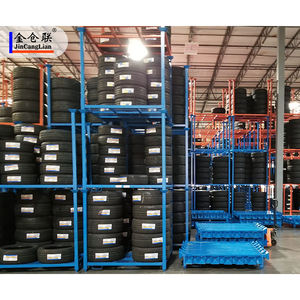
High Standard Steel Tubular Warehouse Racks & Corrosion-Resistant Stacking System
Anti-Corrosion: Hot-dip / epoxy powder
Safety Index: Structural safety factor 1.65
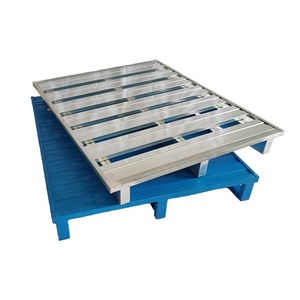
1000–1500kg Long-Life Powder Coated & Galvanized Steel Industrial Pallets
Surface: Hot-dip zinc or hybrid epoxy
Standard: Euro & US GMA dimensional spec
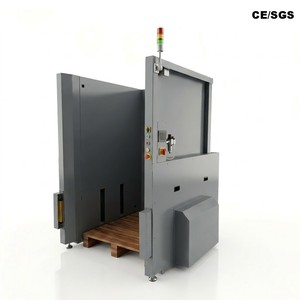
Electric Pallet Flow Rack Dispenser & Labor-Saving Automatic Pallet Feeder
Control: Siemens PLC & Optical Sensors
Application: FIFO production dispatch
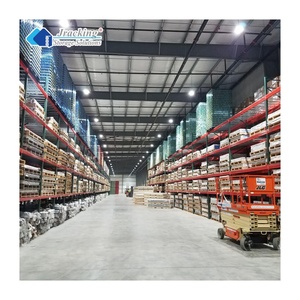
Jracking US Standard Teardrop Pallet Racking System (Interchangeable In-Stock)
Compliance: RMI MH16.1 & AISI S100
Beam Load: Up to 4,500 kg per pair
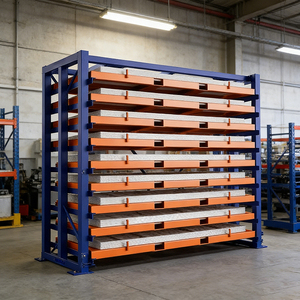
High-Capacity Vertical Sheet Metal Rack | Forklift Roll-Out Drawer System
Extension: 100% full roll-out crank
Protection: Laser cut sheet edge guards
(Established 2001)
Capacity in Tons
Workshop Area
& 10,000+ Projects
Engineering Integrity, Steel Metallurgy & Global Standards
When global warehouse directors and tier-1 3PL operators procure rack shelving systems from Chinese manufacturers, the primary vectors of risk are not merely piece prices, but structural yield stability, deflection ratios under full operational load, seismic ductile behavior, and consistency of automated roll-forming.
As an engineering-driven manufacturer based in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. approaches industrial storage design through the lens of finite element analysis (FEA) and international design codes. The performance of industrial pallet racks begins at the atomic structure of the primary coil. We strictly source prime cold-rolled steel coils conforming to standard GB/T 700 Q235B (Yield Strength $f_y \ge 235 \text{ MPa}$, Tensile Strength $370\text{--}500 \text{ MPa}$) and high-strength low-alloy structural steel GB/T 1591 Q355B (Yield Strength $f_y \ge 355 \text{ MPa}$, equivalent to ASTM A572 Grade 50 or European S355JR). Utilizing Q355B high-grade steel allows up to a 15–22% optimization in profile deadweight while elevating load-bearing thresholds and post-elastic energy dissipation during seismic excitation.
Modern cold roll-forming lines feature multi-station progressive rollers that eliminate residual micro-stresses within upright corners. The geometric profile of our Omega ($\Omega$) upright sections features continuous stiffening ribs along the flange and web, engineered specifically to resist torsional-flexural buckling under axial compression. Upright hole punching (50mm, 75mm European pitch, or 2-inch teardrop US configuration) is executed on computerized high-speed mechanical press banks before roll-forming, guaranteeing hole pitch accumulative tolerances within $\pm 0.5\text{ mm}$ across an entire 12-meter upright column.
| System Typology | Standard Steel Grade | Max Bay Capacity | Aisle Requirement | Selectivity vs Density | Governing Global Codes |
|---|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B | Up to 24,000 kg / bay | 3,000 – 3,500 mm (Counterbalance) | 100% Direct Access (Low Density) | EN 15512 / RMI MH16.1 |
| Drive-In / Drive-Through | Q235B Welded Box | Up to 18,000 kg / lane | Forklift enters racking lane | LIFO / FIFO (Ultra-High Density) | FEM 10.2.02 / AS 4084 |
| Radio Shuttle Automation | Q355B Cold Formed | Up to 40,000 kg / lane | Single loading & retrieval bay | Semi-Automated LIFO/FIFO | EN 15512 / ISO 9001 |
| Heavy-Duty Cantilever | Hot-rolled H-Section / Q235B | 3,000–5,000 kg / arm | Guided VNA or Side-loader | 100% Selectivity for Long Items | AISC 360 / EN 1993 |
| Rack-Supported Mezzanine | Q235B / Q355B Hybrid | 300–1,200 kg / m² | Manual stairs / vertical freight lift | Multi-Tier Picking & Storage | IBC 2024 / CE EN 1090 |
10 Controlled Production Phases from Slit Coil to Export
Every component manufactured inside our 30,000 m² factory undergoes strict quality checkpoints. We eliminate structural variances through automated cold-roll forming, robotic laser cutting, and an automated multi-stage pre-treatment coating line.
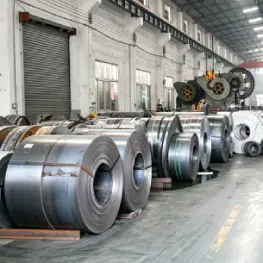
Raw Material Assay
Spectrometric & tensile testing of certified Q235B/Q355B coils before slitting.
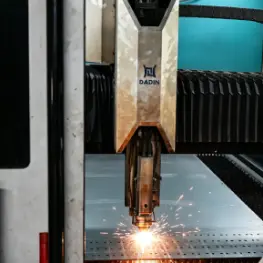
Precision CNC Shearing
High-speed CNC slitting ensuring raw strip width tolerances within ±0.2mm.
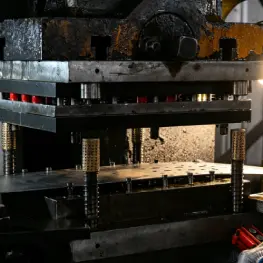
Automated Punching
High-speed punching beds create teardrop, diamond, or metric butterfly pitches.
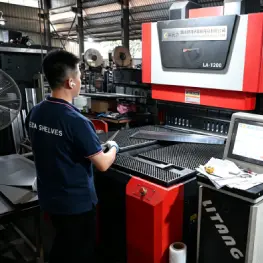
Cold Roll-Forming
Multi-stand profile forming lines ensure tight cross-sectional rigidity.
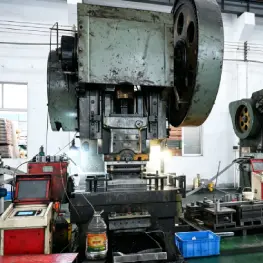
Beam Step-Forming
Continuous roll-forming of box and step beams with interlocking seam closure.
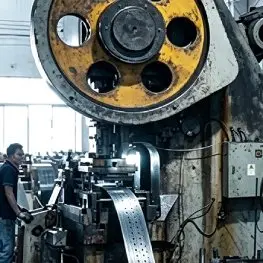
Robotic Polishing
Mechanical deburring & edge smoothing to safeguard installer ergonomics.
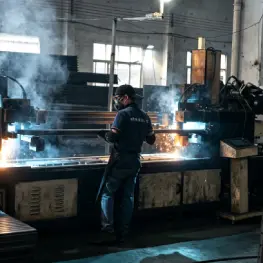
Robotic Welding
CO2/Argon mixed-gas robotic welders bind connector brackets to beam ends.
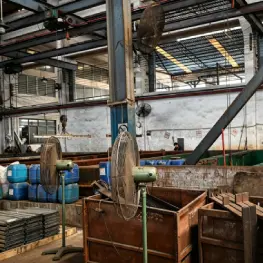
Chemical Pre-Treatment
Multi-stage degreasing, acid pickling & silane phosphating to halt micro-oxidation.
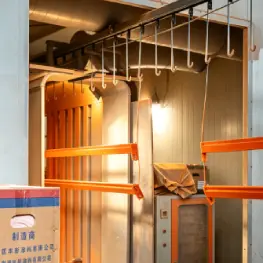
Powder Coating Line
Automated electrostatic thermoset powder cured at 180–200°C (60–90μm thickness).
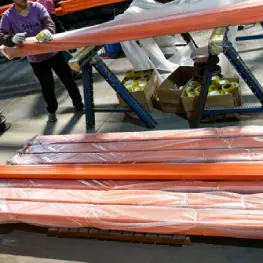
QC & Ocean Bundling
Dimensional micrometer checks, cross-hatch adhesion tests & steel strapped pallets.
Future Procurement Trends in Industrial Storage (2025–2035)
Warehouse supply chains are transitioning rapidly from static racking toward dynamic, automated, and climate-resilient frameworks. Sourcing decisions now prioritize flexibility, structural longevity, and software interoperability.
AS/RS & Shuttle Synergies
Buyers are shifting away from pure manual selective racks toward high-density Radio Shuttle systems and Clad-Rack AS/RS buildings. Procurement demands tighter deflection limits ($L/300$ vs standard $L/200$) to facilitate millimetric autonomous crane positioning.
Total Landed Cost Modeling
Leading 3PLs evaluate suppliers through Total Landed Cost (TCO) calculators. Factory-engineered knockdown (CKD) packing that increases 40ft High Cube container volumetric utilization by 25–35% reduces overseas ocean freight overhead dramatically.
Tropical & Cold-Chain Resiliency
Explosive growth in fresh food e-commerce demands heavy corrosion protection. Sourcing requirements now mandate multi-stage phosphating, low-temperature ductile alloys, and hot-dip galvanized finishes (ASTM A123) for condensation zones.
BIM & Digital Twin Integration
Enterprise EPC contractors mandate Autodesk Revit BIM models and 3D IFC structural files prior to PO release. Racking layouts are checked in virtual space for MEP piping clashing, sprinkler beam clearances, and seismic anchor bolt spacing.
Audited Quality Systems & Global Compliance
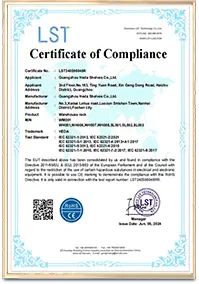
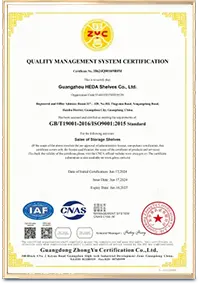
Procurement risk mitigation requires documented proof. Guangzhou Heda Shelves Co., Ltd. products operate under continuous CE and ISO quality assurance, vetted for international construction tenders.
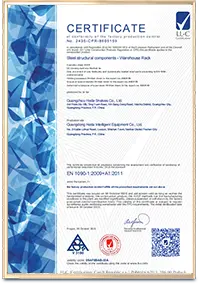
CE Certificate
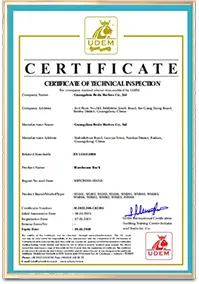
ISO 9001:2015 System
Mechanical Testing QA
RoHS Coating Compliance
Industrial Sourcing & Engineering FAQ
Key technical, logistical, and structural answers to simplify your supply chain due diligence when importing warehouse racking systems from China.
What seismic criteria are integrated for seismically active regions?
How does HEDA guarantee beam deflection compliance under maximum rated load?
What are the typical lead times for standard vs customized racking orders?
How do you protect components from corrosion in humid or coastal climates?
What information is required to generate an engineering CAD & 3D proposal?
How are installation, alignment, and site commissioning managed internationally?
Accelerate Your Warehouse Capacity with Direct-Factory Engineering
Consult directly with senior warehouse storage engineers at Guangzhou Heda Shelves Co., Ltd. We provide free AutoCAD architectural layouts, structural deflection calculations, and factory-direct FOB/CIF container shipping quotations tailored to your operational specifications.