High-Efficiency Material Handling & High-Density Racking Systems
Engineered for seamless integration with high-velocity distribution hubs, fulfillment lines, and automated supply chains worldwide.
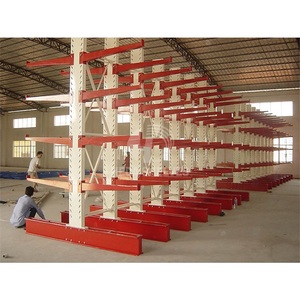
Heavy Duty Cantilever Racking Custom Cantilever Shelving Racking System Warehouse Cantilever for Industrial Storage
Designed for heavy profile loads, long pipes, timber packs, and structural sheet materials with adjustable load-bearing arms up to 3,000 kg capacity.
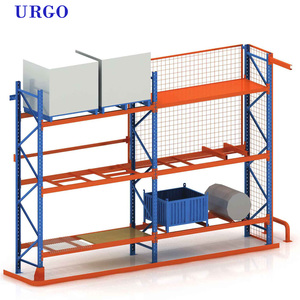
Very Narrow Aisle Pallet Rack / VNA Heavy Duty Racking System
Maximizes vertical cubic capacity with high-precision guide rail systems, reducing operating aisle widths down to 1.6 meters for turret-truck operations.
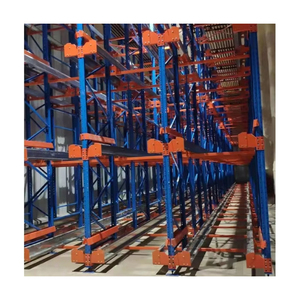
High Efficiency Auto Rack Shuttles Warehouse Racking Stacking Racks & Shelves Storages Rack Pallet Shuttle System
Semi-automated deep-lane dynamic pallet carrier infrastructure, delivering effortless FIFO/LIFO turnover for fast-moving consumer goods and cold storage facilities.
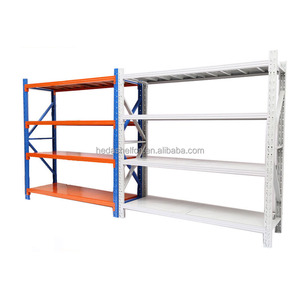
Wholesale Price Industrial Boltless Storage Rack 4 Tier Metal Shelving Units Warehouse Steel Heavy Duty Stacking Racks Shelves
Modular multi-tier hand-loaded boltless shelving engineered for fast deployment, maintenance workshops, high-density parts storage, and ergonomic assembly stations.
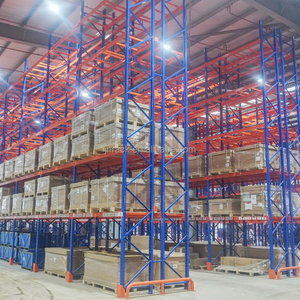
Heavy-Duty Corrosion Protected Pallet Racking Systems For Warehouse And Factory Storage By Jinhui Warehousing Suppliers
Surface-treated with specialized multi-phase pickling, phosphating, and heavy powder coating, built to resist harsh chemical, coastal, and refrigerated humidity environments.
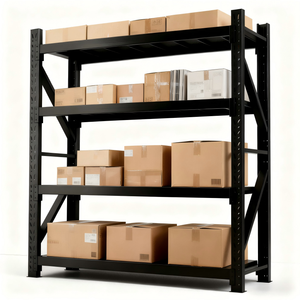
Adjustable Industrial Warehouse Stacking Racks & Shelves Cargo & Storage Equipment Multi Tier Storage Rack Shelving Units
Versatile multi-tier stacking frames providing rapid beam step adjustment, flexible cargo containment, and high uniform distributed load limits per storage tier.
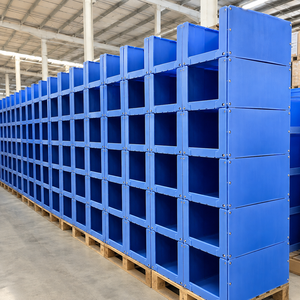
PP Corrugated Plastic Stackable Warehouse Picking Bins Front Opening Warehouse Shelf Storage For Industrial Parts
High-durability polypropylene corrugated front-hopper picking bins optimized for carton flow beds, order replenishment workstations, and small-parts SKU sorting.
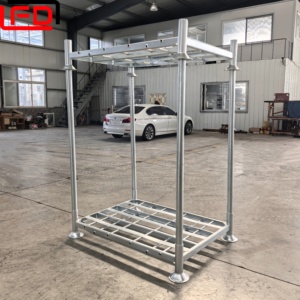
Dip Galvanized Industrial Storage Logistic Equipment Pallet Rack Warehouse Stackable Post Pallet Metal Pallet
Heavy duty hot-dip galvanized post pallets designed for dense vertical stacking without static rack structures, eliminating floor footprint bottlenecks in transshipment zones.
Engineering Principles of Carton Flow Racking in High-Throughput Fulfillment
A rigorous structural analysis of gravity-driven dynamic flow storage, kinetic deceleration, and picker biomechanics.
In contemporary intralogistics, split-case picking, piece picking, and high-SKU inventory turnover present persistent operational bottlenecks. Traditional static shelving systems require material handlers to navigate extensive horizontal travel paths, which can constitute up to 65% to 70% of total order fulfillment time. As a globally verified carton flow racking supplier and exporter, our engineering methodology addresses this labor-intensive inefficiency by leveraging natural gravitational potential energy through inclined roller bed infrastructures.
Carton flow racking—frequently classified as dynamic gravity live storage—segregates stocking and picking activities into separate dedicated aisles. Inventory replenishment personnel stage cartons, totes, or bins onto the elevated charging face (rear loading aisle). Under controlled gravitational gradients, inventory rolls autonomously down durable skate-wheel or steel roller tracks toward the discharge face (front retrieval picking aisle). This architectural configuration establishes an uncompromising First-In, First-Out (FIFO) stock rotation cycle, indispensable for high-turnover consumer goods, pharmaceutical logistics, and cold-chain perishables where strict batch-traceability and expiration monitoring are non-negotiable.
From a biomechanical and structural engineering perspective, the system integrates several critical elements: cold-formed structural steel uprights, heavy-duty box beams, intermediate drop-in roller track supports, full-width pick trays (tilted presentation shelves), and precision tracking dividers. The pick tray angle is typically calibrated between 15° and 25° at the operator pick face, presenting the open carton directly toward the warehouse picker. This reduces spine flexion, eliminates repetitive deep-reach strain, and boosts individual picker accuracy and units-per-hour (UPH) performance by upwards of 40% to 50% compared to static selective bin shelving.
| System Parameter | Skate Wheel Flow Track | High-Density Steel Roller Track | Reinforced Aluminum Flow Bed |
|---|---|---|---|
| Load Capacity Per Meter | 50 kg - 120 kg / meter | 150 kg - 350 kg / meter | 100 kg - 250 kg / meter |
| Incline Pitch Range | 2.5% to 4.5% (approx. 1.5° - 2.6°) | 2.0% to 3.8% (for heavy containers) | 2.5% to 4.0% (variable pitch clips) |
| Roller / Wheel Material | High-impact virgin Polypropylene (PP) | Cold-drawn galvanized precision steel | Anodized extruded aluminum frame / alloy hubs |
| Operating Temperature | -10°C to +45°C ambient | -35°C to +50°C (Cold chain blast rated) | -25°C to +40°C cleanroom certified |
| Recommended Unit Loads | Uniform corrugated carton boxes | Heavy plastic totes, metallic containers | E-commerce mixed-substrate containers |
| Structural Standards | EN 15512, RMI ANSI MH16.1 compliant | FEM 10.2.02, CE 2435-CPR-8605159 | ISO 9001:2015, OSHA Safety Standards |
Emerging Procurement & Technological Trends in Carton Flow Racking
Anticipate global shifts in automation integration, supply chain sustainability, and high-velocity order profile architectures.
1. Convergence with Autonomous Mobile Robots (AMR) & AGVs
Global fulfillment centers are shifting toward automated replenishment. Future-proof carton flow designs are engineered with robotic pick-to-belt clearance, elevated discharge docks, and sensorized rear charging decks allowing automated tow vehicles and AGVs to execute back-replenishment without physical worker intervention in active travel lanes.
Robotic Intralogistics2. Sensorized Pick-to-Light & Put-to-Wall Native Interfaces
Modern B2B enterprise procurement dictates zero-defect picking lines. Racking frames are increasingly prefabricated with concealed wiring channels, integrated magnetic light-display bus bars, and infrared optical break-beam sensors. When an order fires from the WMS, illuminated light modules guide operators instantly to the designated carton flow channel.
Digital Order Routing3. Cryogenic Polymers for Rapid Cold-Chain Expansion
With explosive growth in pharmaceutical biologic cold-rooms and frozen grocery logistics, carton flow track rollers face high brittleness risks at -25°C to -35°C. The procurement trend focuses on high-impact polyoxymethylene (POM) wheels engineered with food-grade lubricants and low thermal contraction tolerances to prevent wheel binding.
Sub-Zero Engineering4. Multi-Substrate Universal Gravity Beds
Warehouses frequently change packaging vendors, transitioning between virgin corrugated boxes, recycled kraft containers, and molded plastic distribution totes. Universal full-width roller beds with drop-in galvanized steel axles are replacing narrow track channels, accommodating fluctuating carton footprints without tedious channel adjustments.
Agile SKU Adaptability5. Landed-Cost & Freight Optimization in Export Sourcing
Global procurement teams prioritize total landed cost efficiency over basic ex-factory unit pricing. Importers mandate precision nested roll-formed profiles, knockdown flow bed construction, and containerization loading plans engineered to maximize 40ft High Cube container volumetric capacity up to 98% while preventing transit coating abrasion.
Global Sourcing EconomicsDirect-From-Factory Manufacturing Authority Since 2001
End-to-end metallurgical control, robotic forming lines, and structural compliance certified across world markets.
Heavy-Scale Engineering, Traceable Steel, and Zero-Intermediary Supply
Headquartered in Guangzhou with an advanced 30,000 square meter manufacturing campus, Guangzhou Heda Shelves Co., Ltd. has stood at the forefront of heavy industrial racking fabrication for over 25 years. Employing more than 300 seasoned engineers, structural draftsmen, and production technicians, we maintain a robust monthly manufacturing capacity of 30,000 tons of finished steel racking equipment.
- Certified Structural Steels: Exclusively formed from prime high-tensile Q235B and Q355B cold-rolled structural steel, certified for yield stress and bending limits under international test protocols.
- Automated 10-Stage Precision Production: In-house uncoiling, precision computer-controlled laser shearing, high-speed multi-stage column punch presses, automated continuous roll forming, robotic welding, and automated thermosetting electrostatic powder coating.
- Free Tailored Engineering Design: Full bespoke 3D CAD modeling, load deflection analysis, dynamic roller pitch calculations, and warehouse space optimization provided free of charge prior to order sign-off.
- Seismic & Harsh Environment Compliance: Dynamic structural configurations calibrated for regional seismic parameters (Chile NCh 433/2369, Peru E.030, Colombia NSR-10, US IBC/UBC) with specialized anti-corrosion galvanized and coastal epoxy options.
Certified Export Quality & Project Track Record
Our quality control infrastructure conducts stringent batch-level metallurgical checks, weld penetration tests, tensile loading inspections, and electrostatic coating thickness audits across every export batch.
Delivered to over 10,000 completed warehouse and logistics installations across South America, North America, Southeast Asia, Europe, and the Middle East.
Carton Flow Racking Procurement: Frequently Asked Questions
Essential engineering, logistics, operational, and commercial insights for facility managers and purchasing directors.
What gradient or slope angle is required for optimal carton flow operation?
How does carton flow racking integrate with existing pallet racking or pick modules?
What is the difference between plastic skate wheel tracks and full-width steel roller tracks?
How are lane dividers configured to prevent SKU cross-over and carton jamming?
What mechanical devices prevent carton impact damage at the picking face?
What surface treatment is best suited for humid, coastal, or refrigerated cold storage?
How long is the typical manufacturing lead time for standard and customized projects?
How are components packaged to prevent damage during long-distance ocean shipping?
Can carton flow racking be retrofitted with Pick-to-Light (PTL) systems later?
What essential data is required for HEDA engineers to produce a free 3D CAD layout?
Request Your Engineered Carton Flow Layout & Factory Quote
Accelerate your order-picking throughput, eliminate worker congestion, and recover valuable warehouse floor area. Connect directly with Guangzhou Heda Shelves' senior technical team for free 3D CAD modeling, custom loading calculations, and competitive factory-direct export pricing.
Inquire Now