Industrial Heavy-Duty Racking Systems Portfolio
Engineered for extreme yield resistance, maximum cubic storage utilization, and rigorous warehouse safety standards. Discover our precision-manufactured product series trusted across 120+ nations.
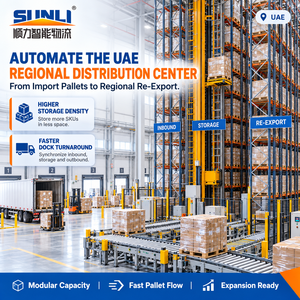
SHUNLI SL-AS004 Factory Customized Heavy Duty Automated AS&RS Pallet Stacking Rack
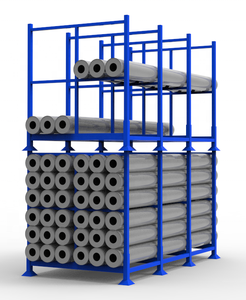
Custom Commercial Stack Metal Pallet Racking Fabric Roll Stacking Shelves
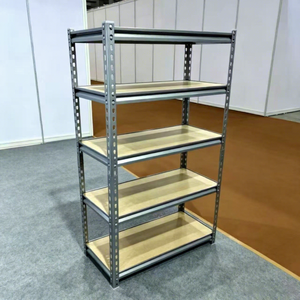
5 Tier Boltless Shelving Unit 150kg Per Layer Metal Storage Rack with Board
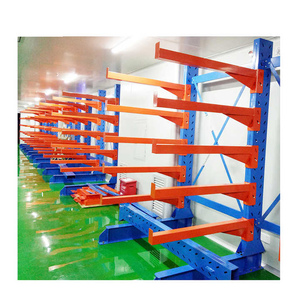
High Quality Heavy Duty Cantilever Rack Shelf 5-Layer Adjustable Racking
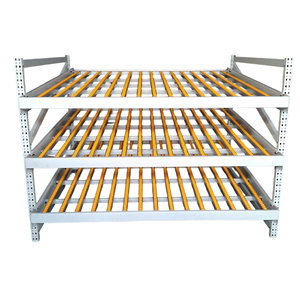
AOCHEN Collapsible Powder Coated Logistics Mobile Gravity Pallet Roller Rack
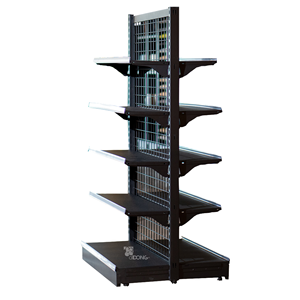
Custom Double-Sided Vertical Heavy Display Supermarket Gondola Shelving
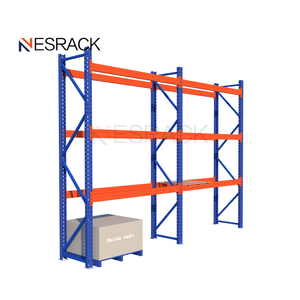
European Standard Industrial Steel Selective Pallet Racking Shelving System
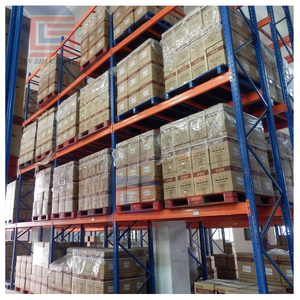
Industrial Heavy Duty Steel Pallet Rack for Distribution Center Logistics
Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves)
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has evolved into an international vanguard in the research, mechanical engineering, structural optimization, and export of heavy-duty industrial warehouse racking systems. Spanning an expansive 30,000 m² state-of-the-art manufacturing campus, our facility houses proprietary CNC roll-forming lines, automated punching arrays, robotic CO₂ gas-shielded welding units, and continuous electrostatic powder coating tunnels.
Operating strictly under ISO 9001:2015 quality management and carrying prestigious CE Certificate No. 2435-CPR-8605159, HEDA Shelves safeguards global supply chain operations. Every racking assembly is mathematically validated through Finite Element Analysis (FEA) to endure extreme dynamic buckling moments, seismic shear forces, and thermal contraction cycles in sub-zero cold rooms.
- Certified CE & ISO 9001:2015 Quality System
- Complimentary 3D CAD & BIM Structural Modeling
- Seismic Dynamic Compliance (EN 15512, RMI MH16.1)
- High-Precision In-House Pickling & Phosphating
Structural Engineering Baseline
Technical audit parameters applied to HEDA heavy-duty upright frames and box beams prior to container loading:
| Engineering Attribute | Standard Specification |
|---|---|
| Steel Raw Material | Baosteel Q235B / Q355B Hot-Rolled Structural Alloy |
| Deflection Coefficient | Maximum L/200 Under Rated Design Service Load |
| Safety Factor | 1.5 to 1.65 Structural Resistance Ratio |
| Welding Integrity | AWS D1.1 Robotic CO₂ Shielded Penetration |
| Coating Deposition | 60–80 Microns Thermoset Epoxy Powder (RoHS) |
| Seismic Calculation | NCh 2369, Peru E.030, NSR-10, Eurocode 8 |
The 10-Step Heavy-Duty Industrial Production Cycle
To maintain unwavering load compliance across decades of dynamic warehouse loading, every single beam, frame, anchor plate, and safety pin travels through our monitored 10-tier fabrication line.
Spectrometric Testing
Mill test certificates verified with optical emission spectrometers for tensile carbon & manganese ratio.
High-Speed Punching
High-tonnage continuous CNC presses punch pitch teardrop/diamond holes at ±0.1mm dimensional precision.
Precision Cold Slitting
Automated shearing and de-coiling guarantee strict profile edge tolerances prior to section bending.
Continuous Roll-Forming
Multi-station hardened roll-tooling shapes cold steel into high-moment Omega upright columns.
Interlock Seam Welding
Interlocking box beams and structural channel profiles undergo seamless seam rolling and crimping.
Robotic Claw Welding
Panasonic 6-axis robotic welding cells fuse 3-claw/4-claw connector plates to beam extremities.
Chemical Pretreatment
Full immersion 4-stage pickling, ultrasonic degreasing, and zinc phosphating strip micro-impurities.
Electrostatic Coating
Automated GEMA spray booths apply uniform thermoset powder cured in a 200°C infrared baking zone.
Batch Deflection QA
Random destructive & non-destructive load tests verify crosshead displacement against finite limits.
Maritime SKD Packing
Bundling with high-density corrugated spacers, moisture-barrier wraps, and structural steel strapping.
Engineering Architecture & Storage Density Comparison
Selecting the correct heavy-duty racking archetype requires balancing pallet selectivity, inventory turnaround dynamics (FIFO vs. LIFO), floor area footprint, and handling equipment compatibility.
| Racking System Architecture | Footprint Density | SKU Selectivity | Inventory Flow | Floor Utilization | Recommended Industrial Use Case |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard | 100% (Direct Access) | FIFO / LIFO | 40% - 45% | Multi-SKU FMCG, 3PL Warehouses, General Distribution Hubs |
| Double Deep Racking | Moderate-High | 50% (Two Pallets) | LIFO | 55% - 60% | Identical batch warehousing, cold storage with pantograph reach trucks |
| Drive-In / Drive-Through | High Density | Low (Lane Dependent) | LIFO (Drive-In) / FIFO | 65% - 75% | Beverage bottling, cold storage facilities, seasonal high-volume lots |
| Radio Shuttle Cart Racking | Ultra High Density | Semi-Automated | Flexible FIFO or LIFO | 75% - 85% | Large-scale cold chains, meat processing, dairy, chemical commodities |
| Heavy Duty Cantilever Racking | Custom Linear | 100% Unobstructed | FIFO / LIFO | Variable Linear | Steel tubing, extrusion bars, structural timber, drywall & sheet metal |
| Automated AS/RS High-Bay | Maximum Vertical | 100% Automated | Computer-Optimized | 85% - 95% | Tier-1 E-commerce fulfillment, mega pharmaceutical distribution centers |
Future Procurement Trends in Heavy-Duty Racking (2025–2035)
Global supply chains are reshaping warehouse procurement. Stay ahead with four macroeconomic shifts governing how leading distribution operators source industrial racking.
Automation & Shuttle-Ready Upgrades
Procurement teams are shifting capital expenditure from static racks toward modular systems pre-engineered for autonomous mobile robots (AMRs) and radio shuttle integration without post-weld site retrofits.
Seismic Resilience in Tender Mandates
Supply chain leaders operating in the Pacific Rim, Andean corridor, and Southern Europe now enforce rigorous dynamic response modeling (EN 15512, NCh 2369, RMI MH16.1) as mandatory procurement criteria.
Circular Cold-Rolled Metallurgies
Buyers prioritize environmental product declarations (EPD) and micro-alloyed hot-rolled coil steels (Q355B/SS400) that achieve superior yield strength (≥355 MPa) while reducing total embodied carbon footprint.
Factory-Direct Landed Cost Optimization
Eliminating middleman margins, modern importers leverage direct factory engineering teams in China for precision 3D load optimization, reducing ocean freight costs per pallet location by up to 28%.
Frequently Asked Questions for Industrial Racking Buyers
In-depth technical answers addressing load calculations, international engineering compliance, container stuffing economics, and long-term facility safety.
Under international standards (such as EN 15512 and RMI MH16.1), the maximum permissible deflection under maximum uniformly distributed load (UDL) is calculated as L/200, where L is the clear span of the horizontal beam. For example, a 2,700mm beam rated at 3,000kg will not deflect more than 13.5mm at its center point. HEDA Shelves validates all beam sections via physical hydraulic test beds and FEA software before mass manufacturing.
We utilize certified primary structural steel coils sourced directly from top mills (Baosteel, Shougang). Upright columns are rolled from high-yield Q355B (equivalent to ASTM A572 Grade 50 / EN 10025 S355JR), featuring a minimum yield strength of 355 MPa. Beams are cold-formed from Q235B or Q355B depending on deflection parameters. Full Mill Test Certificates (MTC 3.1) accompany each export batch.
For projects in seismically active regions (e.g., Chile, Peru, California, Japan), our engineers apply the local design response spectra (such as NCh 2369 or ASCE 7). We thicken the footplate weldments, upgrade chemical shear anchor specifications (M12 to M16 Hilti/Fischer anchors), incorporate diagonal cross-bracing in the rear plane, and add top spine ties to eliminate systemic structural twisting during ground acceleration.
For standard interior warehouses, our automated electrostatic line applies 60–80 microns of epoxy-polyester thermoset powder cured at 200°C. For deep-freeze warehouses operating at -25°C to -30°C where moisture condensation is persistent, or open-air marine ports, we provide hot-dip galvanized steel components conforming to ASTM A123 / ISO 1461, guaranteeing lifetime corrosion resistance.
Selective Racking represents the lowest initial capital cost ($25–$45 per pallet position) but utilizes only 40% of the warehouse volume due to wide aisle requirements (3.0m–3.5m). Radio Shuttle racking requires a higher upfront cost ($90–$160 per position, including automated cart units), but achieves over 80% volume density, slashing refrigerated power consumption and building lease expenditure.
With a dedicated monthly fabrication volume exceeding 30,000 metric tons, standard 40HQ full-container orders (FCL) of selective or drive-in racking are fabricated within 14 to 25 calendar days after CAD shop drawing approval. Large-scale distribution center projects exceeding 50 containers are dispatched in scheduled rolling batches to match civil engineering construction milestones.
Heavy upright frames and beams are bundled with dedicated protective cardboard corner wraps, multi-layer stretch shrink film, and heavy-duty polyester strapping. Components are loaded into 40ft High Cube (40HQ) containers utilizing specialized mechanical dollies to optimize both total gross payload (up to 26–28 metric tons) and container cubic volume while preventing transit abrasion.
Multi-tier mezzanine platforms generate concentrated point loads through baseplates that must not exceed the concrete slab's punch-shear resistance (typically 200–250mm reinforced concrete with 25–30 MPa compressive strength). HEDA Shelves provides customized oversized baseplates (e.g., 300x300x12mm or larger) to redistribute localized point stresses safely across your existing slab without cracking.
Forklift operators occasionally catch pallet corners on the underside of beams while lifting. Each beam-to-column connection in our systems features spring-action or gravity-drop galvanized steel safety lock pins that withstand an upward shear force of over 5.0 kN. This mechanically locks the claw connector into the column slot, preventing accidental vertical disengagement.
We provide complete project submittal packages including 2D architectural CAD layouts, 3D structural perspective renderings, bill of materials (BOM), load distribution calculation certificates, Mill Test Reports (MTC 3.1), CE Declaration of Conformity, and structural assembly guidelines. These enable your local civil engineer to endorse municipal building permits swiftly.
Plan Your High-Density Warehouse with HEDA Structural Engineers
Submit your building dimensions, pallet load requirements, and forklift specifications. Our engineering office delivers an accurate 3D CAD layout, finite load calculations, and a transparent FOB/CIF pricing quote within 24 business hours.