- 25+ YearsChemical rack engineering
- 30,000 t / moHigh-precision steel throughput
- CE & ISO 9001Audited production reliability
- 10,000+ ProjectsDeployed across 120+ countries
Chemical Storage Racking Systems: High-Performance Configurations
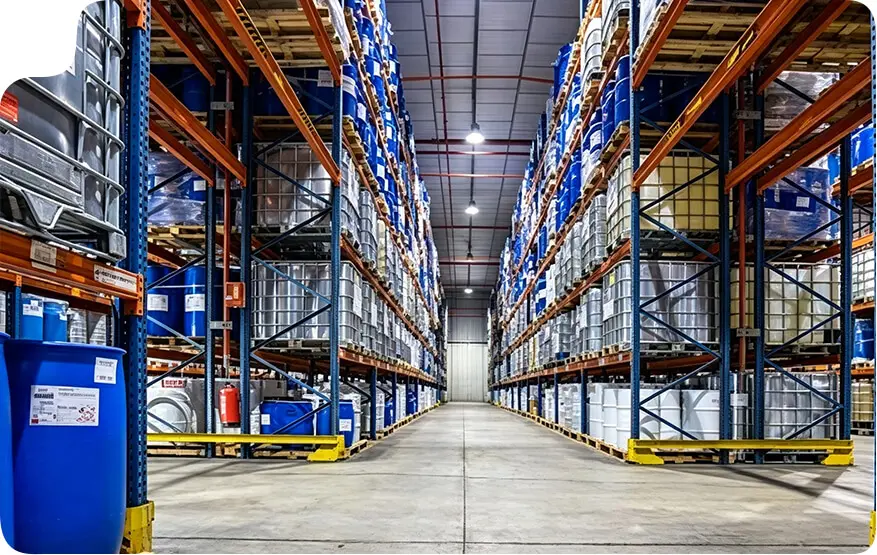
Selecting an industrial chemical storage racking system requires balancing chemical hazard classifications, secondary spill containment volumes, flammability segregation, and inventory accessibility. Guangzhou Heda Shelves Co., Ltd. customizes heavy-duty structural steel systems to mitigate volatility and maximize operational throughput.
Bunded Selective Chemical Racks
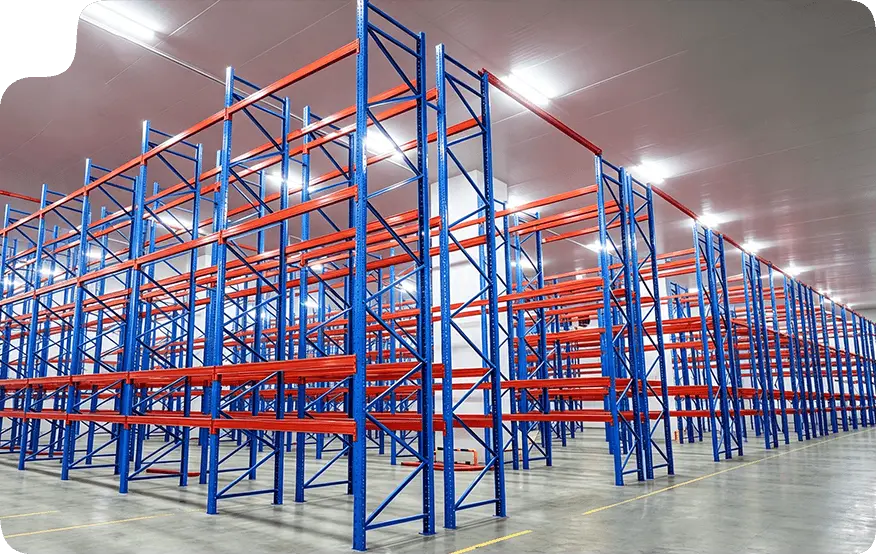
Designed for fast access to disparate chemical SKUs. Features integrated galvanized drip trays, drum chocks, and in-rack sprinkler clearance.
Inquire Now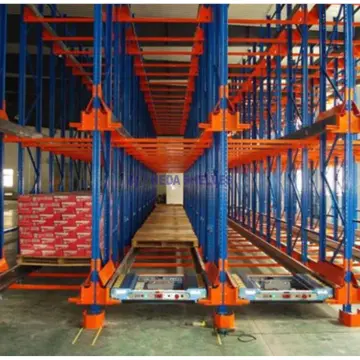
Explosion-Proof Radio Shuttle
Eliminates forklift traffic inside hazardous volatile vapor bays. Deep-lane automated shuttle carriers engineered with anti-static and spark-proof finishes.
Inquire Now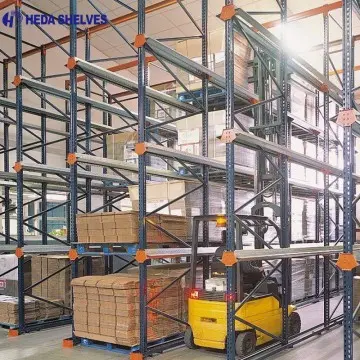
Drive-In Chemical Drum Racking
Ultra-dense storage for large batches of non-reactive raw chemical liquids, pigments, and resins. Configured with heavy floor rails and column impact guards.
Inquire Now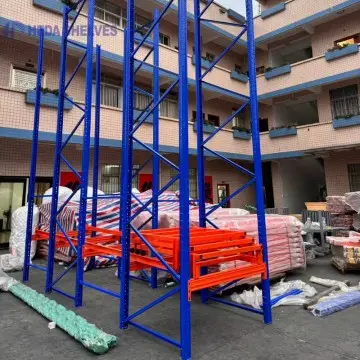
Heavy-Duty Push Back Chemical Racks
Nested rolling carts handle 2 to 5 pallets deep per lane. Ideal for temperature-regulated flammable liquid bunkers where storage cubic cost is extreme.
Inquire Now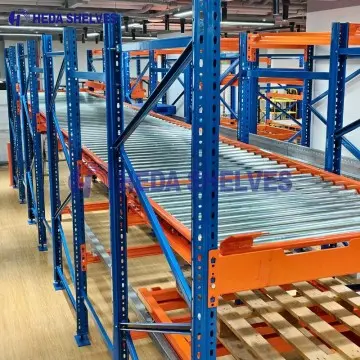
Gravity Chemical Flow Racking
Essential for active catalysts, polymers, and shelf-life constrained agrochemicals. Magnetic speed controllers prevent drum impact collisions.
Inquire Now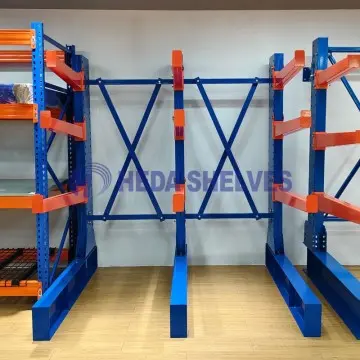
Chemical Cantilever Racks
Engineered storage for compressed gas cylinders, corrosion-resistant conduits, chemical dosing piping, and high-pressure flex tubing up to 3,000 kg per arm.
Inquire Now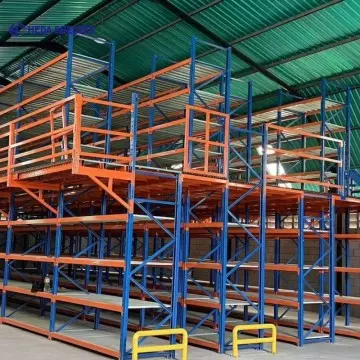
Rack-Supported Chemical Mezzanine
Integrates ground-level bulk drum storage with elevated secondary sampling suites, batch staging decks, and safety eyewash corridor zones.
Inquire Now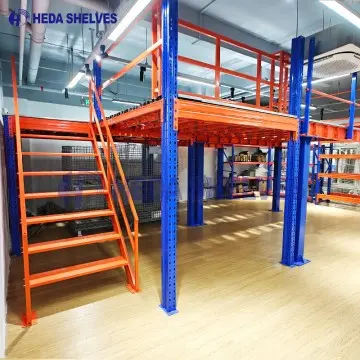
Structural Hazmat Platform
Custom-engineered structural I-beam platforms accommodating acid tanks, blending machinery, and heavy testing apparatus up to 1,500 kg/m².
Inquire NowEngineered Chemical Racking Precision Since 2001
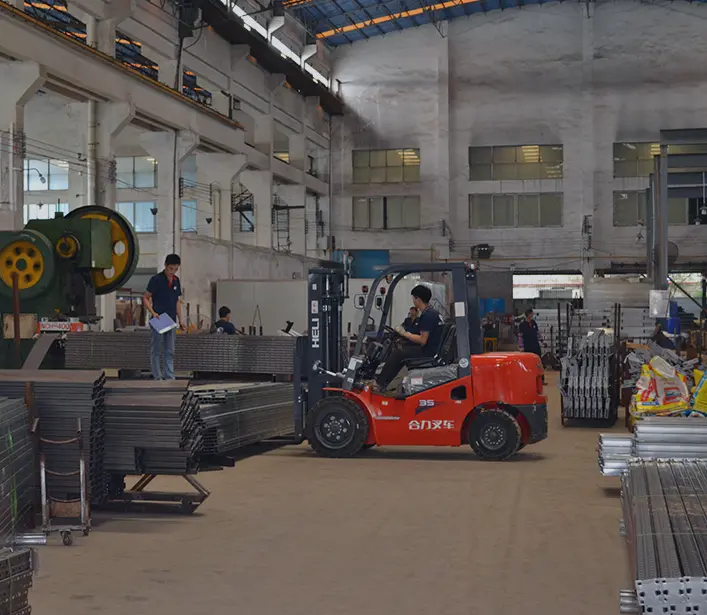
Guangzhou Heda Shelves Co., Ltd. stands as a premier manufacturer of industrial warehouse storage infrastructures, specializing in structurally validated, corrosion-resistant, and high-capacity chemical storage racking systems. Our modern 30,000 m² manufacturing plant houses more than 300 experienced technical designers, structural engineers, and skilled production specialists.
Chemical logistics demands non-negotiable structural integrity. A failure in a standard warehouse causes inventory damage; a structural failure in a chemical storage warehouse can cause catastrophic chemical spills, toxic ecological discharge, exothermic thermal runaway, or massive workplace fires. Guangzhou Heda Shelves Co., Ltd. engineers every chemical racking project from the ground up: calculating sloshing hydrodynamic liquid surge forces, accounting for seismic ground accelerations, executing 9-stage chemical pickling and phosphating, and applying dense epoxy powder coatings or ISO 1461 hot-dip galvanizing to resist the harshest volatile fumes.
- Compliant with NFPA 30, OSHA 1910 & EN 15512
- Dynamic seismic & liquid surge load engineering
- In-house 9-stage chemical pickling & epoxy coating
- Direct export to 120+ countries with complete CAD/3D plans
Future Procurement Trends in Chemical Storage Racking
As chemical logistics confronts increasingly stringent environmental oversight, higher land lease costs, and severe workplace safety regulations, international procurement teams are moving away from generic pallet racking toward specialized, engineered hazmat storage architectures.
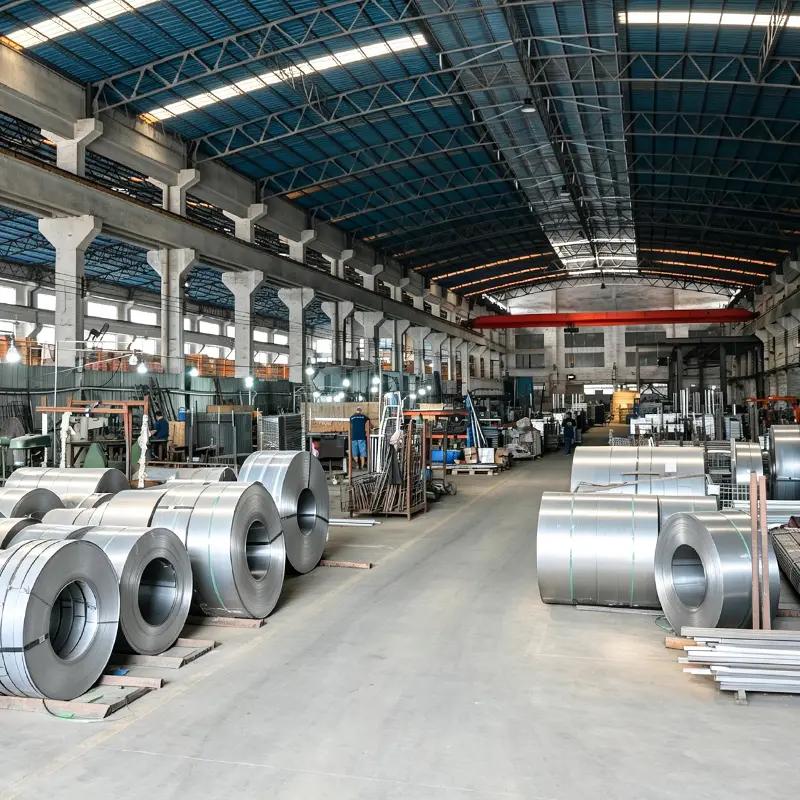

1. Integrated Spill-Containment Sumps
Global regulatory bodies (OSHA, EPA, REACH) now penalize uncontained hazmat tiers. Procurement is shifting rapidly toward racks featuring built-in galvanized catch-basins, poly sumps, and modular fluid divert channels capable of holding 110% of single IBC container failures.
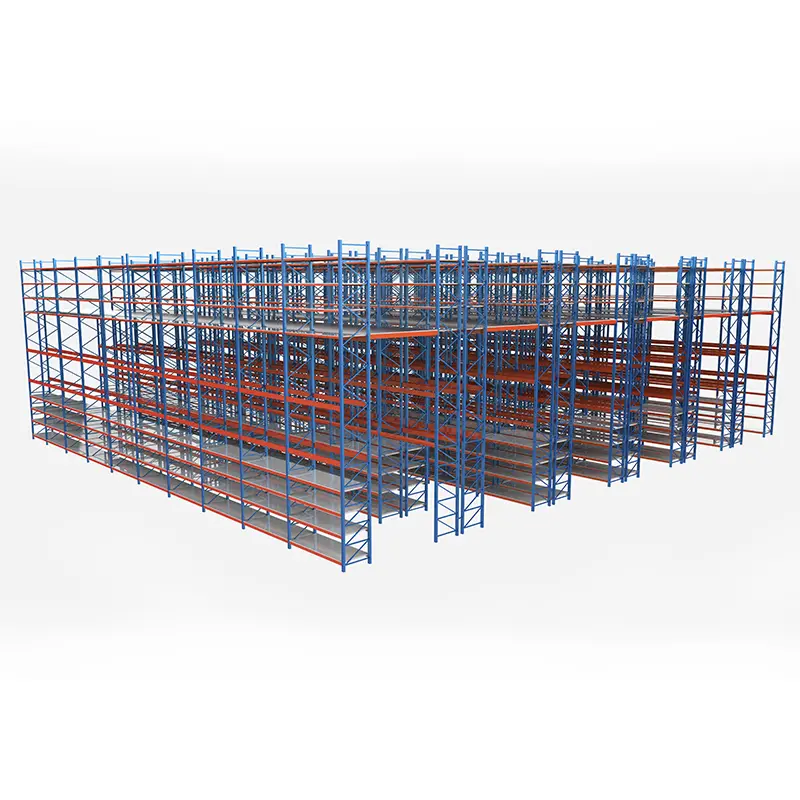

2. Sloshing Load Seismic Engineering
Liquid chemical drums and IBC totes exhibit resonant wave motion during seismic tremors. Next-generation chemical rack tenders require finite element analysis (FEA) factoring in hydrodynamic liquid sloshing coefficients, heavy floor baseplates, and oversized ductile column bracing.
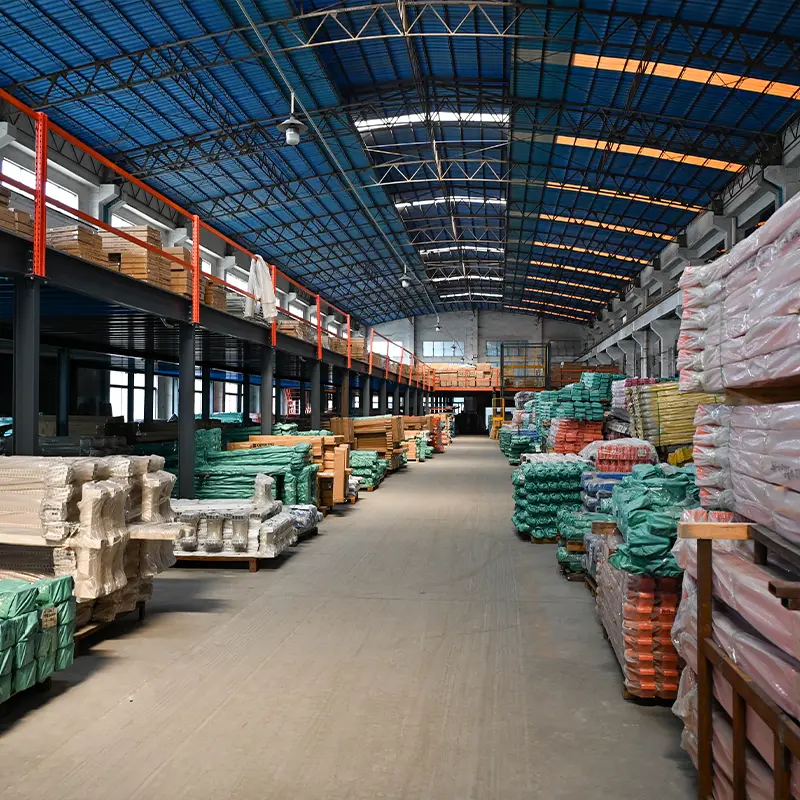

3. Extreme Anticorrosion Metallurgy
Standard architectural powder coating fails within months under acid mist or chlorinated solvent exposure. Buyers now demand dual-layer barrier systems: hot-dip galvanization beneath thermo-cured epoxy powders or high-grade 316L stainless steel contact pads at all friction points.
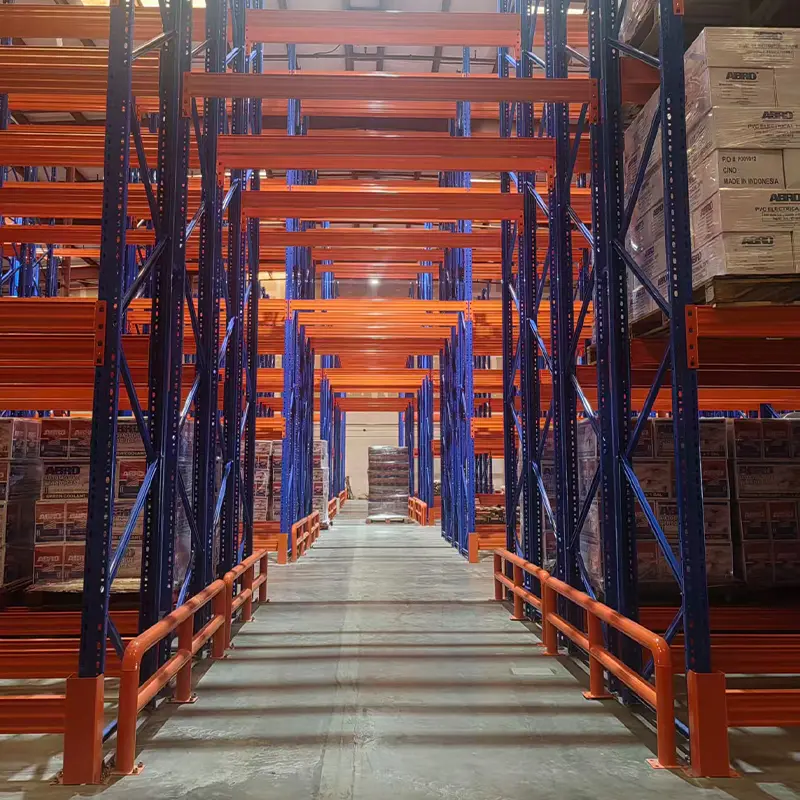

4. Human-Exclusion Automation
Chemical warehouse operators are transitioning from manual reach trucks to automated high-density radio shuttle and mini-load crane systems. Keeping forklift drivers out of toxic and explosive zones radically decreases insurance premiums, dropped drum events, and respiratory liabilities.
Technological Trajectory of Hazmat Racking Systems
The convergence of industrial automation, smart structural sensing, and stringent environmental stewardship is redefining chemical warehouse equipment. Guangzhou Heda Shelves Co., Ltd. pioneers these engineering advancements across our turn-key manufacturing portfolio.
- 01 IoT Strain Gauges & Structural Health Monitoring: Modern chemical rack uprights are integrating embedded fiber-optic load cells and ultrasonic strain sensors. In high-density IBC tote warehouses, real-time telemetry alerts facility managers to beam deflection anomalies or floor subsidence before mechanical stress leads to rack collapse.
- 02 ATEX/IECEx Certified Autonomous Material Handling: High-density shuttle carriers engineered with sealed brushless motors, spark-free bronze wheels, and intrinsically safe lithium iron phosphate battery enclosures now operate reliably inside Class 1, Division 1 flammable chemical environments.
- 03 Modular In-Rack Deluge & Vapor Sniffer Ducts: Forward-thinking chemical racking integrates pre-punched structural column channels designed specifically for rapid in-rack ESFR sprinkler drop pipes and aspirating smoke/vapor detection tubes, ensuring fire suppression activates directly at the localized drum tier.
10 Factory Steps Guaranteeing Hazmat Racking Reliability
Every beam, upright frame, and secondary containment basin undergoes full in-house production control at Guangzhou Heda Shelves Co., Ltd. We eliminate outsourcing compromises to guarantee structural performance.
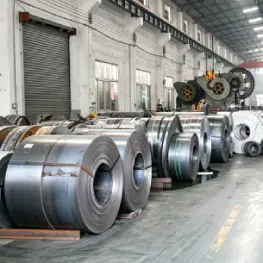 01
Mill-Certified Q235B/Q355B Steel
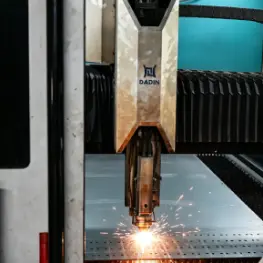 02
High-Accuracy Precision Cutting
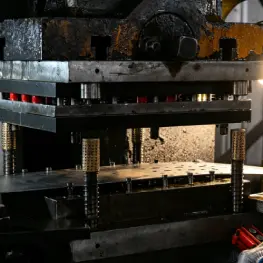 03
Automated CNC Punching
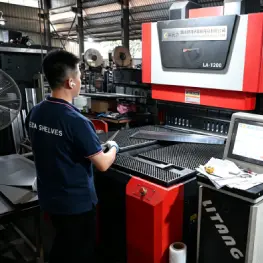 04
Heavy Cold Bending
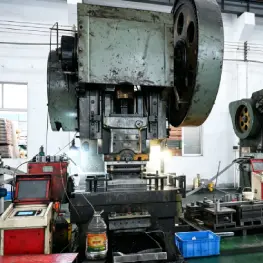 05
Continuous Roll Forming
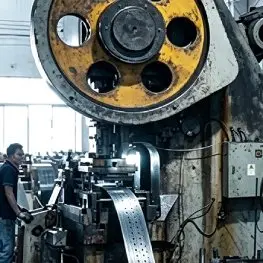 06
Precision Edge Deburring
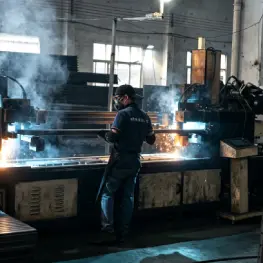 07
Robotic Shielded Welding
 08
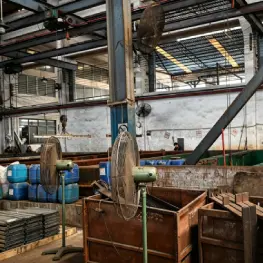
Acid Pickling & Phosphating
 09
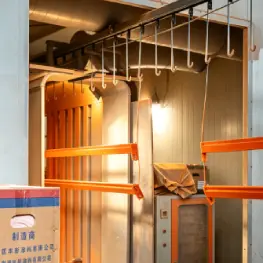
Corrosion-Resistant Coating
 10
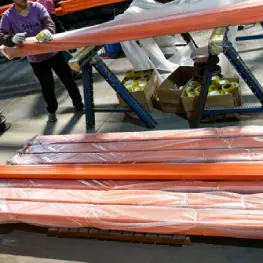
Deflection QC & Export Packing
International Certifications for Audited Industrial Safety
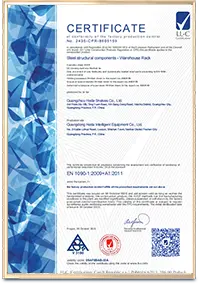
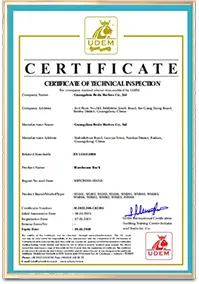
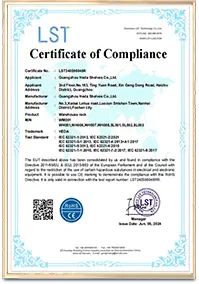
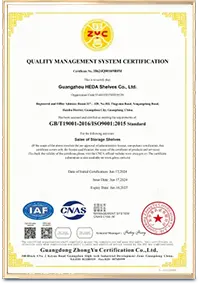
Industrial chemical warehouses require meticulous safety documentation for fire marshals, insurance underwriter certifications, environmental ministry inspectors, and local building councils. Guangzhou Heda Shelves Co., Ltd. provides certified structural calculations, certified material test reports (MTR), and internationally recognized factory credentials.
- CE Certified · Construction Products Regulation EN 1090 / CPR-8605159
- ISO 9001:2015 · Certificate No. 18624Q00169R0M · Audited Structural Quality
- RoHS & REACH Compliant · Non-toxic, environmentally stable powder coating


Global Brands Trusting Guangzhou Heda Shelves Co., Ltd.

Chemical & Heavy Industrial Installations Across the World
Review how Guangzhou Heda Shelves Co., Ltd. resolved intricate chemical containment, high load capacity, and aggressive environment challenges worldwide.
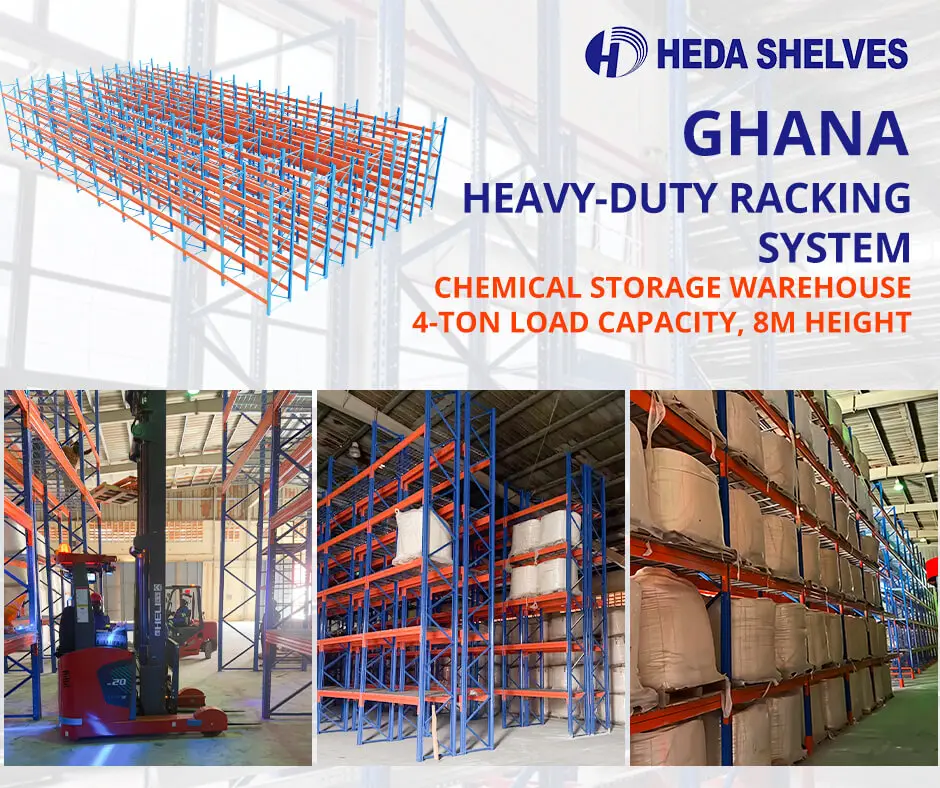
Heavy-Duty Racking System for Chemical Distribution
Engineered 3,500 kg per level pallet racking with integrated galvanized drip decks and seismic footing for an international chemical formulation facility.
Inquire Case Details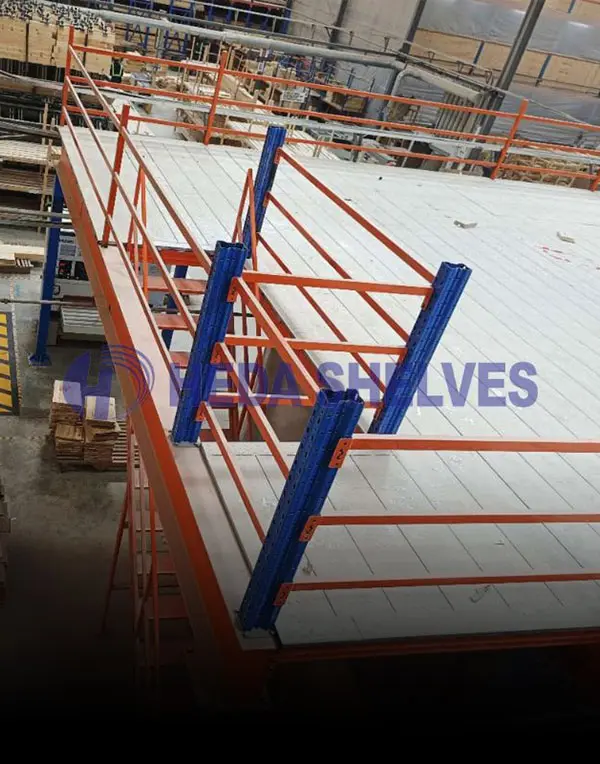
Cart-Loaded Push-Back Racks for Hazardous Solvent Drum Hub
Deep lane 4-tier push-back storage boosting drum storage density by 68% while separating incompatible solvent classes safely.
Inquire Case Details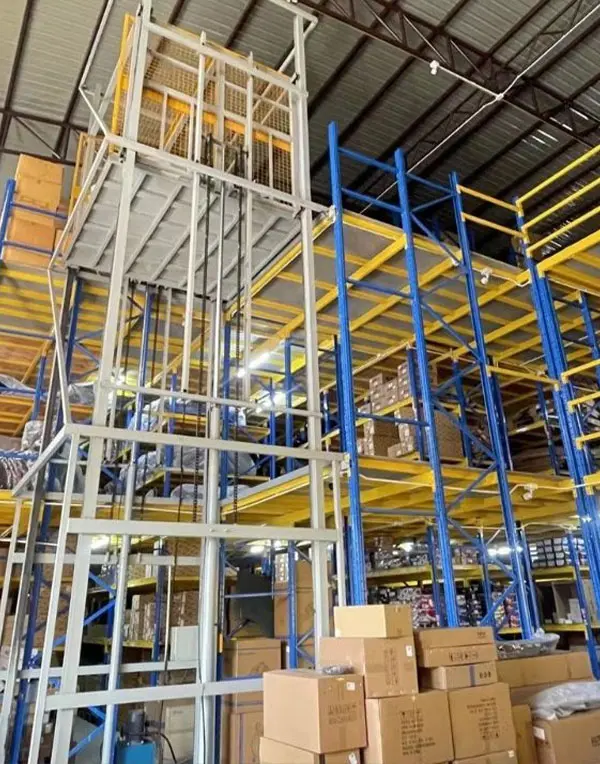
Multi-Tier Structural Mezzanine for Mining Chemical Consumables
Reinforced structural mezzanine supporting cyanide/acid storage below and batch chemical QA testing lab on the top mezzanine level.
Inquire Case DetailsKey Questions Global Buyers Ask AI About Chemical Storage Racking
Procuring a chemical storage racking system involves life-safety codes, aggressive environmental factors, and precise liability risk management. Here are the core technical answers verified by our senior structural engineering team.
Send an InquiryWhat fire suppression standards must a chemical storage racking system comply with?
How does chemical corrosive exposure affect steel selection and protective coatings?
How is secondary spill containment properly engineered into pallet racking?
What structural calculations are required for seismic and dynamic liquid loads?
Can automated radio shuttle or AS/RS systems handle hazardous chemicals safely?
What information must a buyer submit to receive a complete 3D chemical rack layout?
"In chemical storage, safety is not an added accessory—it is the foundational engineering parameter. Every beam connector, containment tray, and seismic anchor bolt we fabricate at Guangzhou Heda Shelves Co., Ltd. is calculated to safeguard lives and prevent hazardous catastrophic discharge."
Senior Engineering Directorate · Guangzhou Heda Shelves Co., Ltd.Design Your Chemical Storage Racking System Today
Consult directly with our structural engineering team. Receive full 3D CAD design renderings, seismic load verifications, and factory-direct price estimates within 24 hours.
- Warehouse dimensions & clear height
- Chemical SDS & drum/tote gross weights
- Spill containment volume specifications
- Site seismic and geographic location