Engineered Warehouse Racking & Structural Solutions
Explore heavy-duty, factory-direct storage configurations designed for third-party logistics, cold storage, and distribution facilities across the United Kingdom.
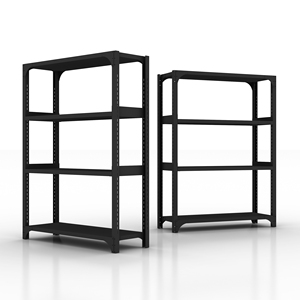
Cheap Metal Light Duty Rack & Steel Pallet Racking
Multi-tier modular light-duty steel shelving suitable for urban picking, retail stockrooms, and parcel staging.
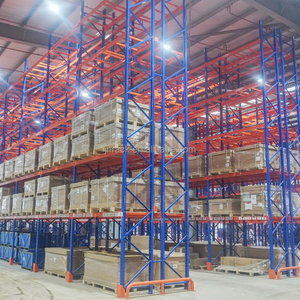
Heavy-Duty Corrosion Protected Pallet Racking Systems
Treated with phosphating and electro-coating, designed for cold chain environments and unheated Thames-side hubs.
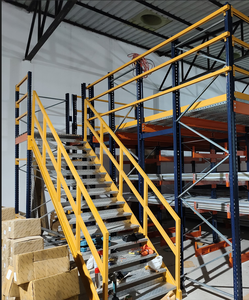
Heavy-Duty Steel Mezzanine Pallet Rack System
Integrated mezzanine and drive-through rack structures engineered to double usable cubic footprint under restrictive ceiling heights.
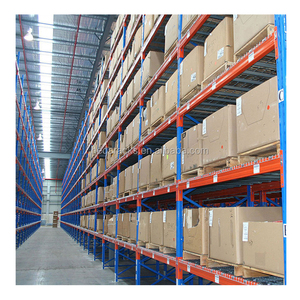
Metal Warehouse Shelf Heavy Duty Racks
High-tensile beam and upright structural framework built for bulk SKU storage and high turnover FMCG fulfillment.
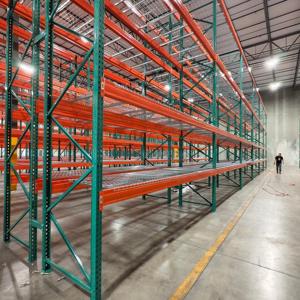
Heavy Duty Teardrop & Universal Pallet Racking
Standardized interlocking design compatible with existing industrial racking profiles, speeding up expansion projects.
Industrial Column-Free Steel Structure Warehouses
Engineered structural portal frames providing expansive unhindered floor clearance for ultra-dense drive-in lanes.
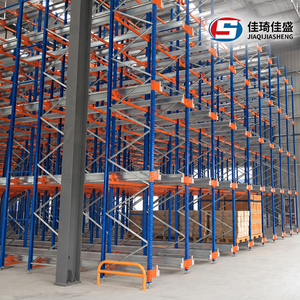
Two-Way Radio Shuttle Automated Racking System
Semi-automated deep lane shuttle system maximizing throughput while preventing mast collision inside cold storage channels.
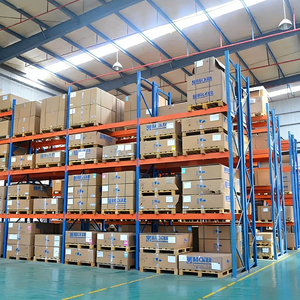
Multi-Purpose Heavy Duty Industrial Storage Racking
Customizable upright profiles engineered for dynamic loading, compatible with UK standard perimeter safety barriers.
Engineering OEM/ODM Drive-In Systems for London’s High-Density Requirements
As industrial real estate valuations across Greater London reach record levels—particularly within critical transport nodes such as Park Royal, Dagenham, Dartford, and Enfield—supply chain directors are under mounting pressure to achieve maximum cubic utilization per square metre. A standard selective racking configuration often allocates up to 60% of available floor space entirely to working forklift aisles. In contrast, an engineered Drive-In Pallet Racking System eliminates conventional operating lanes, consolidating up to 80% of open airspace into active pallet positions.
Operating primarily on a First-In, Last-Out (LIFO) material handling principle—or First-In, First-Out (FIFO) when designed as a continuous Drive-Through matrix—this system allows counterbalance or reach trucks to drive directly into structural storage lanes. Pallets rest on continuous cold-formed load rails supported by heavy-duty cantilevers attached directly to the main upright frames. Because forklifts operate internally, structural tolerances must account for horizontal dynamic impacts, frame racking, and vertical load eccentricities governed by stringent British and European structural standards.
| Structural Component | Standard Technical Specification | Engineering Margin / London Market Options |
|---|---|---|
| Cold-Rolled Upright Steel | Q235B / Q355B structural steel | Profile dimensions 90×65mm to 140×100mm, up to 3.0mm gauge |
| Load Rail Construction | Formed structural channel with integral lead-in guides | Galvanized or 70-micron electrostatic powder coating |
| Pallet Interface Compatibility | UK Standard 1200×1000mm & Euro 1200×800mm | Dual-flange pallet entry guides with safety end-stops |
| Compliance Standard | BS EN 15512:2020 & SEMA Codes of Practice | Third-party verified FEA structural calculation package |
| Impact Protection Package | Heavy-duty column guards & floor-mounted guidance tracks | Continuous 10mm high-yield floor-anchored steel angle guide |
Localized Industrial Application Scenarios Across London & South East England
Optimizing warehouse logistics within the M25 boundary requires systems adapted to stringent operational profiles, non-standard building heights, and fast-moving inventory. Our OEM/ODM manufacturing facility engineers drive-in structures specifically configured for regional facility topologies:
Urban Consolidation Centres (UCC)
London’s Ultra Low Emission Zone (ULEZ) has accelerated the need for multi-tier micro-consolidation facilities in Hayes, Croydon, and Barking. Drive-in racks accommodate bulk intake of homogeneous fast-moving consumer goods (FMCG), holding inventory in dense blocks before redistribution via light electric commercial vehicles.
Cold Storage & Temperature-Controlled Hubs
Refrigerated cubic volume in Park Royal and Bermondsey carries the highest industrial rents in the UK. Drive-in systems consolidate frozen meat, seafood, and fresh produce lines, minimizing the total volume of chilled air that must be mechanically conditioned, cutting facility energy overhead by up to 35%.
Thames Gateway 3PL Distribution Facilities
Large-format Third-Party Logistics centers situated along the A13 and M25 river corridor store seasonal buffers, bulk packaging supplies, and industrial raw materials. Drive-in configurations yield massive depth per bay (6 to 10 pallets deep), delivering maximum capacity across uniform manufacturing runs.
London Logistics Real Estate: Drivers Shaping Racking Architecture
Procurement teams and warehouse designers in the UK must balance structural investment against rapid systemic shifts in commercial property leasing, decarbonization directives, and automated logistics:
Skyrocketing Land Rents & Urban Densification
With prime London industrial yields driving rents past £25-£30 per square foot, new developments cannot expand outward. Warehouse operators are converting obsolete, low-clearance units into ultra-dense storage facilities, demanding custom-height upright fabrication and sub-millimetre clearance tolerances.
Integration of Semi-Automated Shuttles
Health and Safety Executive (HSE) directives continue to emphasize operator welfare. London distribution hubs are retrofitting conventional drive-in frames with two-way radio shuttles, preventing forklift trucks from penetrating deep lanes, thereby reducing upright damage rates by over 70%.
Decarbonization & Embodied Carbon Scrutiny
Institutional developers across the UK now audit the embodied carbon of steel infrastructure. Our factory employs precision coil roll-forming techniques, reducing scrap rates to under 1.5% while using low-VOC electrostatic powder systems to assist end-users in achieving BREEAM Excellent warehouse ratings.
Why London Importers & Contractors Partner With Our Manufacturing Base
As an integrated OEM/ODM manufacturer with 25+ years of specialized engineering experience, Guangzhou Heda Shelves Co., Ltd. operates a 30,000 m² state-of-the-art manufacturing plant producing over 30,000 tons of structural steel storage systems each month. We eliminate multi-tiered trading layers, providing direct factory communication, fully documented structural safety files, and dependable export operations for UK engineering firms and direct end-users.
SEMA & BS EN 15512 Compliance
Fully compliant with British SEMA guidelines and European standards, complete with comprehensive calculation documentation and verified load rating data plates.
Complimentary 3D CAD & BIM Modeling
Our in-house design engineering office delivers accurate 2D CAD floor plans, 3D clearance simulations, and BIM objects within 24 to 48 hours of initial enquiry.
Factory Direct End-to-End Control
Raw coil testing, automated continuous CNC punching, cold-roll forming, robotic welding, and shot blasting under strict ISO 9001:2015 quality surveillance.
Direct London Container Shipments
Optimized 40ft High Cube container load planning delivered directly to London Gateway, Port of Felixstowe, or Southampton with zero shipping-transit damage.
Frequently Asked Questions: Sourcing Drive-In Racks for the London Market
How does your drive-in racking comply with UK SEMA guidelines?
All upright columns, baseplates, cantilever arms, and structural portal bracing are calculated in accordance with BS EN 15512 (Steel static storage systems). We provide project-specific structural load notices, maximum safe working loads (SWL) for individual levels, and complete anchor pull-out test reports to satisfy local building control and insurance assessors.
Can the system accommodate both UK standard and Euro pallets?
Yes. We manufacture custom continuous support rails with adjustable lane widths. Our dual-entry configurations handle UK standard 1200×1000mm four-way wooden pallets along the 1200mm side, while allowing conversion or dual compatibility for Euro 1200×800mm pallets without structural instability.
What protection measures prevent forklift impact inside the drive-in channels?
Because truck masts enter deep lanes, we supply full floor-anchored steel guide rails (either continuous angle or heavy tubular steel). We also integrate heavy duty flared entry lead-in guides, wrap-around column protectors fabricated from 6mm structural plate, and high-visibility traffic yellow powder-coat finishes.
What is the typical ocean transit and lead time to London Gateway / Felixstowe?
Standard fabrication cycle runs between 14 to 25 working days following signed approval of CAD drawings. Ocean transit from our southern manufacturing hubs to London Gateway, Felixstowe, or Southampton takes approximately 24 to 32 days. Full Bill of Lading, Certificate of Origin, and detailed component packing lists are provided.
Upgrade Your London Logistics Facility With Direct OEM Engineering
Consult with our structural engineering desk. Send us your architectural site plan, slab capacity data, and pallet profiles for a complimentary 3D layout, load calculation, and comprehensive factory quote.
Inquire Now