Industrial Pallet Racking & High-Density Storage Solutions
Precision roll-formed Q235B and Q355B structural steel storage platforms, calculated to withstand high-volume forklift turnover, rigorous beam deflections, and site-specific seismic criteria across Victoria.
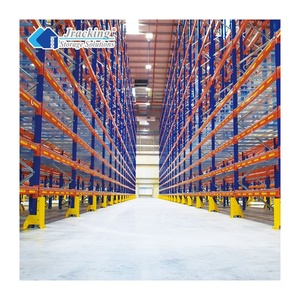
Jracking Steel Pallet Storage Racking
Precision-engineered adjustable steel shelving designed for international EURO and standard Australian pallet footprints in multi-tier logistics hubs.
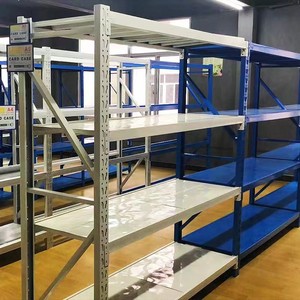
Metal Pallet Stacking Storage Racks
Flexible post-pallet stacking configurations tailored for dynamic warehouse storage, bulk seasonal overflow, and agile footprint redeployment.
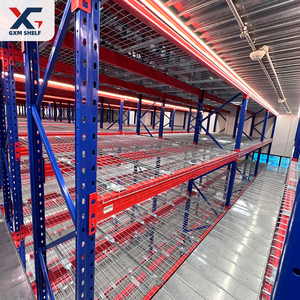
Heavy Duty Pallet Racking System
Multi-tier industrial racking built with high yield upright profiles, dynamic load safety locks, and high-impact column floor guards.
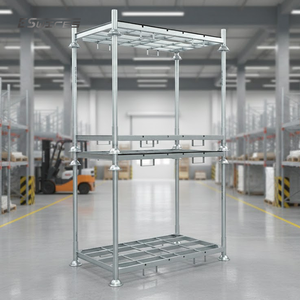
Cold Warehouse Post Pallet Rack
Galvanized structural steel and low-temperature electrostatic finishes engineered to resist condensation embrittlement down to -30°C.
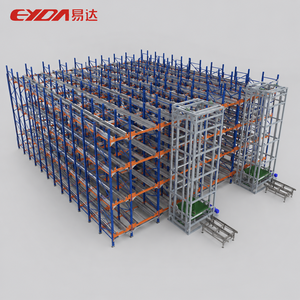
Automated Pallet Shuttle Racking
Semi-automated radio carrier system driving deep-lane FIFO/LIFO high throughput while eliminating internal forklift collisions in high-cube facilities.
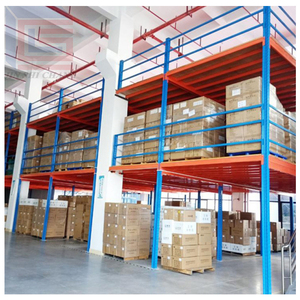
Heavy Duty Mezzanine Storage Platform
Integrated structural uprights supporting high-load overhead picking floors (300–1000 kg/m²), effectively doubling usable floor area without property leasing expansion.
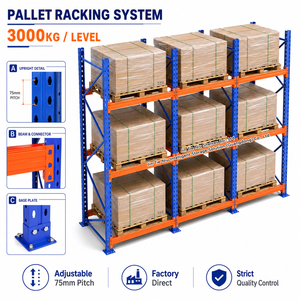
Selective Pallet Racking (3000KG)
Heavy structural box beams and 75mm pitch slotted uprights engineered to handle 3,000kg pallet pair levels with complete direct accessibility.
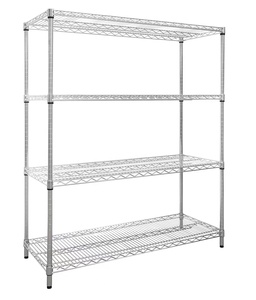
4-Tier Industrial Chrome Wire Shelving
NSF-certified open wire shelving capable of 800 lbs per tier, maximizing air circulation and light penetration for clean-room fulfillment and retail picking.
| System Architecture | Structural Profile | Unit Bay Capacity | Pitch Increment | Surface Finish Standard |
|---|---|---|---|---|
| Selective Pallet Racking | Cold Roll-Formed Omega Upright (Q235B/Q355B) | Up to 24,000 kg frame load | 75mm / 50mm adjustable | Electrostatic Powder Coated (60-80μm) |
| Radio Shuttle Racking | Reinforced High-Tensile Guidance Rails | 1,500 kg per pallet unit | Configured per pallet depth | High-Durability Epoxy / Pre-Galvanized |
| Structural Mezzanine Floor | Universal Beam (UB) / High-Yield Box Profiles | 300 - 1,200 kg / m² | Engineered custom spans | Hot-Dip Galvanized / Industrial Enamel |
| Cold Storage Systems | Low-Alloy Steel with Impact Toughness | Up to 3,500 kg / beam tier | 75mm adjustable | Continuous Hot-Dip Galvanization |
Engineering Storage for Melbourne's Strategic Freight Corridors
Warehouse lease rates across Greater Melbourne have intensified vertical density demands. From automated e-commerce hubs along the Western Ring Road to cold chain consolidation in Truganina, your racking architecture must maximize vertical cubic meter utilization while maintaining uncompromised safety.
West Melbourne Logistics Hubs
Operations across Truganina, Ravenhall, Laverton North, and Derrimut demand high-throughput selective and double-deep racking capable of managing fast container turns direct from the Port of Melbourne via the Footscray freight network.
South-East Cold Chain & Manufacturing
In Dandenong South, Braeside, and Moorabbin, food exporters, pharmaceutical companies, and precision manufacturers require moisture-proof, galvanized drive-in and radio shuttle platforms operating seamlessly inside low-temperature blast freezers.
Northern Industrial & Retail Infill
Campbellfield, Somerton, and Epping facilities leverage multi-tier rack-supported mezzanines to solve land scarcity constraints, facilitating dense SKU parcel sorting and omnichannel fulfillment within strict structural building perimeters.
Key Warehousing & Supply Chain Trends in Victoria
Navigating Victoria's commercial real estate pressures requires long-term capital efficiency, structural certifiability, and integration with advanced materials handling machinery.
Escalating Land Values & Clear-Height Optimization
With prime industrial warehouse rents throughout Melbourne maintaining premium baseline values, new design layouts prioritize 11m to 14.5m vertical clear heights. Facilities are moving toward Very Narrow Aisle (VNA) and automated shuttle architectures to squeeze 45% more storage volume from the exact same concrete footprint.
Stringent WorkSafe Victoria & AS 4084 Oversight
Regulatory scrutiny on structural warehouse safety has intensified. Operating companies now demand complete load rating signage, documented engineering sign-offs, dynamic impact base protections, and certified compliance with Australian Standard AS 4084:2023 for steel storage racking systems.
Shift to Direct Factory OEM Procurement
Forward-thinking warehouse directors and procurement heads are actively cutting out local middleman markups. Sourcing direct from certified manufacturing plants allows Victorian enterprises to secure customized profile steel, project-specific CAD engineering, and guaranteed batch quality at uncompromised economies of scale.
Precision Production Built Upon Certified Metallurgy
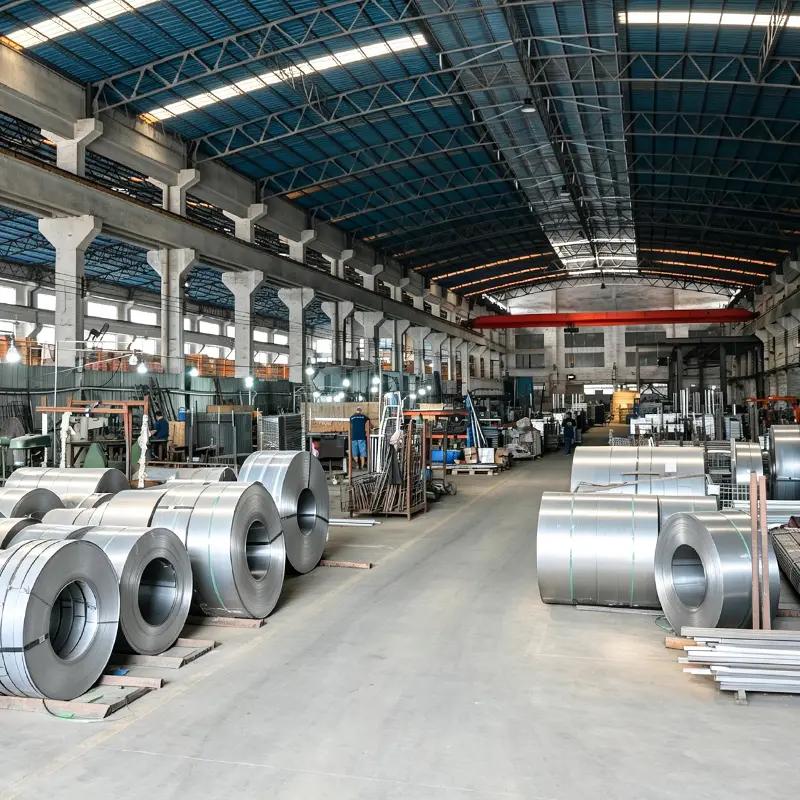
Since 2001, Guangzhou HEDA Shelves Co., Ltd. has operated as a world-class manufacturing authority for heavy warehouse storage systems. Operating from our 30,000 m² state-of-the-art production facility, every upright, beam, and structural bracing component passes through strict automated production lines, governed under ISO 9001:2015 quality assurance protocols and international CE standards.
We maintain end-to-end metallurgical control from raw coil slitting to our multi-stage anti-corrosion chemical wash, followed by automated robotic electrostatic powder application, ensuring long-term resilience against industrial warehouse operational abrasion.
Frequently Asked Questions by Victorian Warehouse Directors
Get immediate, clear answers to technical compliance, freight handling into the Port of Melbourne, engineering customization, and site assembly parameters.
Can your pallet racking and shelving systems be engineered to comply with Australian Standard AS 4084? +
Are your beam lengths and upright frame depths compatible with standard Australian CHEP & Loscam pallets? +
How do you ship and handle logistics into the Port of Melbourne (Swanson / Webb Docks)? +
What is the typical manufacturing lead time for standard and custom projects? +
How is mechanical installation handled on-site in Melbourne industrial estates? +
What information do you require to generate a free 3D CAD layout and structural quotation? +
Optimize Your Melbourne Warehouse Footprint Today
Partner directly with an established engineering manufacturer. Maximize your storage capacity, reduce your landed component costs, and acquire an AS 4084 compliant storage infrastructure built for heavy industrial duty.