High-Performance Certified Racking Systems & Warehouse Hardware
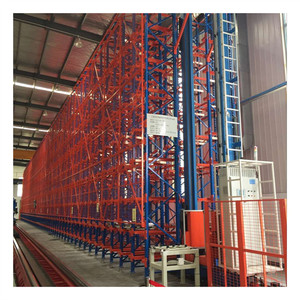
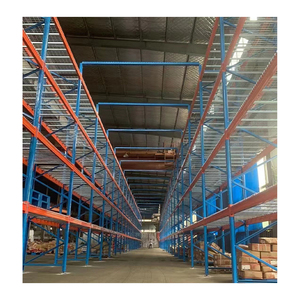
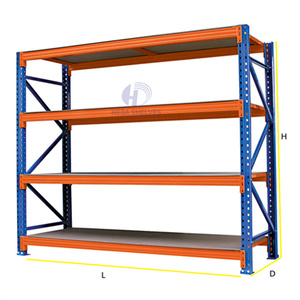
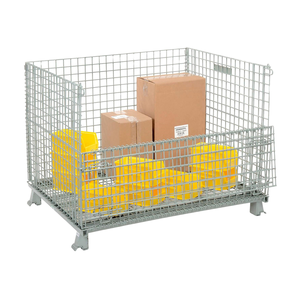
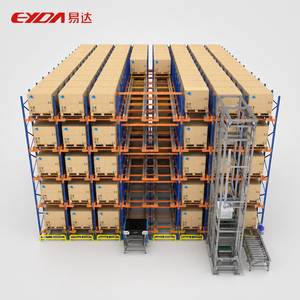
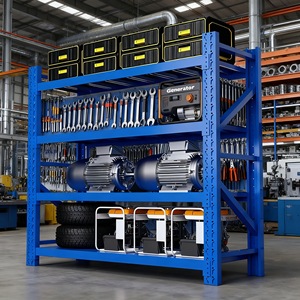
Explore our flagship heavy-duty storage configurations, high-density radio shuttle tracks, steel modular logistics warehouses, and warehouse accessories manufactured with certified Q235B and Q355B structural steel.
Engineering Standards: Structural Calculations, Steel Grades & Compliance
In heavy industrial warehousing, structural integrity is directly linked to regulatory compliance, personnel safety, and long-term asset security. Selecting certified steel racking requires evaluating cold-formed cross sections, connection stiffness, and seismic dynamic resilience.
European Normative (EN 15512:2020)
Our uprights and boxed beam assemblies conform to EN 15512 cold-formed thin-gauge structural design codes. Rigorous limit-state testing evaluates upright global buckling, flexural-torsional distortion, and semi-rigid beam-to-column connector lozenge tests to verify structural rotation stiffness and safety factors exceeding 1.4.
Material Science: Q235B vs. Q355B
We source prime hot-rolled strip coils tested for yield point, ultimate tensile strength, and cold-bend elongation. Critical high-bay columns utilize high-tensile Q355B steel (yield strength ≥ 355 MPa), lowering deadweight while augmenting load capacities up to 5,000 kg per level under strict L/200 deflection limits.
Seismic Design Verification
Operating in seismic zones requires specialized baseplate sizing, chemical wedge anchor calculations, and full vertical/horizontal bracing geometry. Our engineering calculations verify ductility and energy dissipation under Chilean NCh 2369, Peruvian E.030, and Colombian NSR-10 regional seismic parameters.
| Racking Architecture | Typical Bay Load | Max Clear Height | Stock Rotation | Floor Footprint Utilization | Ideal Industry Vertical |
|---|---|---|---|---|---|
| Selective Pallet Racking | 1,000 - 4,500 kg / Level | Up to 12.0 Meters | 100% Direct Access (FIFO) | 35% - 40% (Aisle Dependent) | 3PL, FMCG, E-Commerce Hubs |
| Radio Shuttle Automation | 500 - 2,000 kg / Pallet | Up to 24.0 Meters | FIFO or LIFO Selectable | 75% - 85% Ultra-Dense | Cold Storage, Beverage, Dairy |
| Drive-In Deep Lane System | 800 - 1,800 kg / Pallet | Up to 10.5 Meters | Strictly LIFO Mode | 60% - 70% Dense Block | Raw Commodity, Packaging Stacks |
| Heavy Duty Cantilever | 500 - 3,000 kg / Arm | Up to 9.0 Meters | Direct Crane / Forklift Access | 50% - 60% Open Linear | Steel Tubing, Timber, Extrusions |
| Multi-Tier Mezzanine Rack | 300 - 1,000 kg / m² Deck | Up to 3 - 4 Tiers | Manual Cart / Conveyor Access | 200% - 300% Multiplied Floor | Auto Spare Parts, Apparel E-Commerce |
Future Industrial Storage Procurement Trends: 2026–2030
Procurement directors and supply chain engineers must future-proof infrastructure investments. Shifts in labor dynamics, micro-fulfillment demands, real-estate costs, and environmental mandates are transforming industrial warehousing strategies globally.
1. Convergence on Semi-Automation
While fully autonomous AS/RS stacker crane towers require multi-million dollar outlays and multi-year commissioning schedules, semi-automated radio shuttle pallet systems offer a rapid ROI bridge. Shuttle systems triple pallet volume while reusing existing reach trucks, protecting capital expenditure against economic volatility.
2. Cold-Chain Volume Surge
Global demand for perishable foodstuffs, pharmaceutical biologicals, and fresh agro-export produce has made refrigerated cubic storage the most expensive real estate in supply chains. High-density racking with low-temperature ductile alloys (-30°C resistant) and galvanized roll-formed uprights avoids corrosion caused by freeze-thaw condensation cycles.
3. ESG & Low-Carbon Coating
Tier-1 multinational importers now audit their supply chain Scope 3 emissions. Modern manufacturers must implement closed-loop continuous shot-blasting, solvent-free epoxy-polyester electrostatic powder coating lines, and RoHS-compliant heavy-metal-free pre-treatments, eliminating VOC emissions while boosting corrosion endurance.
4. Modular Hybrid Footprints
Modern distribution centers no longer purchase standalone single-type pallet racks. Procurement specifications demand integrated hybrid layouts: ground-level carton flow lanes for order picking, heavy-duty selective rack overhead for buffer replenishment, and structural steel mezzanines for high-speed automated sorting conveyors.
End-to-End Quality Engineering: From Coil Slitting to Final Dispatch
Every structural column and boxed beam produced in our 30,000 m² production facility follows ten continuous, computer-monitored manufacturing milestones to eliminate weld spatter, micro-cracks, and dimensional variance.
Steel Coil Slitting
Certified Q235B/Q355B coils checked for chemical composition and slit to millimeter tolerances.
Automated Punching
High-precision 50mm / 75mm teardrop and diamond hole pitch stamping under continuous CNC monitoring.
Multi-Pass Roll Forming
18 to 24 roll-station cold forming machines fold rigid, ribbed multi-flange profiles without micro-fractures.
Robotic Laser Welding
Automated robotic weld cells bond connector claws to boxed beams with deep penetration and zero slag.
Pretreatment & Coating
Submersion pickling, phosphating rust inhibitors, and 180°C cured electrostatic powder polymer shield.
Guangzhou HEDA Shelves: 25 Years of Factory-Direct Excellence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates as a world-class manufacturing exporter equipped with heavy CNC profiling lines, robotic welding jigs, and an in-house team of structural engineers. We do not intermediate: you deal direct with engineers who understand bending moments, dynamic pallet loads, and international maritime packing.
-
Direct Factory Accountability (30,000 t / Month)
Large-scale continuous production enables stable pricing, rapid batch turnaround within 2–4 weeks, and absolute traceability from steel mill test certificates to final container dispatch.
-
Free Structural CAD & 3D Modeling Within 24 Hours
Submit your architectural CAD DWG or building layout. Our design team analyzes column spacing, sprinkler clearances, forklift aisle radii, and returns detailed 3D load simulation layouts.
-
Turnkey Export Container Load Optimization
Every shipment is packaged with numbered modular tags, protective film, and computer-calculated container stowage schemes that achieve 98% cubic space utilization while preventing freight damage.
Accredited Testing & Certifications
Verified compliance certificates ready for insurance underwriters, municipal building inspectors, and customs declaration clearance.
 CE 2435-CPR
 ISO 9001:2015
 Quality Bureau
 Load Test Proof
Frequently Asked Questions: Global Industrial Racking Procurement
Essential engineering, logistics, and quality assurance answers for procurement officers, logistics consultants, and warehouse facility directors.
What specific criteria validate a factory's CE Certification under EN 15512?
A legitimate CE marking for industrial storage requires compliance with European Regulation (EU) No 305/2011 for Construction Products (CPR) and standard EN 15512 (cold-formed steel storage systems). Our CE certificate (No. 2435-CPR-8605159) is issued by an accredited European notified body. It covers factory production control (FPC), periodic physical stub column testing, beam-to-column connector moment rotation curves, and shear stiffness calibration, ensuring legal compliance and insurable status for industrial facilities.
How do you calculate safe load capacity per pair of beams and avoid structural failure?
Beam load calculations follow limit-state design principles evaluating bending moment capacity and deflection criteria. Standard international guidelines require maximum deflection under design load not to exceed L/200 (length of beam divided by 200), with safety factors applied over the elastic limit. Additionally, every beam is secured to upright frames using certified safety locking pins withstanding a minimum 5.0 kN upward shear force to prevent accidental dislodgement from forklift tines.
What surface treatment best protects racking in coastal or sub-zero cold-storage facilities?
Standard dry ambient warehouses use our electrostatic epoxy-polyester powder coating (60–80 microns) applied after an automated 5-stage pickling, rinsing, and phosphating sequence. For coastal marine environments with elevated salinity or sub-zero food freezers (-25°C to -30°C) subject to thermal condensation, we supply hot-dip galvanized upright frames (HDG, coating thickness ≥ 55 microns conforming to ISO 1461) or sendzimir pre-galvanized components to prevent micro-corrosion pitting.
How does your engineering team support site-specific seismic calculations?
When clients supply their warehouse site location, soil profile class, and local seismic acceleration values (Ss and S1), our structural department calculates dynamic earthquake actions using response spectrum analysis. We adjust baseplate dimensions, anchor bolt grades (e.g., Grade 8.8 chemical or wedge anchors), column upright steel gauge, and back-to-back bracing geometry to conform with regional seismic codes such as Chile (NCh 433 / 2369), Peru (E.030), Colombia (NSR-10), or US RMI / ASCE 7.
What is the standard production lead time and ocean export loading workflow?
With an automated monthly throughput of 30,000 metric tons, standard 40ft high-cube container orders are completed in 15 to 25 calendar days following drawing sign-off. Beam bundles are separated with timber dunnage and strapped with steel bands, while upright frames are cushioned with multi-layer bubble wrap and shrink film. Components are marked with barcoded part labels matching installation assembly manuals, allowing local teams to execute rapid, error-free erection.
Request an Engineered Layout & Factory Price Matrix
Send your building dimensions, pallet specs, and lift equipment details. Our technical team delivers complete 2D/3D CAD layout schemes and formal quotation files within 24 working hours.