Factory Direct Gravity Fed & Industrial Storage Racks
Explore heavy-duty, certified industrial racking configurations precision-engineered for maximum storage density, strict First-In-First-Out (FIFO) material rotation, and structural longevity under demanding warehouse throughput.
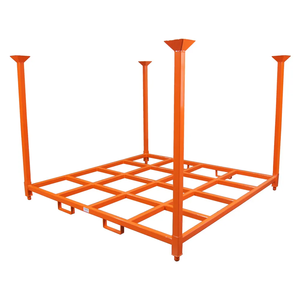
Factory Direct Inverted Metal Pallet Stack Rack
Tubular Subframe Carrier Pallet Platform Rack
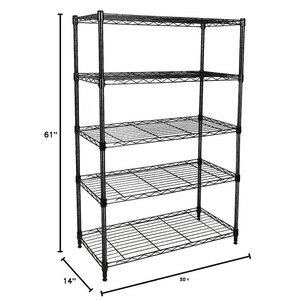
5-Tier 800lbs NSF Metal Chrome Wire Shelving
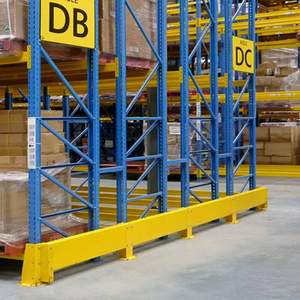
Warehouse VNA Heavy Pallet Racking System
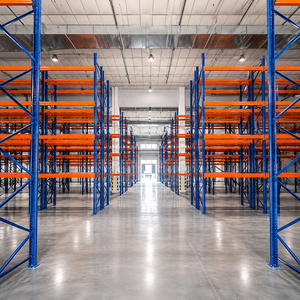
Heavy Duty 2000KG Level Steel Pallet Rack
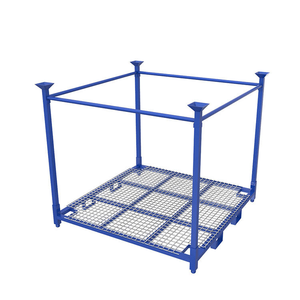
Commercial Metal Warehouse Pallet Tire Storage Rack
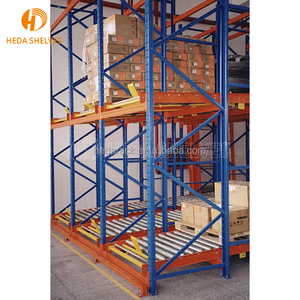
Industrial FIFO Gravity Carton & Pallet Flow Racks
Stainless Steel Pegboard Tool & Part Storage Shelf
Physics, Kinematics & Mechanics of Gravity-Fed Racking
Gravity-fed racking (encompassing Pallet Flow and Carton Flow systems) represents the pinnacle of passive, high-density warehouse throughput. Understanding the mechanical parameters is critical to avoiding pallet hang-ups, structural deflection, and uncontrolled runaway impacts.
In high-velocity distribution centers dealing with perishable food, pharmaceuticals, and high-turnover consumer goods, static selective racking consumes excessive aisle square footage. Gravity flow systems compress multiple storage aisles into a single deep-lane block, allowing loading on the replenishment side (charging face) and picking on the retrieval side (discharging face). The entire dynamic movement is driven solely by gravitational potential energy, eliminating electric drives, sensors, and continuous maintenance.
Critical Kinematic Equations in Gravity Racking Design
Designing a zero-failure gravity bed demands balancing the tangential component of gravity against the combined rolling resistance, bearing drag, and pallet bottom irregularities. The continuous descent velocity \(v\) along a roller incline with an angle \(\theta\) is governed by:
F_net = m × g × (sin θ - μ_r × cos θ) - F_brake
Where \(m\) represents gross pallet mass (typically 500 kg to 1,500 kg), \(\theta\) is the lane pitch (normally engineered between 2.5% and 4.0%), \(\mu_r\) is the rolling friction coefficient of the heavy-duty zinc-plated steel or polyurethane rollers, and \(F_{brake}\) is the resistive retarding force applied by centrifugal dynamic brake rollers. Without carefully spaced brake rollers, a 1,200 kg pallet traveling down a 30-meter lane would reach catastrophic terminal velocities exceeding 4.5 m/s, compromising structural uprights and operator safety.
Centrifugal Brake Rollers
Integrated internal planetary gearing with centrifugal friction shoes that engage proportionally to pallet speed, keeping lane velocity strictly regulated between 0.15 m/s and 0.30 m/s regardless of pallet load fluctuations.
Load Separator Mechanisms
Mechanical foot-pedal or pneumatic latches that isolate the front-most retrieval pallet from the rear accumulating queue, shielding forklift operators from thousands of pounds of line back-pressure during pickup.
Cold-Store Dynamic Rollers
Specially formulated low-temperature bearing grease and condensation-resistant galvanized tracks designed to operate flawlessly down to -30°C in blast freezers without roller seizure or surface icing.
Top 10 Gravity Fed Racking Manufacturers & Factories
A comprehensive review of the world's premier gravity flow and dynamic pallet racking manufacturers, ranked by production capacity, engineering integrity, international certifications, and global supply chain execution.
1. Guangzhou Heda Shelves Co., Ltd.
Top Direct OEM/ODM FactoryFounded in 2001 with a massive 30,000 m² state-of-the-art manufacturing campus in Guangzhou, China. HEDA Shelves produces over 30,000 tons of precision-engineered racking per month. Renowned for custom heavy-duty gravity pallet flow, carton live storage, and integrated multi-tier mezzanine racks. Features full seismic modeling, free 3D CAD design within 24 hours, and direct global export to over 120 countries.
2. SSI Schaefer Group
GermanyA global juggernaut in intralogistics and automated material handling. SSI Schaefer provides ultra-reliable live storage systems with high-end modular carton flow tracks and deep-lane pallet flow. Their systems are widely recognized in enterprise pharmaceutical and FMCG distribution centers where full ASRS integration is required.
3. Mecalux Racking Solutions
SpainOne of the dominant storage manufacturers in Europe and the Americas. Mecalux specializes in dynamic pallet flow channels utilizing dual-roller and full-width steel roller tracks. Their flow beds excel in dense buffer warehouses and order dispatch staging docks for high-turnover consumer goods.
4. Dexion (Gonvarri Material Handling)
Norway / GermanyOriginator of adjustable storage slotted angle racks, Dexion brings immense metallurgical authority to gravity live storage. Their carton flow beds feature ultra-durable plastic wheel tracks with aluminum framing for high-speed carton picking stations and assembly lines.
5. Interroll Group
SwitzerlandThe definitive global reference for gravity flow roller components, dynamic modules, and centrifugal speed controllers. While many rack builders construct the structural steel uprights, they frequently integrate Interroll's patented roller tracks, magnetic speed controllers, and time-delay pallet separators.
6. BITO-Lagertechnik Bittmann GmbH
GermanyRecognized European leader in small-parts live storage and piece-picking gravity racks. BITO excels in ergonomic carton flow shelves with drop-in track segments, adjustable lane dividers, and integrated pick-to-light bracket systems designed for zero-error fulfillment operations.
7. Ridg-U-Rak, Inc.
United StatesA premier North American heavy-gauge structural pallet rack manufacturer. Ridg-U-Rak is widely known for fabricating high-impact roll-formed and structural steel gravity flow racking systems that resist repetitive forklift abuse in beverage loading docks and cold stores.
8. Stow Group
BelgiumA fast-growing European intralogistics titan with extensive automated and dynamic racking production lines. Stow engineers high-bay dynamic pallet flow racks capable of reaching 25+ meters vertical heights with automated crane replenishment on the loading face.
9. Frazier Industrial Company
United StatesThe pioneer of 100% hot-rolled structural steel channel racking in North America. Frazier's gravity flow systems are essentially indestructible, engineered specifically for harsh environments such as sub-zero freezers and brutal heavy manufacturing facilities where roll-formed steel would buckle.
10. Apex Warehouse Systems
United StatesSpecialized warehouse engineering and custom flow rack fabricator. Apex offers custom full-roller, skate-wheel, and deep-lane pallet flow designs. They maintain dedicated in-house dynamic testing labs where client pallets are tested at full weight across simulated slopes prior to fabrication.
| Manufacturer | Primary Steel Grade | Speed Control Mechanism | Seismic Compliance | Lead Time (Standard) | Direct Export Capability |
|---|---|---|---|---|---|
| Guangzhou HEDA Shelves | Q235B / Q355B Cold-Rolled | Adjustable Centrifugal Brake Rollers | NCh 433, NSR-10, E.030, EN 15512 | 2–4 Weeks (30k Ton Cap.) | Worldwide / Port Delivery |
| SSI Schaefer | European Certified Coil | Centrifugal / Magnetic Gear | EN 15512, Eurocode 3 & 8 | 8–12 Weeks | Global Subsidiary Network |
| Mecalux | High-Elastic Micro-Alloy | Centrifugal Brake Assemblies | RMI MH16.1, EN 15512 | 6–10 Weeks | Direct / Regional Hubs |
| Dexion | High-Yield Structural Coil | Integrated Friction Rollers | FEM 10.2.02, SEMA | 6–9 Weeks | Europe, APAC, Americas |
| Interroll | Precision Drawn Tube / Polymer | Patented Magnetic / Gearless Regulators | Component Level EN Certified | 4–6 Weeks (Components) | Global OEM Distribution |
| Frazier Industrial | 50,000 PSI Hot-Rolled Channel | Centrifugal Hydraulic / Mechanical | AISC, RMI MH16.1 | 10–14 Weeks | North America Focused |
Future Procurement Trends in Gravity Storage (2026–2030)
Dynamic warehouse storage is undergoing rapid technological adaptation. Driven by labor constraints, cold chain expansion, and autonomous mobile robotics, procurement directors must evaluate five key market shifts before placing long-term capital investments.
1. AMR/AGV Interface Optimization
Forklift-free loading and discharging. Next-generation gravity flow beds feature self-centering entry funnels, precision optical stop plates, and magnetic damping rollers engineered to interface directly with Autonomous Mobile Robots (AMRs) without human intervention.
2. Telemetry-Enabled Roller Beds
Low-power IoT sensors embedded within flow track bearings monitor lane dwell time, identify stalled pallets, and measure internal bearing temperatures in refrigerated facilities, warning maintenance teams before catastrophic lane jams occur.
3. Hybrid High-Density Automation
Combining gravity flow with radio shuttles and automated stacker cranes. Flow beds act as multi-deep dispatch and staging buffers at cross-dock loading doors, creating ultra-fast buffer queues without the massive capital expenditure of fully powered conveyors.
Why Tier-1 Importers Partner with Guangzhou HEDA Shelves
With 25 years of engineering leadership, our 30,000 m² factory delivers direct manufacturing control, strict structural certifications, and comprehensive seismic design directly to international distribution hubs.
Certified Global Quality
Certified to CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 No. 18624Q00169R0M. Full structural compliance with international storage standards, including EN 15512 and RMI specifications.
30,000 Tons Monthly Capacity
Operating out of our fully owned 30,000 square meter factory staffed by 300+ technicians. We process up to 30,000 tons of structural steel monthly, ensuring large multi-container projects ship within 2 to 4 weeks.
Free 3D Layout & Seismic Calcs
Send our senior engineering team your warehouse architectural floor plans. We generate a full 3D layout, CAD drawing, and structural seismic load analysis tailored to your exact geographical site parameters within 24 hours.
10-Step Controlled Factory Workflow
To eliminate field defects and guarantee roller alignment down to the millimeter, every gravity rack, upright, and support crossmember passes through our in-house automated production line:
Raw Materials
Certified Q235B & Q355B coils verified for tensile yield strength.
Precision Cutting
CNC fiber laser and automated shear lines with 0.1mm tolerances.
Auto Punching
Multi-station automated hydraulic presses punch column pitch holes.
Cold Roll Forming
Continuous multi-pass roll forming mills craft reinforced uprights.
Robotic Welding
Automated MIG welding fixtures ensure uniform, ultra-high strength seams.
Surface Polishing
Automated shot-blasting removes scale, rust, and surface imperfections.
Phosphating Wash
Multi-stage chemical pre-treatment bath guarantees paint adhesion.
Powder Coating
Electrostatic automated powder booth bakes 60-100μm durable finishes.
Dynamic QA Test
Brake roller velocity and latch separation load verified in test lanes.
Export Crating
Steel banded, bubble-cushioned, and container-optimized load plans.
Gravity Fed Racking Procurement FAQ
Essential engineering answers to technical questions raised by supply chain directors, industrial architects, and warehouse operations managers.
How do you calculate the correct incline pitch for gravity pallet flow lanes? +
- Wood Euro pallets (smooth bottom runners): Typically require a 3.0% to 3.5% incline.
- Plastic or GMA pallets with bottom cavities: Require 3.5% to 4.0% incline and a three-track roller configuration to bridge gaps.
- Extreme light loads (<300 kg): Require a steeper incline (up to 4.2%) to overcome roller starting inertia.
- Heavy loads (>1,200 kg): Require 3.0% incline combined with centrifugal speed controllers spaced at every single pallet length.
Can your gravity flow racks be engineered for high seismic zones (Chile, Peru, California)? +
What happens if a pallet gets stuck halfway down a deep gravity lane? +
What is the maximum lane depth achievable in a gravity pallet flow system? +
How does electrostatic powder coating compare to galvanizing for cold storage and coastal warehouses? +
What minimum data is required to receive a complete 3D layout and formal quotation? +
- Warehouse architectural drawing (DWG or PDF) including clear ceiling heights, building columns, dock doors, and sprinkler clearance.
- Pallet dimensions (W × D × H) including overhang and gross weight (min/max).
- Bottom pallet runner direction and material (hardwood, softwood, plastic, metal skid).
- Forklift model, mast lift height, and turning radius clearance.
- Project site city/country (for local seismic coefficient calculations).
Request an Engineered 3D Layout & Factory Quote
Eliminate intermediate distributors and work directly with Guangzhou HEDA Shelves. Our engineering team delivers comprehensive CAD layouts, structural load calculations, and turnkey factory-direct container freight proposals within 24 hours.