Years Industrial Manufacturing (Est. 2001)
Monthly Cold-Rolled Steel Output
Certified In-House Engineers & Specialists
Global Projects Across 120+ Countries
Engineered Warehouse Racking & Heavy-Duty Storage Systems
Designed strictly under CE (2435-CPR-8605159) & ISO 9001:2015 frameworks to support high-density logistics, seismic safety standards, and corrosion-resistant intralogistics applications.
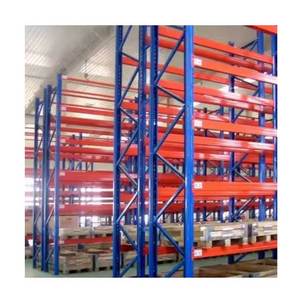
Industrial Heavy Duty Racks Pallet Racks Heavy Duty Warehouse Pallet Racking Manufacturing Companies OEM
100% selective accessibility system made with high-yield cold-rolled steel, adjustable 50mm/75mm beam pitch, and 1,000 to 5,000 kg capacity per level.
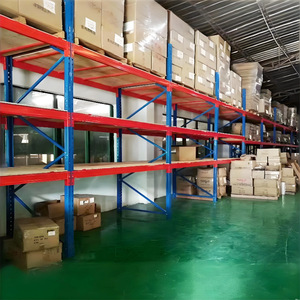
Heavy-duty Cold-rolled Steel Warehouse Racking Extra-Strong Load Capacity Thickened Construction Four-Layer Industrial Shelving
Thickened beam profiles and stiffened steel decks engineered for high-density multi-tier picking centers, raw materials, and assembly lines.
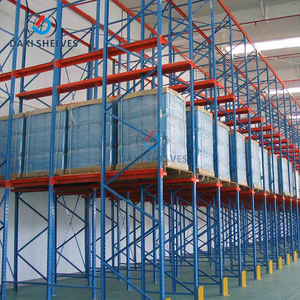
Automation Warehouse Drive-in Pallet Rack Warehouse Shelves Adjustable Pallet Racking Stacking Racks Warehouse Storage
Maximizes volumetric utility up to 80% by reducing forklift aisles; optimized for cold chain facilities, beverage depots, and batch manufacturing.
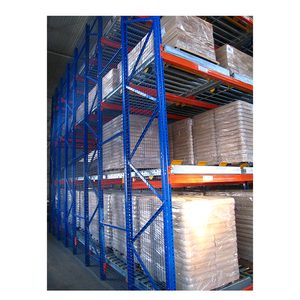
Factory Price Industrial Racking Warehouse FIFO Pallet Flow Rack Systems
Gravity-driven inclined roller lanes ensure strict First-In-First-Out (FIFO) stock turnover with automated speed brakes for perishable fulfillment.
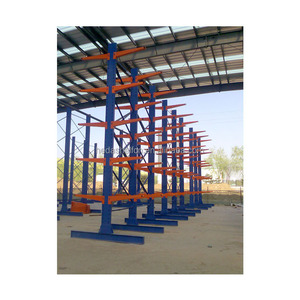
Double Sided Heavy Duty Cantilever Racking System Cantilever Racks Industrial Shelves Warehouse Racks
Unobstructed frontal design for oversized, elongated loads such as structural steel pipes, timber packs, plastic extrusions, and heavy sheet metal.
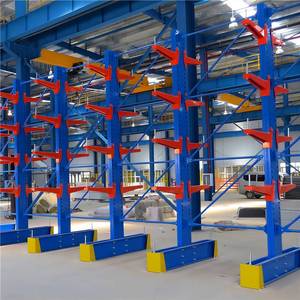
Storage Racks Wholesale Selling Heavy Duty Double Side Arm Storage Racks Warehouse Storage Industrial Cantilever Lumber Rack
Reinforced column base and taper-locked cantilever arms delivering load capacities over 3,000 kg per arm with optional retaining pins.
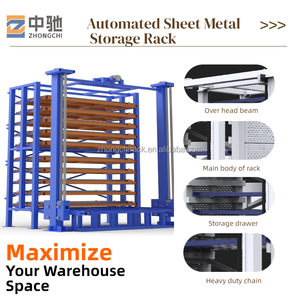
Automatic Warehouse Storage Rack System for Steel Sheet Heavy Duty Anti Rust Industrial Racking System Blue 1140x1140mm Pallet
High-tolerance vertical racking configured for stacker crane interface, automated guided vehicles (AGVs), and anti-rust electrophoretic treatment.
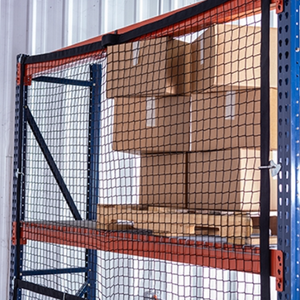
OEM ODM Customizable Strong Nylon Pallet Cargo Rack Net Rope Edge Pallet Rack Netting Securing Cargo Wrap Cutting Processing
High-tensile modular nylon safety netting designed to prevent overhead inventory shedding in high-bay structures and designated seismic zones.
The Global Procurement Shift: Heavy Industrial Warehouse Racking from China
In modern industrial logistics, warehouse racking has evolved far beyond basic metal framework. Today's global supply chain executives in North America, Europe, Australia, and South America view heavy-duty pallet racking as a critical infrastructure investment. Choosing an experienced China pallet warehouse racking manufacturer and exporter requires navigating rigorous structural engineering, metallurgical specifications, seismic resilience calculations, and factory-direct quality control.
Operating a 30,000 m² state-of-the-art production base established in 2001, Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) produces over 30,000 tons of precision-engineered racking monthly. Certified under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 (No. 18624Q00169R0M), we bridge the gap between competitive factory economics and strict international safety codes such as EN 15512, RMI, and regional seismic codes.
Core Technical Takeaway: Modern pallet racking design is primarily governed by limit state structural analysis. The transition from generic structural steel sections to specialized cold-rolled omega-profile uprights (Q235B/Q355B) allows for up to a 28% increase in vertical load-bearing capacity while lowering shipping tare weight for full-container ocean transport.
Future Procurement Trends in Industrial Storage (2025–2030)
Enterprise procurement professionals are shifting away from traditional transactional buying towards holistic system integration. Current procurement trends demonstrate five critical movements:
- Seismic-Aware Dynamic Engineering: Warehouses located along active zones (such as Chile, Peru, Western North America, and New Zealand) require finite-element modeling (FEM) to configure base-plate anchoring, back-to-back bracing, and energy-dissipating beam connectors according to standards such as NCh 2369, NSR-10, and AS 4084.
- Direct Automation Readiness (AS/RS & Shuttle Systems): Pallet racking must now feature sub-millimeter manufacturing tolerances (under ±1.0mm) to allow smooth passage of robotic radio shuttles, automated guided vehicles (AGVs), and autonomous mobile robots (AMRs).
- Eco-Responsible High-Performance Finishes: Environmental scrutiny has pushed the industry toward heavy-metal-free, RoHS-compliant electrostatic polyester powder coating preceded by automated non-hazardous pickling and phosphating lines that guarantee 500+ hours of salt-spray resistance.
- Container Landed-Cost Optimization: With maritime freight fluctuations, tier-1 Chinese exporters provide modularized beam-column flat-packing algorithms that achieve over 95% volumetric utilization inside standard 40-foot High Cube (40HQ) ocean containers.
Roll-Forming Accuracy
Automated multi-stage continuous roll-forming lines guarantee consistent cross-sectional thickness, uniform column pitch, and zero micro-cracking in high-tensile steel.
Automated 10-Step QC
From raw coil spectroscopic analysis to laser punch verification, dual-sided robotic welding, and automated powder coating thickness checks (60-80 microns).
Free 3D & CAD Engineering
Our 300+ engineering and technical team provides complete custom layout designs, pallet load matrices, seismic simulations, and detailed assembly blue-prints within 24 hours.
Comprehensive Enterprise Manufacturing Advantages
Why partner directly with an established Chinese original equipment manufacturer? Because intralogistics efficiency depends on manufacturing capability and engineering integrity:
- Direct Control of Raw Materials: Strategic long-term purchasing partnerships with leading tier-1 steel mills ensure verified mill test certificates (MTC) specifying yield strength, chemical composition, and elongation parameters for every production batch.
- Custom Surface Treatments for Harsh Environments: We configure multi-stage phosphating, heavy-duty powder coatings, and hot-dip galvanizing for harsh cold-storage environments (-30°C) and high-humidity coastal facilities.
- Comprehensive OEM & ODM Capabilities: Full branding, customized component stamping, custom beam hook profiles, and specialized packaging for regional racking brands, distributors, and EPC warehouse contractors worldwide.
- Global Logistics & Installation Guidance: Over 10,000 successful projects delivered across 120 countries, supported by multilingual engineering guidance (English, Spanish, Portuguese), numbered components, and comprehensive 3D installation videos.
Frequently Asked Questions on Pallet Racking Procurement
Clear, direct answers for warehouse managers, structural engineers, and logistics directors sourcing factory-direct industrial racking systems.
How do you verify the load-bearing safety of your pallet racking systems?
Can the racking be custom-engineered for specific regional seismic zones?
What parameters are required to generate a complimentary 3D CAD warehouse layout?
What surface treatment prevents corrosion in cold chain or coastal environments?
What is the typical production timeline and ocean transit lead time?
Transform Your Warehouse Storage Capacity Today
Send our structural engineering department your floor plan and pallet specifications. Receive a free 3D simulation, CAD drawing, and accurate factory-direct quotation within 24 hours.
Contact Us